Alumina crystals are widely utilized across various industrial sectors, and the efficient transportation of these materials is essential for maintaining production efficiency and preserving product quality. This article provides an overview of the alumina crystal conveying system, with a focus on the benefits and characteristics of pneumatic conveying technology. The system is engineered to handle the unique properties of alumina crystals, ensuring safe, reliable, and efficient material transport from storage to processing units.
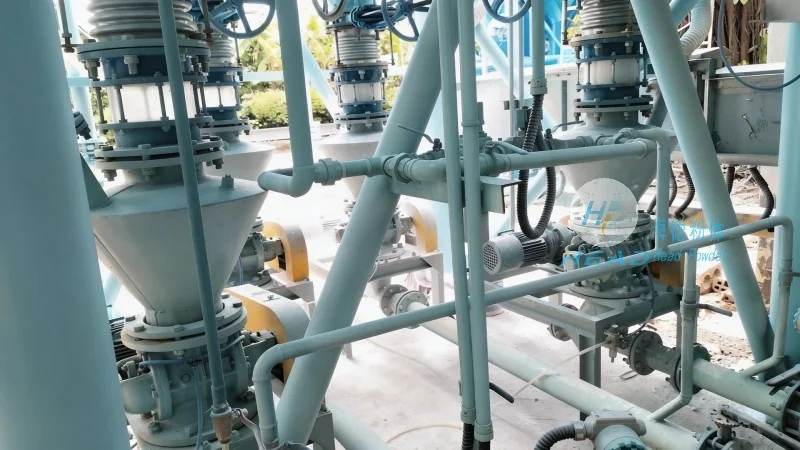
The alumina crystal conveying system is a specialized solution developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a prominent manufacturer based in Shandong, China. This system integrates advanced pneumatic conveying technology to address the challenges associated with handling alumina crystals, which are typically abrasive, lightweight, and prone to dust generation. The system is designed to meet the specific requirements of alumina production facilities, offering a flexible and scalable approach to material handling.
The alumina crystal conveying system comprises several critical components that work in unison to ensure optimal performance. These include a material hopper for storage and feeding, a pneumatic conveyor line with appropriately sized ductwork, a dust collection system to control airborne particles, and a discharge unit for delivering the crystals to processing equipment. Each component is carefully selected and configured to accommodate the unique characteristics of alumina crystals, such as their particle size distribution, density, and flowability. The system is engineered to minimize material degradation and maintain the purity of the crystals throughout the conveying process.
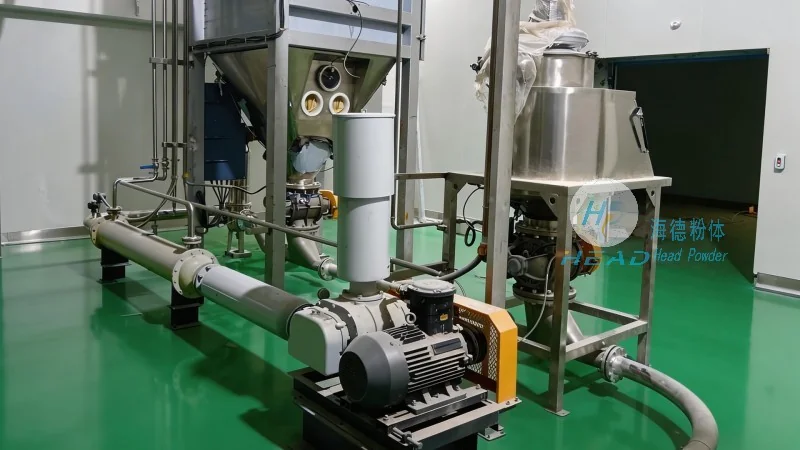
Pneumatic conveying offers several distinct advantages over traditional mechanical conveying methods for alumina crystals. One primary benefit is the ability to transport materials over extended distances without the need for multiple transfer points or intermediate storage. This reduces the risk of product contamination and degradation, which is crucial for high-value applications like ceramics and electronics where crystal purity is paramount. Additionally, pneumatic systems are more energy-efficient compared to mechanical systems, as they utilize compressed air to move materials, resulting in lower operational costs and reduced environmental impact.
Another key advantage is the minimized risk of product damage. Alumina crystals are delicate and can be easily broken or deformed during handling. Pneumatic conveying reduces mechanical stress by using air pressure to move materials, thereby preserving the integrity of the crystals. This is particularly important for applications where the crystal shape and size directly affect performance, ensuring consistent quality in downstream processes.
The alumina crystal conveying system incorporates robust safety features and environmental controls to comply with industrial standards. The integrated dust collection system effectively captures and filters airborne particles, preventing dust emissions and maintaining a clean working environment. This is essential for protecting both personnel and equipment from the harmful effects of alumina dust. Furthermore, the system is equipped with safety valves and pressure relief mechanisms to prevent over-pressurization and ensure safe operation under various conditions, providing peace of mind for facility operators.
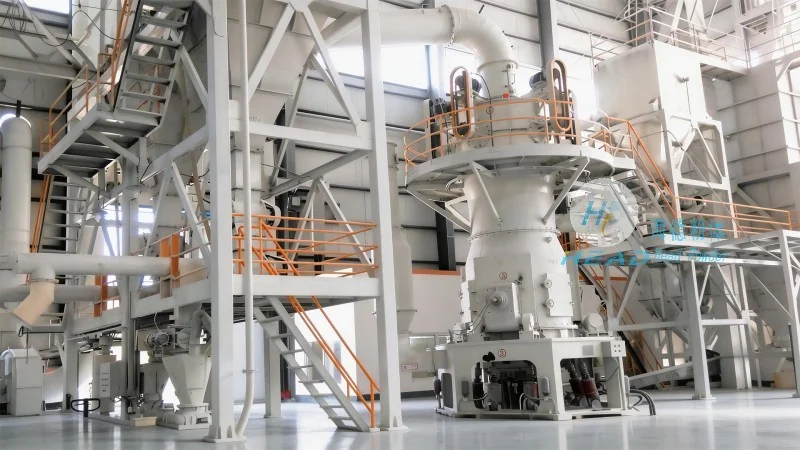
Shandong HeadPowder Engineering Co., Ltd. recognizes that each alumina production facility has unique operational requirements. Therefore, the conveying system is highly customizable to meet specific needs. Whether the facility requires a small-scale system for laboratory use or a large-scale system for industrial production, the company can design and implement a solution tailored to exact specifications. The system is also scalable, allowing for easy expansion as production volumes increase. This flexibility ensures that the system remains effective and efficient throughout the lifecycle of the alumina production process, adapting to evolving business needs.
In summary, the alumina crystal conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a cutting-edge solution for the efficient and safe transportation of alumina crystals. By leveraging pneumatic conveying technology, the system delivers numerous benefits, including long-distance transport, reduced product damage, enhanced safety, and environmental control. With its customizable and scalable design, the system is well-suited for a wide range of alumina production applications. As a leading manufacturer based in Shandong, China, headpowder continues to innovate and provide high-quality solutions that meet the evolving demands of the alumina industry, ensuring reliable material handling and consistent product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top