Efficient and reliable dust material conveying lines are essential in various industrial applications, particularly in sectors dealing with bulk materials like powders, granules, and fine particles. These systems are designed to transport these materials from one location to another with minimal loss, ensuring consistent performance and safety. Understanding the working principle and key features of such conveying lines is crucial for optimizing industrial processes and enhancing operational efficiency.
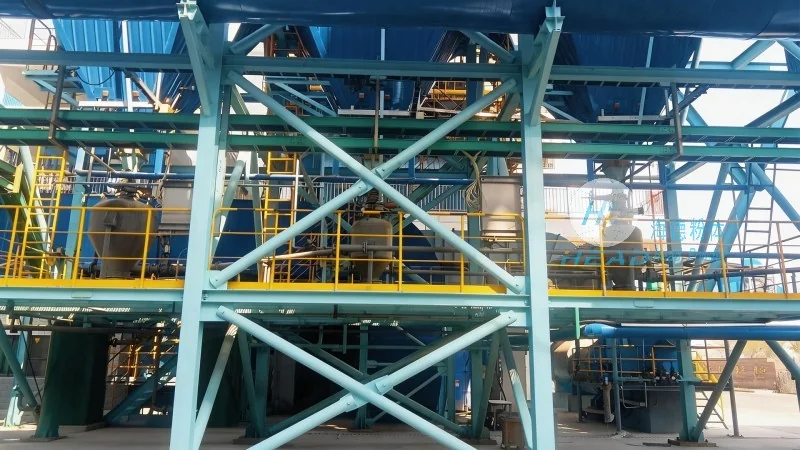
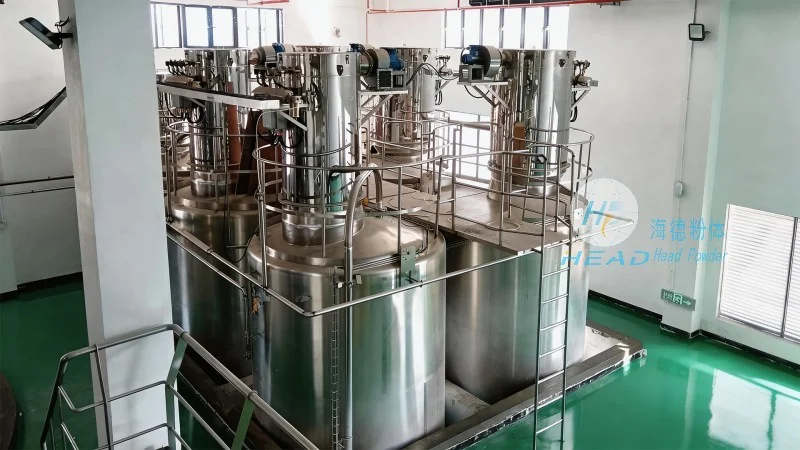
The core working principle of dust material conveying lines revolves around the use of mechanical or pneumatic systems to move particulate materials. Mechanical systems typically employ components like belts, screws, or buckets, while pneumatic systems utilize air pressure to transport materials through pipelines. In mechanical systems, the material is often conveyed through a continuous or intermittent motion, such as in belt conveyors where a moving belt carries the material from the inlet to the outlet. Screw conveyors, on the other hand, use a rotating screw to push the material forward, making them suitable for horizontal or slight incline applications. Bucket elevators, another common type, lift materials vertically using buckets attached to a chain or belt, which then discharge the material at the top. Pneumatic conveying systems, including positive displacement and negative pressure (or suction) methods, rely on compressed air to draw or push the material through a pipeline. Positive displacement systems use a pump to force air and material through the line, while suction systems create a vacuum to pull the material from the source to the destination. The choice of system depends on factors like material characteristics, distance, and environmental conditions. For instance, abrasive or corrosive materials may require special materials of construction for the conveying components, such as stainless steel or high-density polymers, to ensure durability and prevent wear. Additionally, the design of the system must consider the particle size, density, and flowability of the material, as these properties influence the selection of the conveying method and equipment. Proper sealing and maintenance are also critical to prevent material leakage and ensure the system operates efficiently over time. The working principle also involves controlling the flow rate and pressure to maintain consistent material transfer, which is vital for downstream processes like storage, processing, or packaging. By understanding these fundamental principles, industries can select the most appropriate dust material conveying line to meet their specific operational needs.
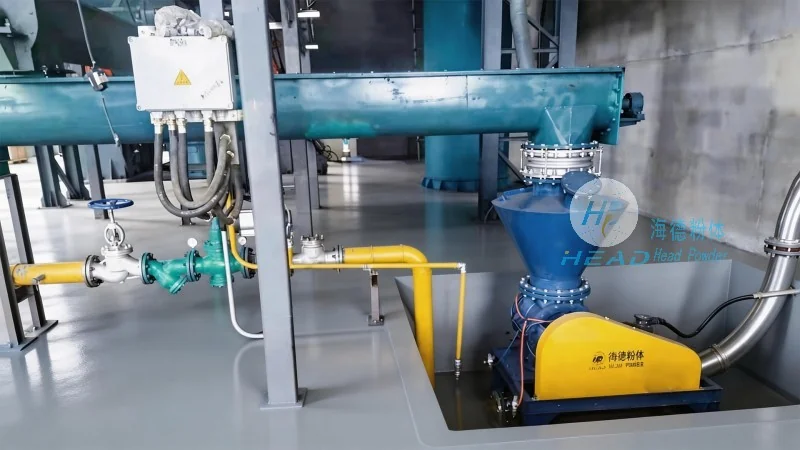
Dust material conveying systems offer several key features that make them indispensable in industrial settings. One of the primary features is their ability to handle a wide range of materials, from fine powders to bulk granules, with minimal degradation or segregation. This versatility allows them to be used in diverse industries, including pharmaceuticals, food processing, chemicals, and mining. Another important feature is their high efficiency in material transport, often achieving long distances with minimal energy consumption compared to other methods like manual handling or truck transport. The systems are also designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. Safety is a critical feature, as many dust material conveying lines are equipped with explosion-proof designs and dust collection systems to prevent dust explosions and ensure worker safety. The systems also provide consistent and reliable material flow, which is essential for maintaining production continuity and meeting quality standards. Furthermore, modern dust material conveying systems are often equipped with advanced control systems, such as variable frequency drives (VFDs) and sensors, that allow for real-time monitoring and adjustment of the conveying process. This enables operators to optimize the system performance based on changing material conditions or production demands. The features also include adaptability to different operating environments, from indoor facilities to outdoor applications, with weather-resistant components for outdoor use. The systems are designed to be scalable, allowing for expansion or integration with other industrial equipment as the business grows. Overall, the key features of dust material conveying systems contribute to improved operational efficiency, reduced costs, and enhanced safety in material handling processes.
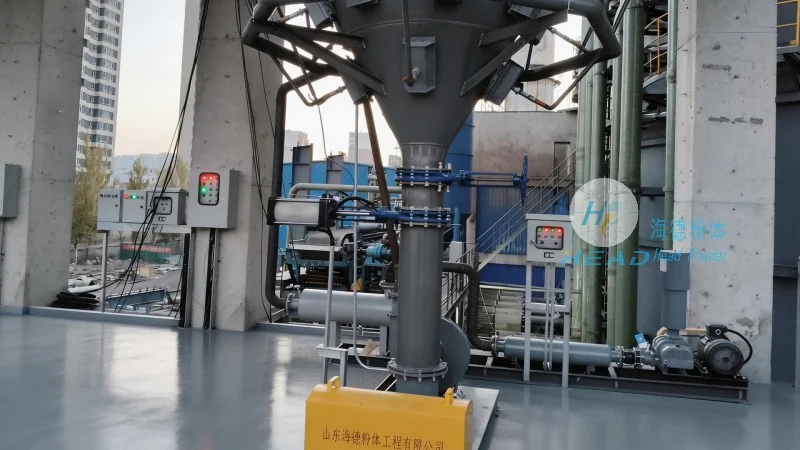
HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of dust material conveying systems, with a strong presence in the industrial equipment market. The company is headquartered in Shandong, China, and specializes in designing, manufacturing, and installing high-quality conveying solutions tailored to the needs of various industries. With years of experience in the field, HeadPowder has developed a reputation for delivering reliable and efficient dust material conveying lines that meet international standards. The company's products are engineered to handle a wide range of materials, including powders, granules, and fine particles, and are designed to operate in harsh industrial environments. HeadPowder's commitment to quality is evident in its use of advanced manufacturing techniques and rigorous quality control processes. The company's team of engineers and technicians work closely with clients to understand their specific requirements and provide customized solutions that enhance their operational efficiency. HeadPowder's dust material conveying systems are known for their durability, low maintenance, and high performance, making them a preferred choice for industries seeking reliable material handling solutions. The company's facilities are equipped with state-of-the-art technology and equipment, ensuring that every product meets the highest standards of quality and safety. HeadPowder's dedication to customer satisfaction and innovation has helped it establish a strong reputation in the market, with clients relying on its products for their critical material handling needs. Whether for new installations or upgrades, HeadPowder provides comprehensive support, including design, installation, and after-sales service, to ensure that clients get the most out of their dust material conveying systems. The company's focus on sustainability and environmental responsibility is also reflected in its products, which are designed to minimize energy consumption and reduce waste. Overall, Shandong HeadPowder Engineering Co., Ltd. is a trusted partner for industries looking to improve their material handling processes with efficient and reliable dust material conveying lines.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top