Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in dilute phase powder conveying systems. Based in Shandong, China, our company, known by the abbreviation "headpowder," provides innovative solutions for efficient and reliable powder handling in various industrial applications. This article explores the working principle and key features of our dilute phase powder conveying equipment, highlighting its advantages in modern material transport.
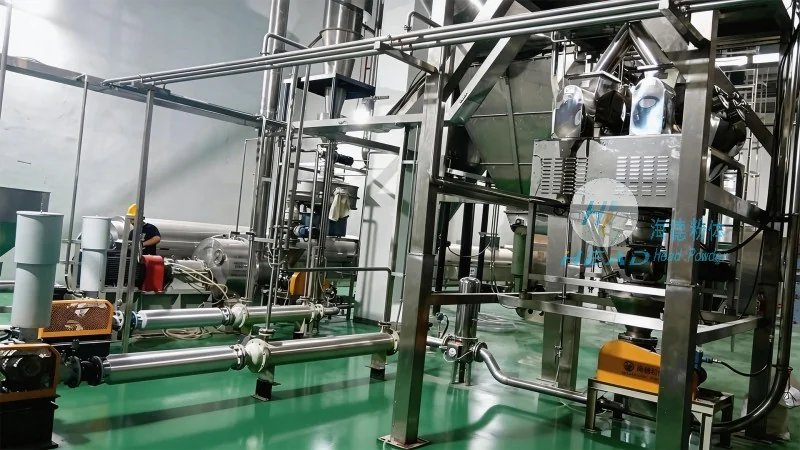
Dilute phase powder conveying systems are designed to transport dry powders and granular materials through a pipeline using a carrier gas, typically air or other inert gases. Unlike dense phase systems that rely on high pressure and low velocity, dilute phase systems operate at lower pressures and higher velocities, ensuring a more efficient and cost-effective material transport. The core components of these systems include a feeder, a pipeline, a compressor (or blower), and a control system. The feeder feeds the powder into the pipeline, while the compressor provides the necessary airflow to move the material through the system. The control system monitors and adjusts the flow rate and pressure to maintain optimal performance.
At the heart of a dilute phase powder conveying system is the principle of pneumatic transport. The process begins with the powder being fed into the inlet of the pipeline. The feeder, often a rotary valve or a star feeder, ensures a consistent flow of material. Simultaneously, the compressor generates a high-velocity airflow that carries the powder particles through the pipeline. As the powder travels, it is suspended in the gas stream, creating a dilute mixture. The velocity of the gas is critical; it must be sufficient to keep the powder particles airborne and prevent settling or blockages. The system typically includes a filter or separator at the outlet to remove the powder from the gas stream, allowing the clean air to be discharged or recycled. This continuous cycle ensures the efficient and reliable transport of powders over long distances and varying elevations.
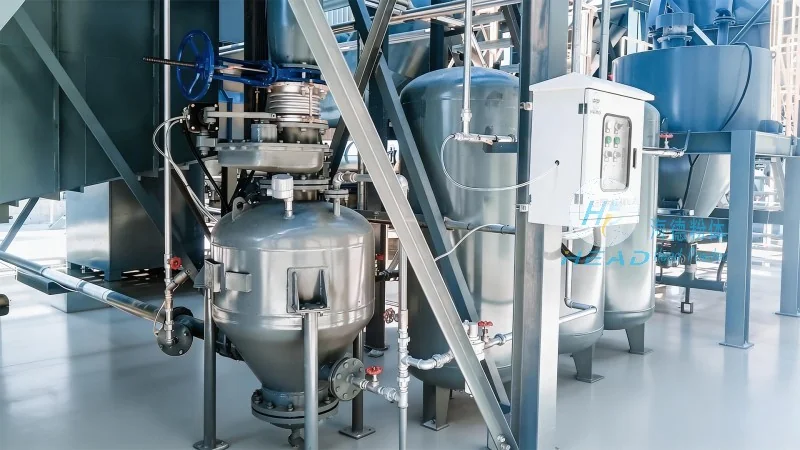
Our dilute phase powder conveying systems are engineered with several key features that enhance performance and reliability. First, the system operates at lower pressures compared to dense phase systems, reducing energy consumption and operational costs. This makes it suitable for applications where energy efficiency is a priority. Second, the high-velocity airflow ensures that the powder is fully suspended, minimizing the risk of blockages and ensuring smooth operation. The use of a feeder with precise control allows for consistent material feed rates, which is crucial for maintaining stable system performance. Additionally, the system is designed for easy maintenance and cleaning, with components that can be easily accessed and serviced. The control system provides real-time monitoring of pressure, flow rate, and temperature, enabling operators to quickly identify and address any issues. This proactive approach to maintenance helps to minimize downtime and maximize system uptime. Finally, the system is highly adaptable, capable of handling a wide range of powder types and particle sizes, from fine powders to coarse granules. This versatility makes it suitable for various industries, including chemical, pharmaceutical, food, and mining.
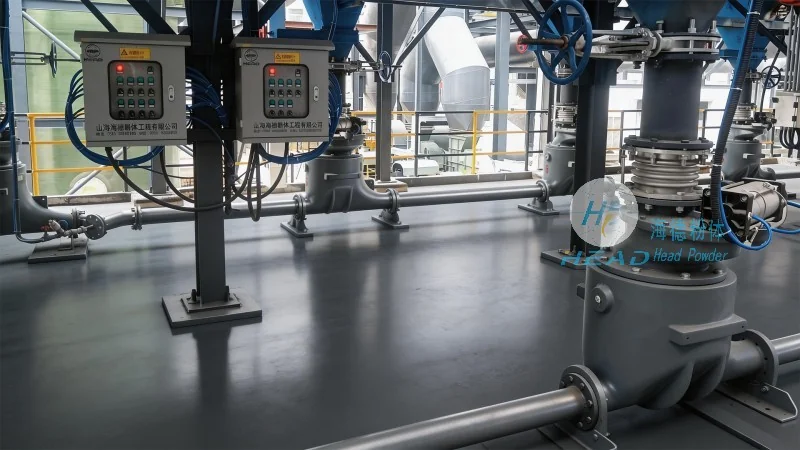
Implementing a dilute phase powder conveying system offers several significant advantages for industrial operations. The primary benefit is the reduction in energy consumption and operational costs. By operating at lower pressures, the system requires less power to move the material, leading to lower electricity bills and reduced carbon footprint. This is particularly important for companies looking to improve their sustainability and meet environmental regulations. Another advantage is the increased efficiency in material transport. The high-velocity airflow ensures that the powder is transported quickly and reliably, reducing the time and labor required for material handling. This can lead to improved production throughput and increased productivity. The system also offers flexibility in terms of distance and elevation changes. It can transport powders over long distances and through varying elevations without the need for additional equipment, such as pumps or conveyors. This makes it ideal for applications where the material needs to be moved from one location to another, such as in manufacturing plants or processing facilities. Furthermore, the system is relatively simple to install and operate, with minimal training required for operators. The compact design of the equipment also saves space in industrial facilities, making it suitable for applications where space is limited. Finally, the system is highly reliable, with a low risk of blockages or malfunctions. The use of a filter or separator at the outlet ensures that the powder is efficiently removed from the gas stream, preventing clogging and ensuring smooth operation. This reliability reduces the need for frequent maintenance and repairs, leading to lower overall costs.
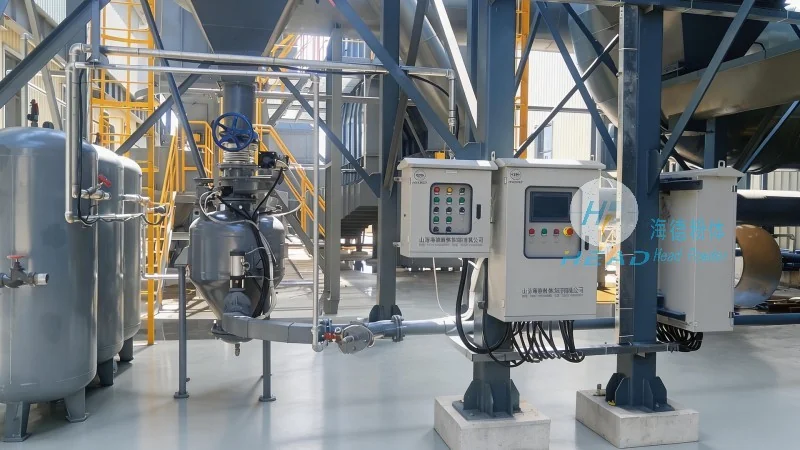
Dilute phase powder conveying systems are widely used in various industries due to their versatility and efficiency. In the chemical industry, these systems are used to transport raw materials and finished products, such as powders and granules. They are particularly useful in applications where the materials are sensitive to moisture or temperature, as the system can be designed to maintain specific conditions. In the pharmaceutical industry, the systems are used to transport active pharmaceutical ingredients (APIs) and other powders, ensuring that the materials are handled in a clean and controlled environment. The food industry also benefits from these systems, as they can transport food powders and ingredients without contamination. The mining industry uses dilute phase systems to transport ore and other materials from mines to processing facilities. The systems are also used in the agricultural industry to transport fertilizers and other agricultural products. In addition, they are used in the construction industry to transport cement and other building materials. The versatility of these systems makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial plants.
Shandong HeadPowder Engineering Co., Ltd. provides high-quality dilute phase powder conveying systems that are designed to meet the needs of various industrial applications. Our systems are engineered with the latest technology and features, ensuring efficient and reliable material transport. The working principle of these systems, based on pneumatic transport, allows for the safe and effective movement of powders over long distances and varying elevations. The key features of our systems, including low pressure operation, high-velocity airflow, and precise control, enhance performance and reduce operational costs. The advantages of using these systems, such as energy efficiency, increased productivity, and flexibility, make them an ideal choice for industrial operations. Whether you are in the chemical, pharmaceutical, food, mining, or construction industry, our dilute phase powder conveying systems can help you improve your material handling processes and achieve your business goals. Contact us today to learn more about our products and how we can help you.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top