Rice husk ash, a byproduct of rice processing, is widely utilized across various industrial sectors due to its distinctive properties. The efficient handling of this material is pivotal for optimizing production workflows and maintaining consistent quality standards. This article examines the concept of rice husk ash material handling and explores the core design principles that form the foundation of effective material handling systems.
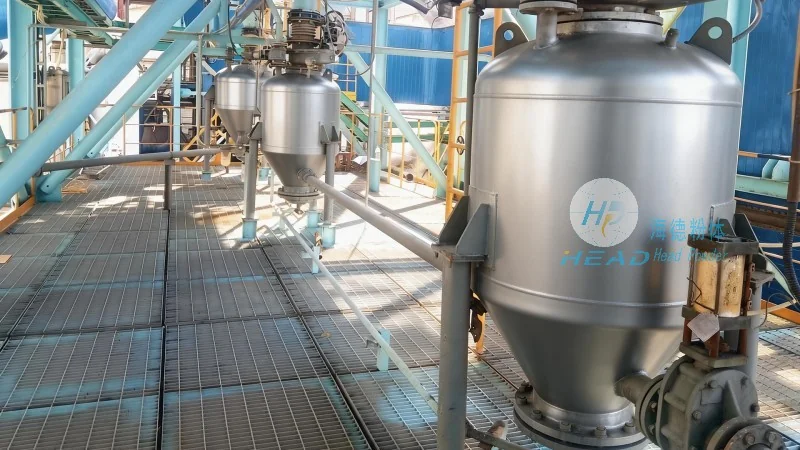
Rice husk ash material handling encompasses the processes and technologies involved in transporting, storing, and managing rice husk ash from its source to the point of application. This material, typically presented as fine powders or granules, demands specialized equipment and systems due to its lightweight, abrasive, and dusty characteristics. Proper material handling not only enhances operational efficiency but also minimizes environmental impact and ensures worker safety.
The design of rice husk ash material handling systems is guided by several critical principles that address the unique attributes of the material. These principles include:
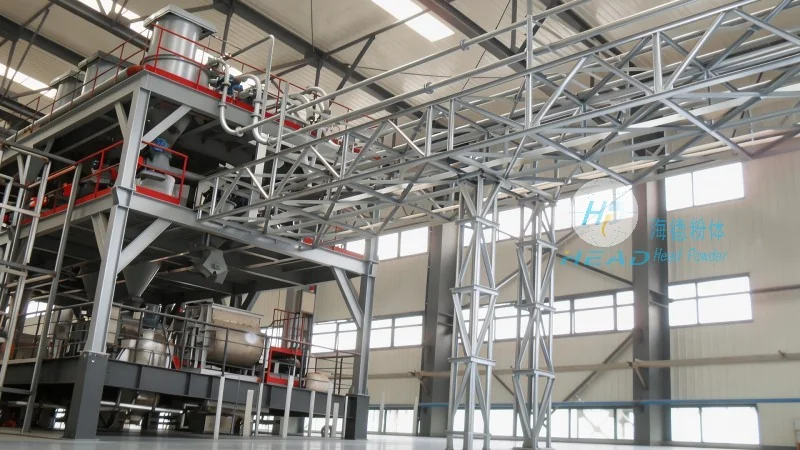
1. Material Compatibility: The equipment and components must be resistant to the abrasive and potentially corrosive nature of rice husk ash. This often requires selecting materials such as stainless steel, specialized alloys, or wear-resistant coatings to prevent degradation and ensure long-term durability.
2. Efficient Conveying Methods: Given the light weight and fine particle size of rice husk ash, conventional bulk handling methods may not be optimal. Systems may incorporate pneumatic conveying, screw conveyors, or bucket elevators, each chosen based on specific application requirements like distance, volume, and material flow characteristics.
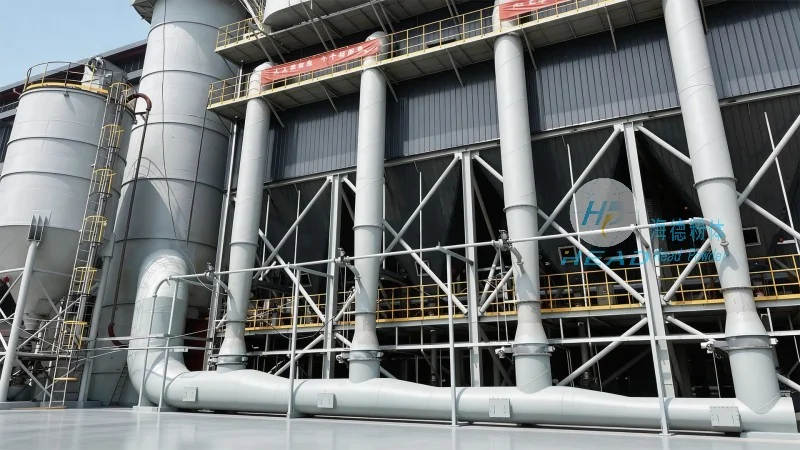
3. Controlled Dust Management: Rice husk ash is prone to generating dust, which can affect air quality and pose health risks. Effective design incorporates dust suppression systems, including enclosed conveyors, dust collection units, and proper ventilation, to maintain a safe working environment and comply with environmental regulations.
4. Space Optimization: In industrial settings, space is often limited. Design principles emphasize compact and modular systems that can be integrated into existing facilities without major modifications. This includes considerations for vertical space utilization, where vertical conveyors or multi-level storage solutions may be employed to maximize efficiency.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing systems tailored to the specific needs of rice husk ash processing. With extensive experience in the industry, the company understands the challenges associated with handling this material and offers customized solutions that adhere to the key design principles outlined above.
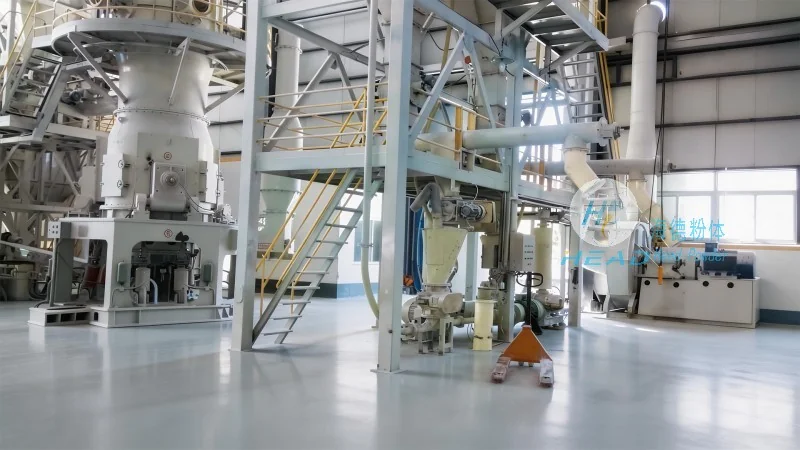
The company’s expertise lies in integrating advanced technologies and materials to create robust, efficient, and safe material handling systems. For example, their systems may incorporate high-efficiency screw conveyors with wear-resistant liners, pneumatic conveying networks equipped with dust collection capabilities, and automated control systems that optimize material flow and minimize downtime.
Efficient rice husk ash material handling is essential for maximizing the benefits of this valuable byproduct while ensuring operational efficiency and safety. By adhering to the fundamental design principles of material compatibility, efficient conveying, dust management, and space optimization, industries can develop systems that are both effective and sustainable. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing the expertise and solutions needed to implement these principles, helping clients achieve their production goals while maintaining high standards of safety and environmental responsibility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top