Understanding the process of copper concentrate powder material handling is crucial for industries involved in copper mining and processing. This article delves into the fundamental aspects of transporting and managing these fine powders, alongside the key design principles that ensure efficiency and safety in such operations.
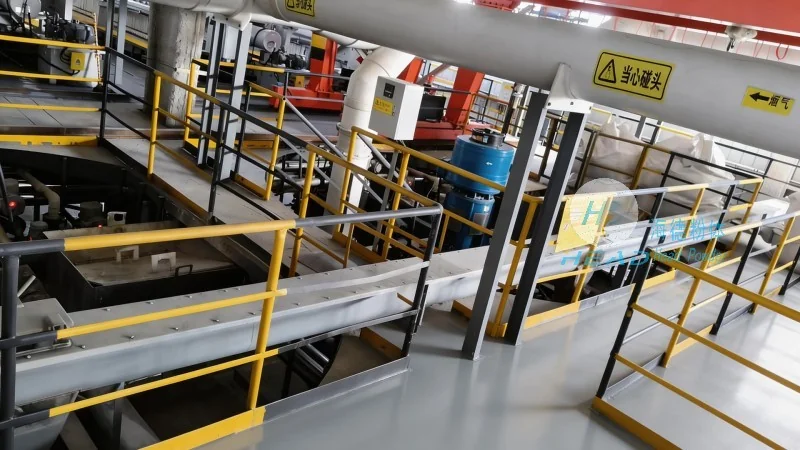
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of material handling solutions tailored to the unique challenges of copper concentrate powder processing. With a focus on innovation and reliability, the company provides comprehensive services to optimize material flow in copper mining operations.
Copper concentrate powder is a fine, granular material resulting from the beneficiation of copper ores. It typically contains high concentrations of copper sulfide minerals, along with other elements like iron, sulfur, and trace metals. The handling of this powder requires specialized equipment and systems due to its fine particle size, which can lead to issues such as dust generation, caking, and flowability challenges. Efficient material handling is essential to maintain product quality, minimize losses, and ensure safe operation in copper processing facilities.
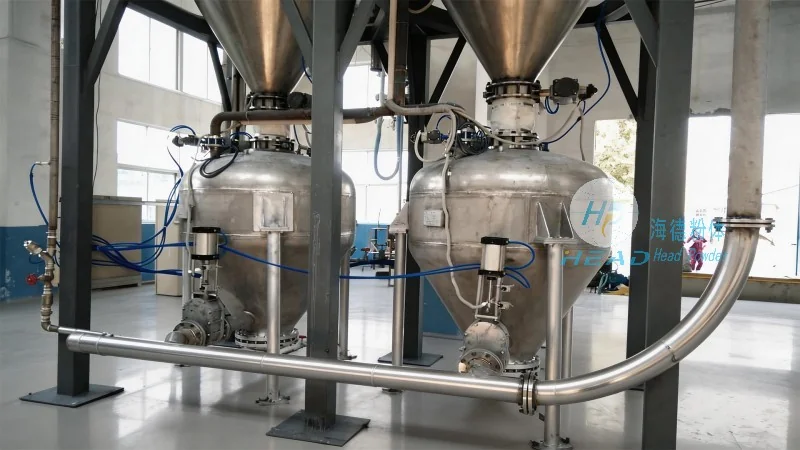
The design of copper concentrate powder handling systems is guided by several critical principles aimed at optimizing performance and safety. First, the principle of minimizing dust generation is paramount, as fine powders can pose health risks and environmental concerns. This is achieved through the use of enclosed systems, proper sealing, and dust collection equipment. Second, the principle of maintaining consistent flowability is crucial to prevent clogging and ensure smooth material transport. This involves selecting appropriate conveyor types, such as belt conveyors or pneumatic conveying systems, and incorporating features like vibration or air assistance to enhance flow. Third, the principle of energy efficiency is important to reduce operational costs. Designers often opt for systems with low power consumption, such as gravity-fed conveyors or energy-efficient motors, to minimize long-term expenses. Finally, the principle of safety and compliance is essential, as copper concentrate powders may contain hazardous components or require adherence to environmental regulations. This includes implementing proper ventilation, protective equipment, and adherence to industry standards.
Modern copper concentrate powder handling systems incorporate a range of components and technologies to meet these design principles. Conveyors are a primary component, with belt conveyors being widely used for horizontal and slight incline transport due to their reliability and ability to handle large volumes. For vertical or long-distance transport, pneumatic conveying systems are often employed, which use air pressure to move the powder through pipes. These systems can be either positive or negative pressure, depending on the application. In addition to conveyors, storage silos and hoppers are used to store the powder before transport, ensuring a steady supply. These structures are designed with smooth interiors and proper discharge mechanisms to prevent caking and blockages. Dust collection systems, such as baghouses or cartridge filters, are integrated to capture and remove airborne particles, protecting both personnel and the environment. Control systems, including sensors and automation, are also critical for monitoring flow rates, detecting blockages, and adjusting system parameters in real-time, enhancing overall system performance and safety.
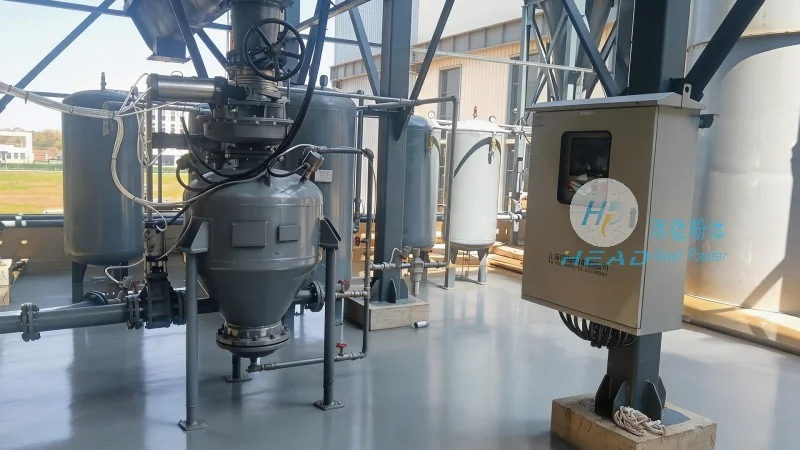
Real-world applications of copper concentrate powder handling systems vary based on the specific needs of mining operations. For example, in a large-scale copper mine, a combination of belt conveyors and pneumatic conveying systems may be used to transport the powder from the ore processing plant to a storage facility or to a smelter. The system would be designed to handle high volumes of material while minimizing dust and ensuring consistent flow. In smaller operations, a simpler system with a single belt conveyor and a storage silo might suffice. Practical considerations include the particle size distribution of the copper concentrate, as finer powders require more specialized handling equipment. The presence of moisture in the powder can also affect flowability, requiring additional measures such as drying or adding anti-caking agents. Additionally, the distance and elevation changes between the source and destination of the powder must be carefully considered when selecting the appropriate conveyor type and system configuration. Proper maintenance of the equipment is also essential to ensure long-term reliability and minimize downtime.
In conclusion, copper concentrate powder material handling is a complex process that requires careful consideration of design principles, components, and practical applications. By adhering to principles such as minimizing dust, maintaining flowability, and ensuring safety, industries can optimize their material handling systems to improve efficiency, reduce costs, and enhance product quality. HeadPowder Engineering Co., Ltd., with its expertise in material handling solutions, provides tailored designs and implementations to meet the unique needs of copper mining operations in China. With a commitment to innovation and reliability, the company continues to advance the technology and practices in copper concentrate powder handling, supporting the growth and sustainability of the copper industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top