Understanding the fundamentals of pneumatic conveying, particularly in the context of amino acids like glycine, is crucial for industries that handle fine powders. This article delves into the concept of glycine pneumatic conveying, explores the different types of pneumatic conveying systems, and highlights their practical applications in various industrial settings.
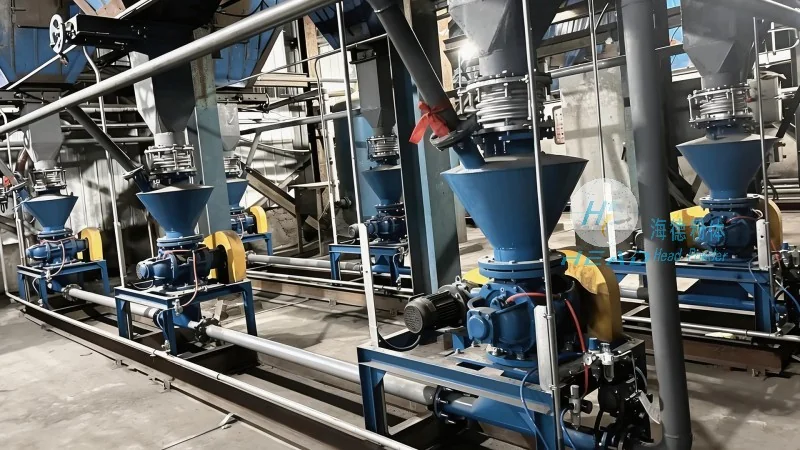
Glycine, a simple amino acid, is widely used in pharmaceuticals, food supplements, and chemical manufacturing. Pneumatic conveying is a method that uses air or other gases to transport bulk materials, including fine powders like glycine, from one location to another. This technique offers several advantages over traditional mechanical conveying, such as reduced equipment wear, lower risk of contamination, and the ability to handle materials in a closed system, which is essential for maintaining product purity and safety.
Pneumatic conveying systems are categorized based on the direction of airflow and the pressure used. The two primary types are pressure and vacuum systems.
Pressure systems operate by blowing air or gas into the conveying line, creating positive pressure that pushes the material forward. These systems are suitable for short to medium distances and can handle a wide range of materials, including abrasive or corrosive powders. They are commonly used in applications where the material needs to be transported from a central storage to multiple processing points.
Vacuum systems, on the other hand, use a vacuum to draw material into the conveying line. This method is ideal for long-distance transport or when the material needs to be collected from multiple sources. Vacuum systems are often preferred for handling delicate or sensitive materials, as they exert less force on the particles, reducing the risk of degradation or damage.
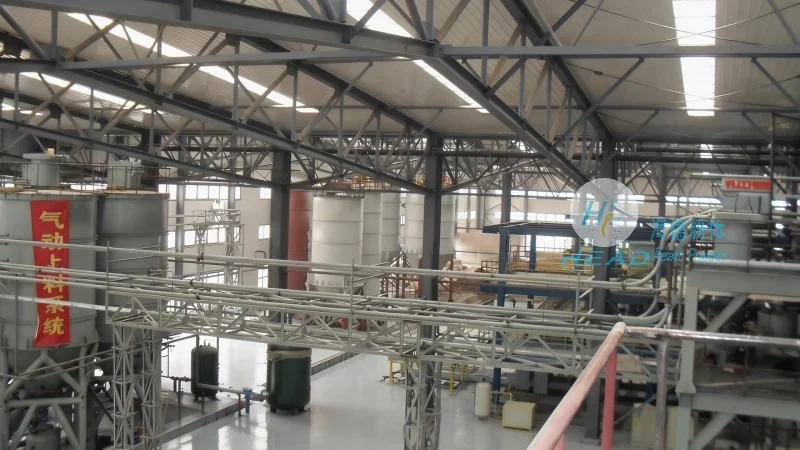
The versatility of pneumatic conveying makes it an ideal choice for processing glycine and other fine powders. Some key applications include:
1. Pharmaceutical Manufacturing: In the production of glycine-based drugs or supplements, pneumatic conveying ensures that the powder is transported without contamination, maintaining the high standards required for pharmaceuticals. The closed system prevents exposure to environmental factors, such as moisture or dust, which could compromise the product's quality.
2. Food and Beverage Industry: Glycine is used as a flavor enhancer and nutritional supplement in food products. Pneumatic conveying allows for efficient and hygienic transfer of the powder from storage to production lines, ensuring that the final product meets safety and quality regulations.
3. Chemical Processing: In chemical plants that produce or process glycine derivatives, pneumatic conveying systems are used to transport raw materials and finished products. The ability to handle corrosive or reactive materials safely makes this method indispensable in chemical manufacturing.
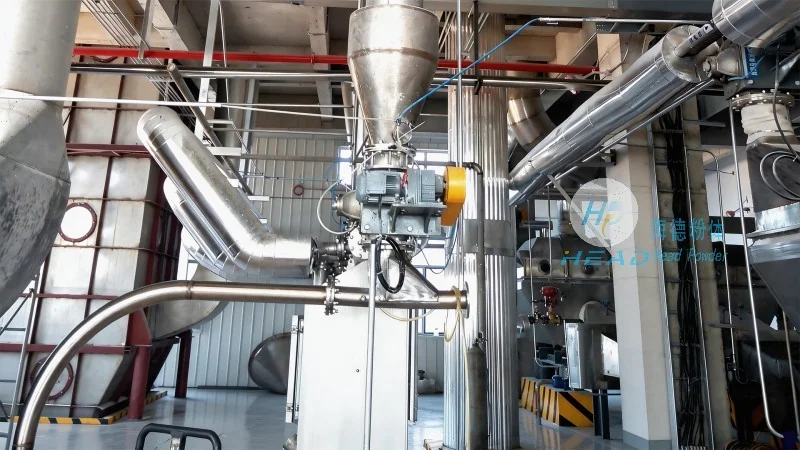
4. Research and Development: Laboratories working with glycine often require precise and controlled transport of small quantities of the powder. Pneumatic conveying systems can be scaled down to meet these needs, providing accurate and reliable material transfer for experimental purposes.
Implementing pneumatic conveying for glycine handling offers several benefits that enhance operational efficiency and product quality.
Firstly, hygiene and contamination control is a significant advantage. The closed system prevents the material from coming into contact with external contaminants, which is critical in industries like pharmaceuticals and food processing. This reduces the risk of product recalls and ensures compliance with regulatory standards.
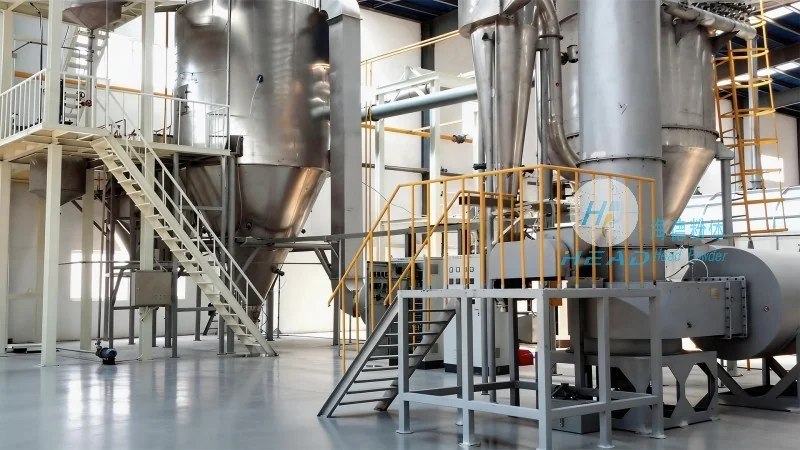
Secondly, energy efficiency is achieved through optimized system design. Modern pneumatic conveying systems use less energy compared to traditional methods, leading to lower operational costs and reduced environmental impact.
Thirdly, flexibility and scalability are key features. These systems can be easily adjusted to handle varying volumes of material, making them suitable for both small-scale research and large-scale industrial production. Additionally, they can be integrated with other processing equipment, such as mixers or reactors, to create a seamless production line.
Finally, reduced maintenance is another advantage. Unlike mechanical conveyors, which require regular maintenance to prevent wear and tear, pneumatic systems have fewer moving parts and are less prone to breakdowns. This results in lower maintenance costs and increased system reliability.
Glycine pneumatic conveying is a reliable and efficient method for transporting fine powders in various industrial applications. By understanding the different types of pneumatic conveying systems and their applications, industries can make informed decisions about the most suitable method for their specific needs. The benefits of this technology, including improved hygiene, energy efficiency, and flexibility, make it a preferred choice for handling glycine and other sensitive materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top