Asphalt powder, a critical component in road construction and pavement maintenance, requires efficient and reliable transportation methods to ensure quality and safety in construction projects. Pneumatic conveying systems have emerged as a preferred solution for handling asphalt powder due to their ability to transport materials in a dust-free environment, enhance operational efficiency, and reduce labor costs. This article provides an in-depth analysis of the classification of asphalt powder pneumatic conveying systems and their practical applications in various construction scenarios.
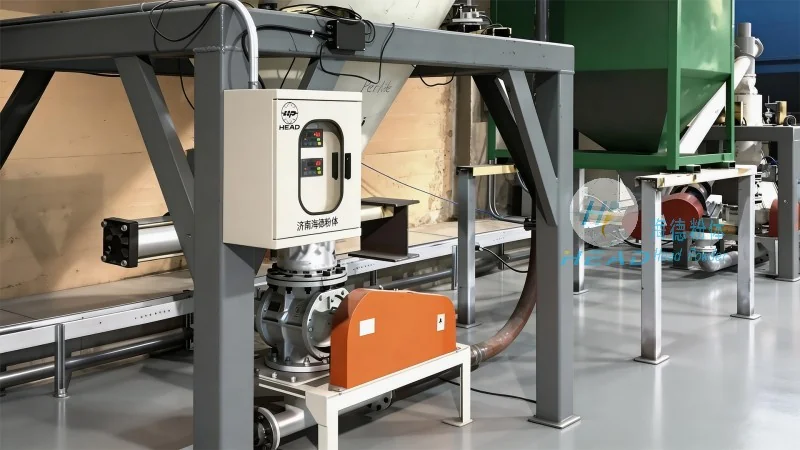
Asphalt powder pneumatic conveying systems can be categorized based on several key factors, including the conveying principle, pressure type, and application scope. The primary classifications include positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems utilize compressed air to push the material through the pipeline, offering high conveying capacity and suitability for long-distance and high-rise applications. Negative pressure systems, on the other hand, use vacuum to draw the material into the pipeline, which is ideal for short-distance and low-rise operations, especially in environments where dust control is paramount. Hybrid systems combine elements of both positive and negative pressure, providing flexibility in handling different material characteristics and operational requirements.
Understanding the core components and working principles of these systems is essential for optimizing performance and ensuring longevity. The main components of a pneumatic conveying system for asphalt powder typically include a material hopper, feeder, air compressor or vacuum pump, conveying pipeline, and a receiver or dust collector. The material hopper stores the asphalt powder, while the feeder regulates the flow rate to maintain consistent material supply. The air compressor generates the necessary pressure for positive pressure systems, whereas the vacuum pump creates the suction force for negative pressure systems. The conveying pipeline transports the material from the source to the destination, and the receiver collects the material at the end of the system, often equipped with dust filtration to minimize environmental impact.
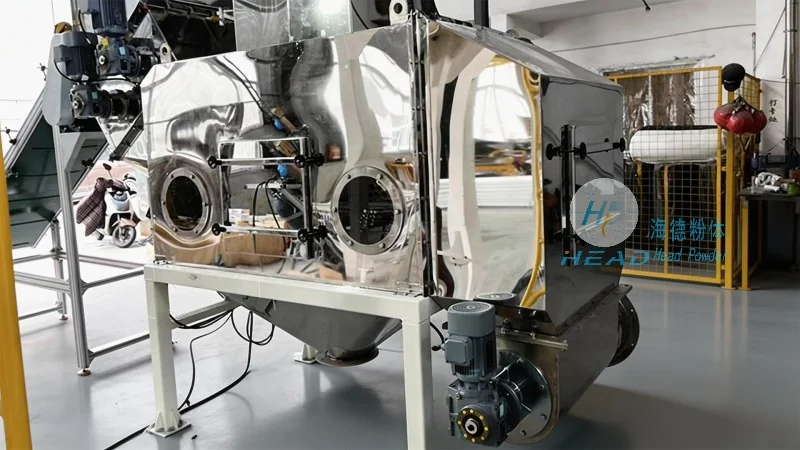
The application of asphalt powder pneumatic conveying systems varies across different construction projects, each with specific requirements for material handling. In large-scale road construction projects, these systems are commonly used to transport asphalt powder from storage silos to mixing plants, ensuring a continuous and uninterrupted supply of raw materials. This is particularly beneficial in high-volume production environments where traditional bucket elevators or belt conveyors may face limitations in terms of speed and efficiency. Additionally, in pavement maintenance and repair operations, pneumatic conveying systems enable precise and controlled delivery of asphalt powder to the work site, reducing the need for manual handling and minimizing material waste.
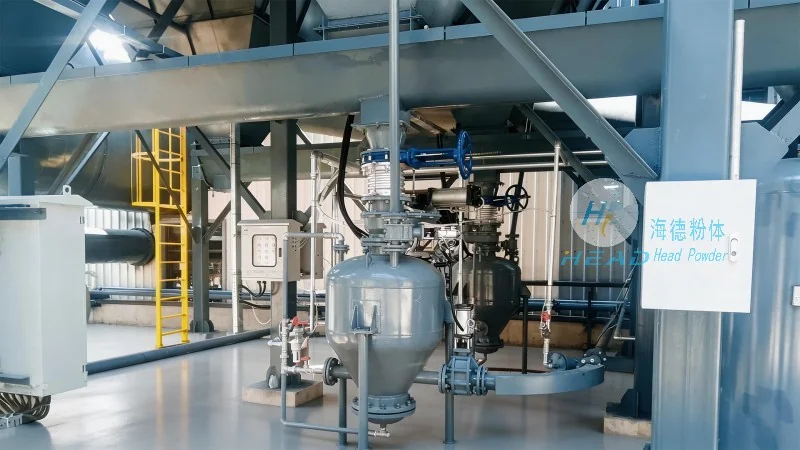
Implementing asphalt powder pneumatic conveying systems offers several advantages, including improved safety by eliminating manual handling of dusty materials, enhanced material quality through reduced exposure to air and moisture, and increased operational efficiency through automated control. However, challenges such as system maintenance, material compatibility, and energy consumption must be carefully considered. Regular maintenance of components like air compressors, pipelines, and filters is crucial to prevent downtime and ensure consistent performance. Material compatibility is also a key factor, as certain asphalt powders may have high moisture content or abrasive properties that can affect the lifespan of system components. Energy consumption is another consideration, as both positive and negative pressure systems require significant power, and optimizing energy usage through efficient design and operation is essential for cost-effectiveness.
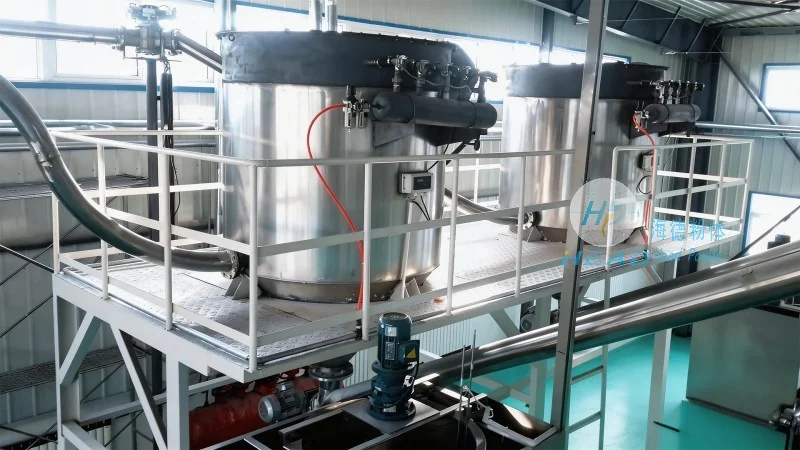
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, has successfully implemented asphalt powder pneumatic conveying systems in numerous construction projects across China. One notable case involved a major highway construction project in Shandong Province, where the company's positive pressure system efficiently transported asphalt powder from a storage silo to a mixing plant over a distance of 500 meters. The system's high conveying capacity and reliable performance ensured that the construction schedule was met without any material shortages or operational disruptions. Another application was in a pavement maintenance project for a large urban area, where a negative pressure system was used to transport asphalt powder to repair sites, minimizing dust emissions and improving worker safety. These successful implementations highlight the effectiveness of pneumatic conveying systems in enhancing construction efficiency and quality.
In conclusion, asphalt powder pneumatic conveying systems represent a sophisticated and efficient solution for handling asphalt powder in construction applications. The classification of these systems based on pressure type and conveying principle allows for tailored solutions to meet specific project requirements. By understanding the key components, working principles, and application scenarios, construction companies can optimize their material handling processes and improve overall project outcomes. As technology advances, future trends may include the integration of automation and smart monitoring systems to further enhance system performance and reduce operational costs. The continued development and adoption of pneumatic conveying systems will undoubtedly play a vital role in the future of road construction and maintenance, ensuring sustainable and efficient material handling practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top