For industries dealing with bulk powders, the small bag weighing and quantitative powder conveying system equipment plays a crucial role in ensuring accurate material handling and processing. This equipment is designed to efficiently handle the weighing, packaging, and transport of powders in small bag formats, providing precision and reliability in operations. Understanding the components and design principles behind such systems is essential for optimizing production processes and maintaining quality standards.
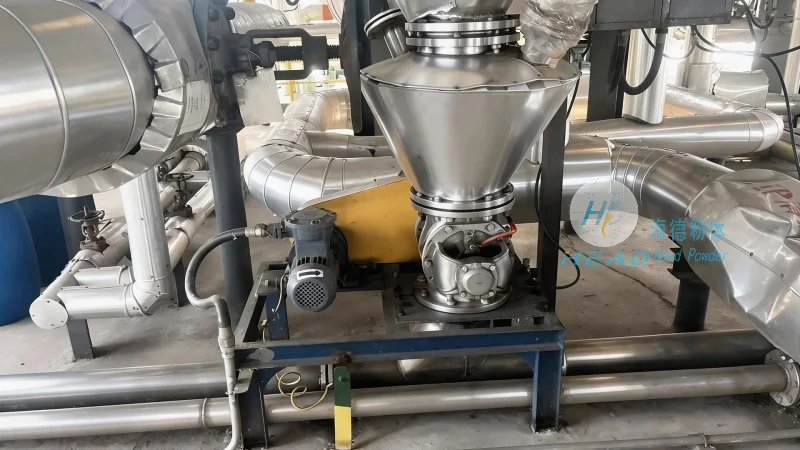
At the core of these systems is the ability to measure and dispense powders into small bags with high accuracy. The system typically integrates several key components, including a weighing scale, a conveyor mechanism, a bagging unit, and a control system. Each component works in tandem to ensure that the correct amount of powder is weighed and transferred into the bag, minimizing waste and maximizing efficiency. The design of these systems is tailored to handle various types of powders, from fine chemicals to food ingredients, making them versatile for different industrial applications.
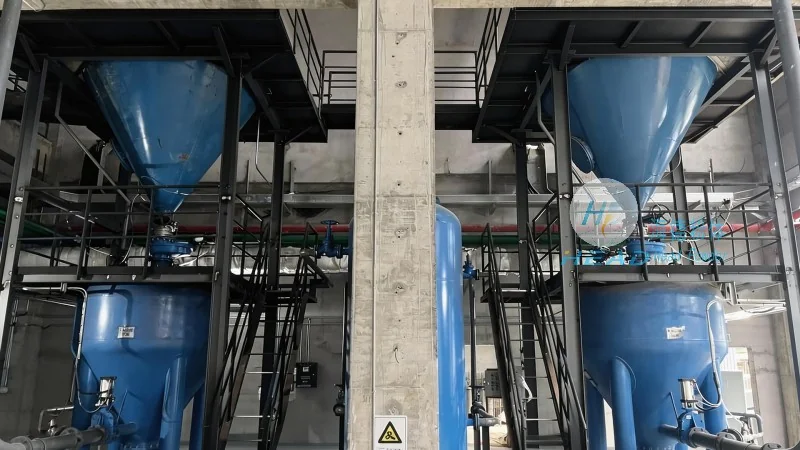
The design principles of small bag weighing and quantitative powder conveying systems focus on precision, reliability, and adaptability. Precision is achieved through advanced weighing technology, such as load cells and digital scales, which provide accurate measurements even for small quantities of powder. The control system, often equipped with programmable logic controllers (PLCs), allows for automated operation and real-time monitoring of the weighing process. This ensures that each bag is filled to the exact specified weight, reducing errors and improving product consistency. Reliability is enhanced by robust construction and regular maintenance protocols, ensuring that the system operates continuously without downtime. Adaptability is achieved through modular design, allowing for customization based on the specific requirements of the user, such as different bag sizes, powder types, or production volumes.
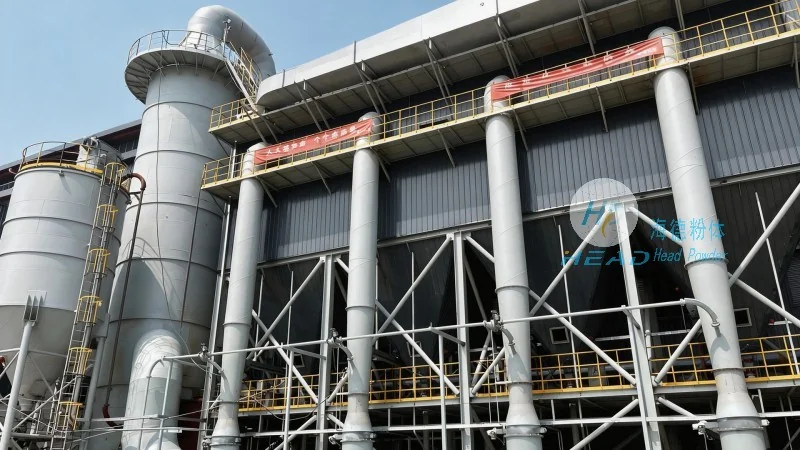
Several critical components contribute to the functionality of small bag weighing and quantitative powder conveying systems. The weighing scale is the primary component responsible for measuring the weight of the powder as it is being filled into the bag. High-precision load cells are used to detect even minor changes in weight, providing accurate data to the control system. The conveyor mechanism transports the powder from the storage hopper to the weighing scale and then to the bagging unit. This mechanism is designed to handle different powder flow rates and maintain a consistent flow, preventing clogging or uneven distribution. The bagging unit is responsible for forming and sealing the small bags, ensuring that the powder is contained securely. This unit may include features like bag openers, fill spouts, and sealing mechanisms, depending on the specific design. The control system, often integrated with a human-machine interface (HMI), allows operators to set parameters, monitor the process, and adjust settings as needed. This system provides real-time feedback on the weighing process, enabling quick corrections if any deviations occur.
Small bag weighing and quantitative powder conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemicals, and agriculture. In the pharmaceutical industry, these systems are essential for packaging active ingredients and excipients with high precision, ensuring compliance with regulatory standards. In food processing, they are used to package spices, flour, and other ingredients, maintaining quality and consistency. In the chemical industry, they handle raw materials and intermediates, reducing material waste and improving production efficiency. The benefits of these systems include improved accuracy in weighing, reduced labor costs through automation, increased production speed, and enhanced product quality. Additionally, the modular design allows for easy integration into existing production lines, minimizing the need for extensive modifications.
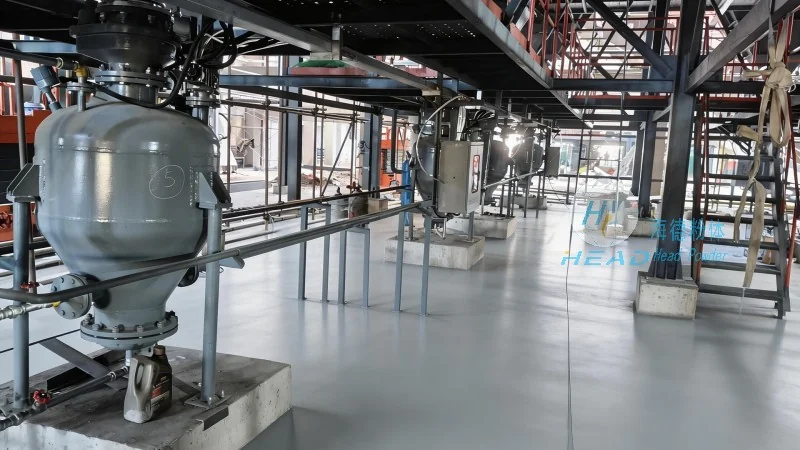
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of small bag weighing and quantitative powder conveying systems. With a focus on innovation and quality, the company has developed advanced solutions tailored to the needs of various industries. HeadPowder's systems are designed to meet the highest standards of precision and reliability, ensuring that customers can achieve optimal performance in their operations. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center. HeadPowder's commitment to customer satisfaction and technical excellence has made it a trusted partner for businesses worldwide seeking efficient and accurate powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top