HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems. Among their product line, the Red Bean Pneumatic Conveying Machine stands out for its efficiency and adaptability in various industrial applications. This article delves into the fundamental principles behind this equipment and explores the diverse working scenarios where it excels.
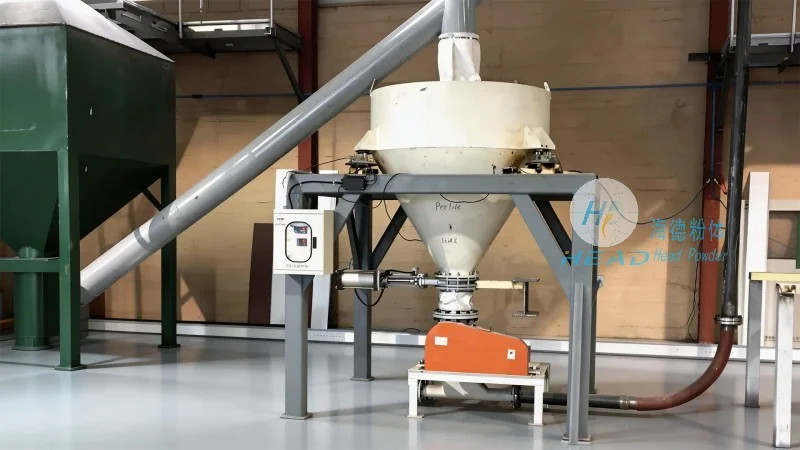
The Red Bean Pneumatic Conveying Machine operates on the principle of pneumatic transport, utilizing air as the medium to move bulk materials from one location to another. Unlike traditional mechanical conveyors, this system eliminates the need for physical contact between the material and the conveying components, reducing wear and tear and minimizing the risk of contamination. The machine typically consists of a hopper, a rotary valve, a pipeline system, and a dust collector, all working in tandem to ensure smooth and reliable material transfer. The hopper stores the material, while the rotary valve controls the flow rate. Compressed air is then introduced into the pipeline, creating a pressure differential that propels the material forward. The dust collector ensures that any airborne particles are captured, maintaining a clean and safe working environment. This integrated approach allows for precise control over the conveying process, making it suitable for a wide range of materials, including powders, granules, and even small solid particles.
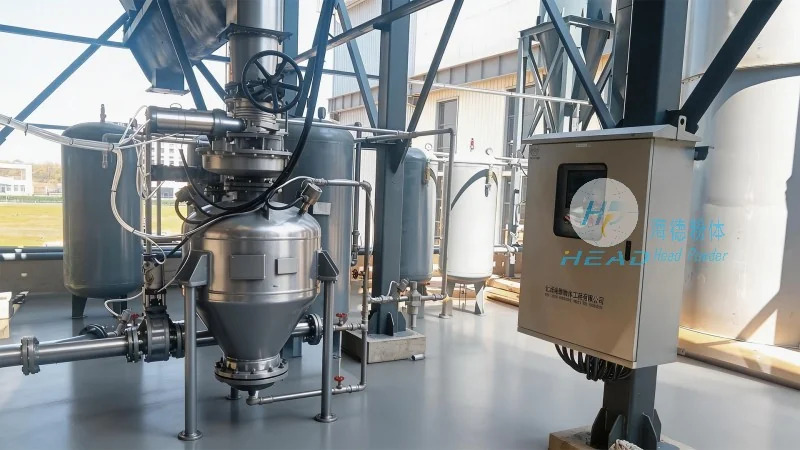
The Red Bean Pneumatic Conveying Machine is particularly well-suited for industries that require the handling of bulk materials in a controlled and efficient manner. One of the primary applications is in the food processing sector, where the machine is used to transport ingredients such as red beans, flour, and other dry goods. The system's ability to maintain a sterile environment, thanks to the dust collector and sealed pipelines, makes it ideal for food-grade applications. Additionally, it is widely used in the pharmaceutical industry, where the handling of powders requires stringent hygiene standards. The machine's design ensures that no cross-contamination occurs, preserving the purity of the products. In the chemical industry, it is employed to transport various powders and granules, including those that are abrasive or corrosive. The system's flexibility allows for adjustments in air pressure and flow rate to accommodate different material properties, ensuring optimal performance. Furthermore, the Red Bean Pneumatic Conveying Machine is utilized in the agricultural sector for the processing and distribution of seeds and grains. Its compact design and low maintenance requirements make it a cost-effective solution for small to medium-sized operations. The machine's adaptability also extends to the manufacturing of building materials, where it is used to convey cement, sand, and other aggregates. In each of these scenarios, the machine's efficiency and reliability contribute to increased productivity and reduced operational costs.
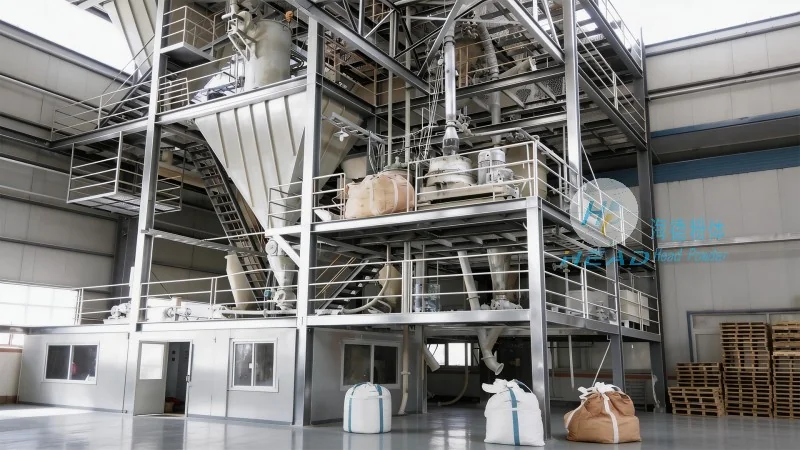
HeadPowder's Red Bean Pneumatic Conveying Machine offers several advantages that make it a preferred choice for industrial applications. One of the key benefits is its ability to handle a wide range of materials, from fine powders to larger granules, without the need for pre-processing. The system's design minimizes material degradation, ensuring that the product's quality is maintained throughout the conveying process. Another advantage is its low maintenance requirements, as the components are designed to withstand the rigors of continuous operation. The machine's energy efficiency is also notable, as it uses compressed air efficiently, reducing operational costs. Technical specifications of the Red Bean Pneumatic Conveying Machine typically include a conveying capacity ranging from 1 to 50 tons per hour, depending on the material and system configuration. The pipeline diameter can vary from 50 to 200 mm, allowing for customization based on the application. The system operates at pressures between 0.5 to 1.0 MPa, with adjustable air flow rates to control the material velocity. The hopper capacity is usually designed to accommodate 0.5 to 2 cubic meters of material, ensuring a steady supply. The dust collector is equipped with a filtration system that can handle high volumes of air, maintaining a clean working environment. These specifications make the machine versatile and adaptable to various industrial needs, from small-scale operations to large-scale production facilities.
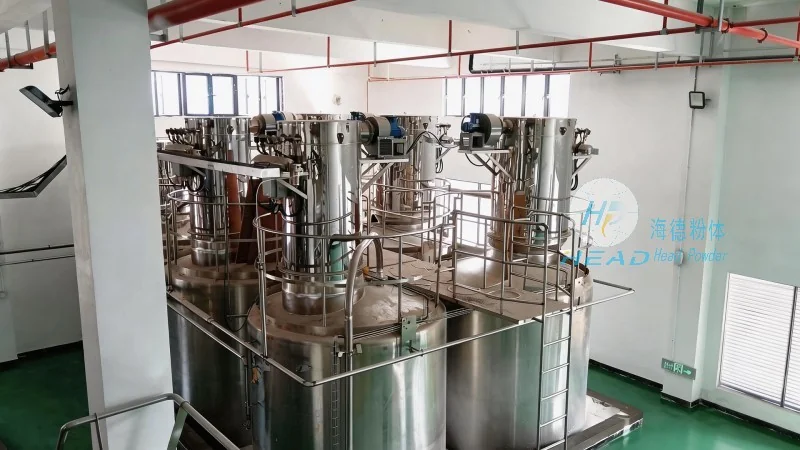
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable manufacturer specializing in the production of high-quality pneumatic conveying systems. The Red Bean Pneumatic Conveying Machine exemplifies the company's commitment to innovation and efficiency, offering a reliable solution for material handling in diverse industries. With its robust design, advanced features, and adaptability, this equipment has become a trusted choice for businesses seeking to optimize their material transport processes. HeadPowder's dedication to quality and customer satisfaction ensures that their products meet the highest standards, making them a leading provider in the industry. Whether used in food processing, pharmaceuticals, chemicals, or agriculture, the Red Bean Pneumatic Conveying Machine provides an efficient and cost-effective solution for bulk material handling, contributing to increased productivity and operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top