Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions. Based in Shandong, China, our company specializes in the design, manufacturing, and installation of advanced material conveying systems tailored for dust collection stations. This article provides a detailed overview of the operation process and working principles of our material conveying equipment, ensuring efficient and reliable material transport in industrial applications.
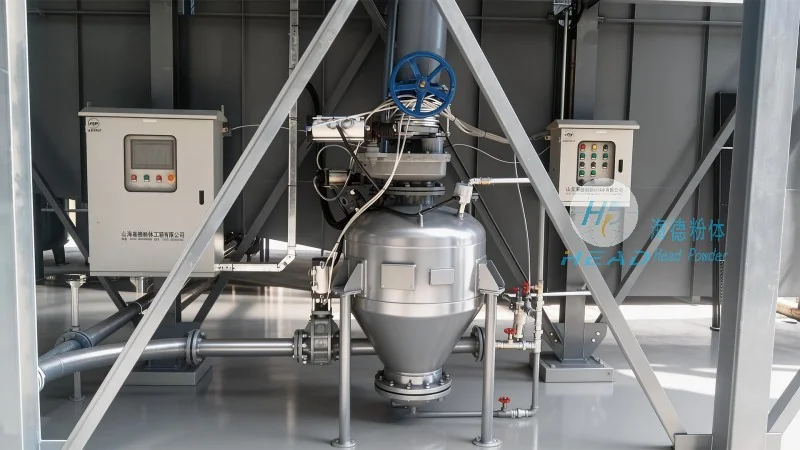
Shandong HeadPowder Engineering Co., Ltd. is dedicated to delivering high-quality engineering solutions for material handling in various industrial sectors. Our headquarters is located in Shandong, China, where we leverage local expertise and advanced manufacturing capabilities to produce robust and efficient material conveying equipment. We focus on providing customized solutions that meet the specific needs of our clients, ensuring optimal performance and durability in demanding operational environments.
Material conveying equipment for dust collection stations plays a critical role in the efficient operation of industrial dust control systems. These systems are designed to transport bulk materials, such as powders or granules, from the dust collection point to storage or processing areas. The equipment typically includes components like feed hoppers, conveyor belts, screw conveyors, or pneumatic transport systems, each tailored to handle different material characteristics and operational requirements.
The material conveying equipment for dust collection stations consists of several key components, each with a specific function to ensure smooth and reliable operation. The feed hopper is the initial component that collects the material from the dust collector. It is designed to handle varying material flow rates and prevent material buildup or blockages. The hopper is often equipped with a discharge valve or gate to control the flow of material into the conveyor system.
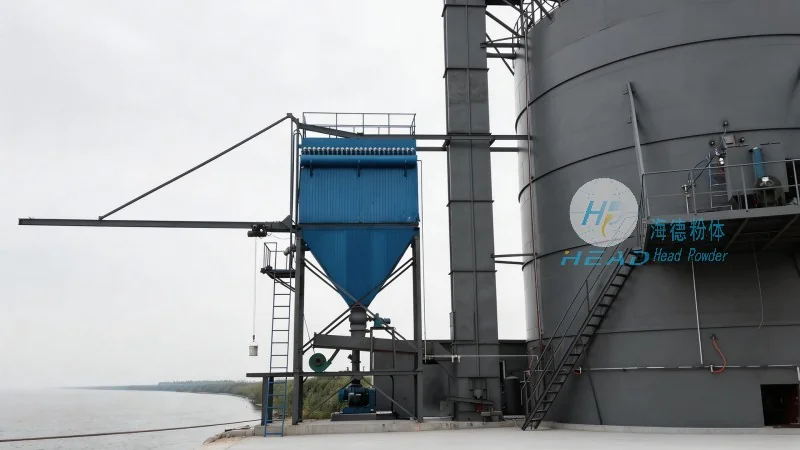
Next, the conveyor system itself, which can be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the material properties and application. A belt conveyor uses a continuous belt to transport material horizontally or at an incline, while a screw conveyor utilizes a rotating screw to push material forward. Pneumatic conveyors use air pressure to move material through a pipeline. Each type of conveyor has its advantages and is selected based on factors like material size, moisture content, and the required transport distance.
The operation process of the material conveying system for dust collection stations begins with the material being collected by the dust collector and deposited into the feed hopper. The material then flows from the hopper into the conveyor system under gravity or with the assistance of a feeder mechanism. The conveyor transports the material to the discharge point, where it is either stored in a silo or transferred to further processing equipment.
During operation, the system is monitored for proper functioning. Sensors and control systems ensure that the material flow rate is consistent and that there are no blockages or overloads. The control panel allows operators to adjust the speed of the conveyor or the feed rate from the hopper, optimizing the system's performance based on the current production needs. Regular maintenance is also crucial to ensure the longevity and efficiency of the equipment, including cleaning of the conveyor belt, lubrication of moving parts, and inspection of the hopper and discharge mechanisms.
The working principle of the material conveying equipment for dust collection stations is based on the physical properties of the material and the mechanical action of the conveyor components. For belt conveyors, the material is placed on the moving belt and carried forward by the belt's motion. The screw conveyor operates by rotating a screw within a casing, which pushes the material forward as it turns. Pneumatic conveyors use compressed air to create a flow of material through the pipeline, with the air pressure and velocity controlling the transport rate.
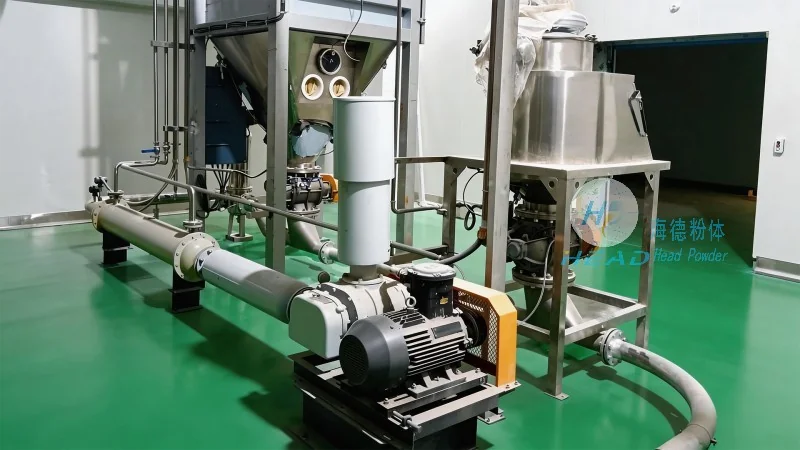
In all cases, the equipment is designed to minimize material degradation and loss. The conveyor components are made of materials resistant to the specific properties of the conveyed material, such as abrasion resistance or chemical compatibility. The system is also equipped with dust collection and filtration features to prevent dust emissions during the transport process, ensuring compliance with environmental regulations and maintaining a safe working environment.
Our material conveying equipment for dust collection stations offers numerous benefits, including improved operational efficiency, reduced labor costs, and enhanced safety. The equipment is designed to handle high volumes of material with minimal maintenance, making it suitable for continuous industrial operations. It is widely used in industries such as mining, cement, chemical processing, and food processing, where efficient material transport is critical to overall production efficiency.
The system's ability to handle various material types and transport them over long distances makes it a versatile solution for different industrial applications. By integrating with dust collection systems, the equipment ensures that material is transported without causing dust pollution, contributing to a cleaner and safer working environment. Our company's expertise in designing and manufacturing these systems ensures that clients receive tailored solutions that meet their specific operational requirements and regulatory standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top