Dilute phase powder conveying systems are industrial equipment designed to transport bulk solid materials, such as powders and granules, over long distances with high efficiency and minimal pressure drop. These systems are widely used in various industries, including chemical, pharmaceutical, food processing, and mining, due to their ability to handle large volumes of material while maintaining low energy consumption and operational reliability. The core of a dilute phase system lies in its design, which integrates several key components to achieve effective material transport. Understanding the design principles and operational mechanisms of these systems is crucial for optimizing performance and ensuring safe and efficient material handling in industrial applications.
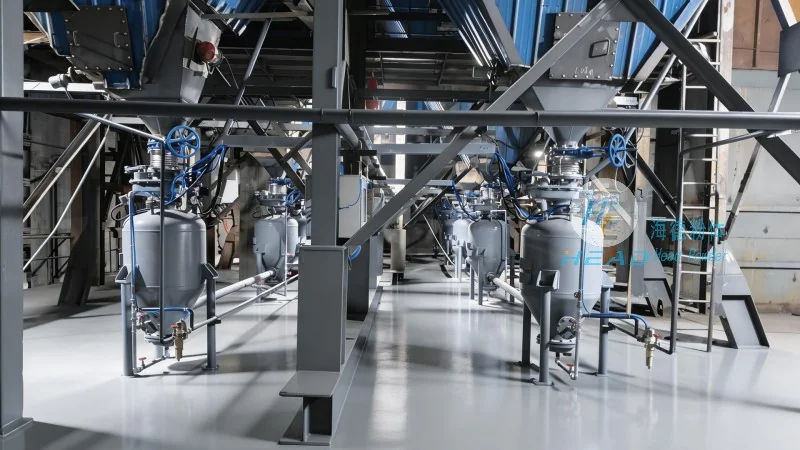
The headpowder system, as a representative of advanced dilute phase technology, typically consists of several essential components. The primary components include a blower or compressor to generate the necessary air flow, a hopper or feeder to feed the powder into the system, a pipeline network to transport the material, and a receiver or discharge unit to collect the material at the destination. Each component plays a critical role in the overall operation of the system. The blower provides the motive force by creating a high-velocity air stream that suspends the powder particles, allowing them to be carried through the pipeline. The feeder ensures a consistent and controlled feed rate of the powder, preventing blockages and maintaining system stability. The pipeline network, often made of materials like stainless steel or plastic, is designed to minimize friction and pressure loss, while the receiver efficiently collects the conveyed material, preventing dust emissions and ensuring product integrity.
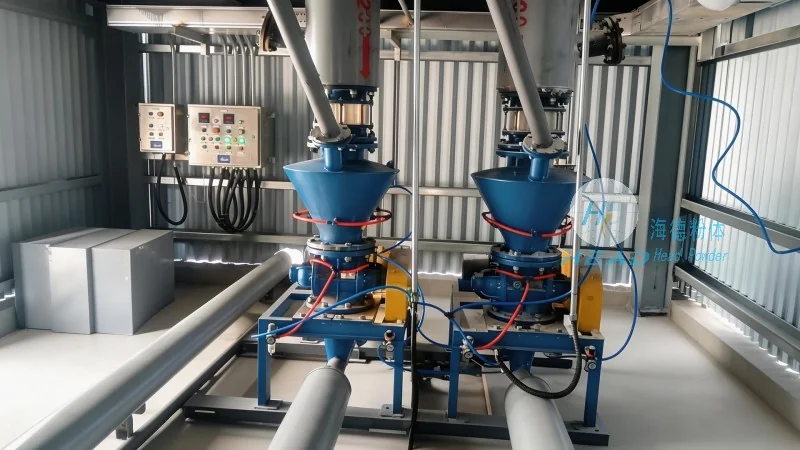
The design of a dilute phase powder conveying system is based on several fundamental principles to ensure optimal performance. The most critical principle is the creation of a dilute phase flow, where the powder particles are suspended in the air stream rather than settling as a dense phase. This suspension is achieved by maintaining a specific air-to-solid ratio, which is typically determined by the particle size, density, and flow characteristics of the material being conveyed. The system's design must also consider the pressure drop across the pipeline, as excessive pressure drop can lead to reduced conveying capacity or increased energy consumption. Engineers use computational fluid dynamics (CFD) and empirical formulas to calculate the optimal air velocity and pipeline diameter for a given material, ensuring that the system operates within its efficient range. Additionally, the system must be designed to handle variations in material properties, such as changes in moisture content or particle size distribution, which can affect the conveying performance. The integration of sensors and control systems in modern dilute phase systems allows for real-time monitoring and adjustment of operational parameters, further enhancing efficiency and reliability.
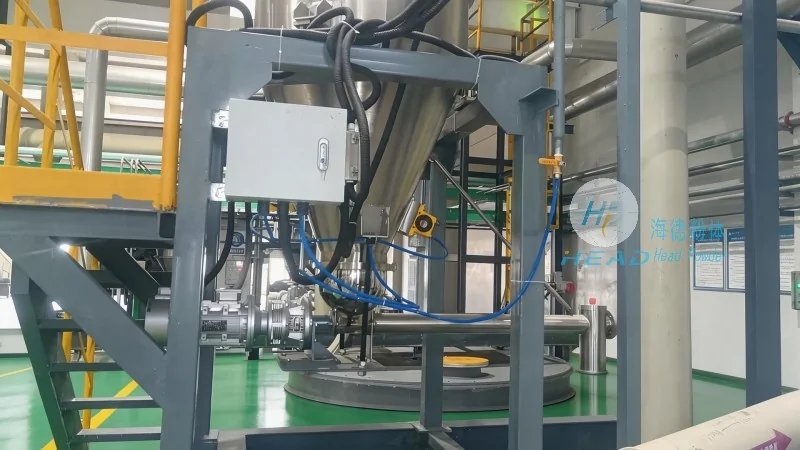
Compared to dense phase or pneumatic conveying systems, dilute phase systems offer several advantages that make them suitable for a wide range of industrial applications. One of the primary advantages is their high conveying capacity, which allows for the transport of large volumes of material over long distances with minimal equipment. The low pressure drop across the pipeline reduces energy consumption, making these systems more cost-effective and environmentally friendly. Additionally, dilute phase systems are capable of handling a variety of materials, including fine powders, which are difficult to transport using other methods. The system's design also minimizes the risk of material degradation or contamination, as the material is suspended in an air stream rather than being in direct contact with the pipeline walls. This is particularly important for sensitive materials, such as pharmaceuticals or food products, where product quality and safety are paramount. Furthermore, dilute phase systems are relatively simple to install and maintain, with fewer moving parts compared to other conveying technologies, reducing downtime and maintenance costs.
The versatility of dilute phase powder conveying systems is demonstrated through their application in various industrial settings. In the chemical industry, these systems are used to transport raw materials like limestone or coal to processing plants, ensuring a continuous supply of feedstock. In the pharmaceutical industry, dilute phase systems are employed to convey active pharmaceutical ingredients (APIs) and excipients, maintaining strict quality control and preventing cross-contamination. The food processing industry utilizes these systems to transport ingredients like flour, sugar, or spices, ensuring hygienic and efficient handling. In the mining sector, dilute phase systems are used to transport ore or tailings from processing facilities to storage or disposal sites, improving operational efficiency and reducing environmental impact. Each application requires a customized design of the system, considering factors such as material properties, conveying distance, and operational requirements. The headpowder engineering company, with its expertise in dilute phase technology, provides tailored solutions to meet the specific needs of different industries, ensuring optimal performance and reliability.
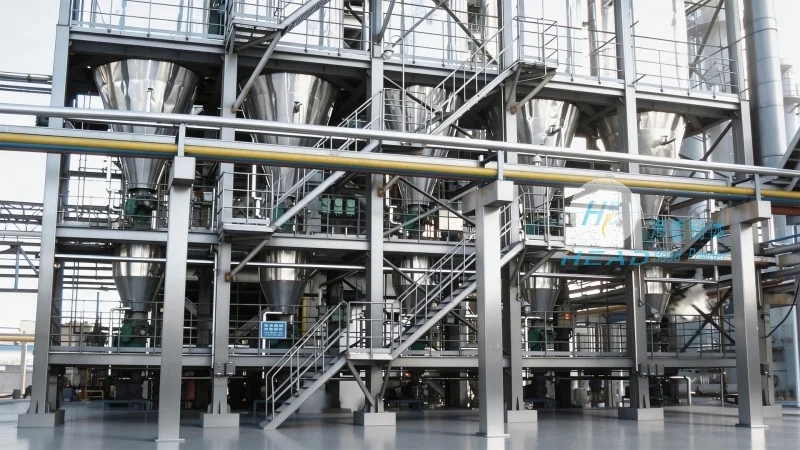
In conclusion, dilute phase powder conveying systems are essential equipment for efficient and reliable material transport in various industrial applications. The design principles, which focus on creating a dilute phase flow and optimizing system components, ensure high conveying capacity, low energy consumption, and minimal material degradation. The headpowder engineering company, based in Shandong, China, specializes in the design and manufacturing of advanced dilute phase systems, providing customized solutions to meet the diverse needs of industries worldwide. As technology advances, future developments in dilute phase systems may include the integration of more sophisticated control systems, materials with improved corrosion resistance, and enhanced energy efficiency, further improving their performance and applicability. The continued evolution of these systems will play a crucial role in supporting the growth and efficiency of industrial operations across various sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top