Understanding the magnesium sulfate powder conveying system is crucial for industries that handle this chemical efficiently and safely. This equipment is specifically designed to transport magnesium sulfate, a common industrial chemical, from one location to another within a production or processing facility. The system plays a vital role in ensuring smooth operations, maintaining product quality, and adhering to safety standards in various applications.
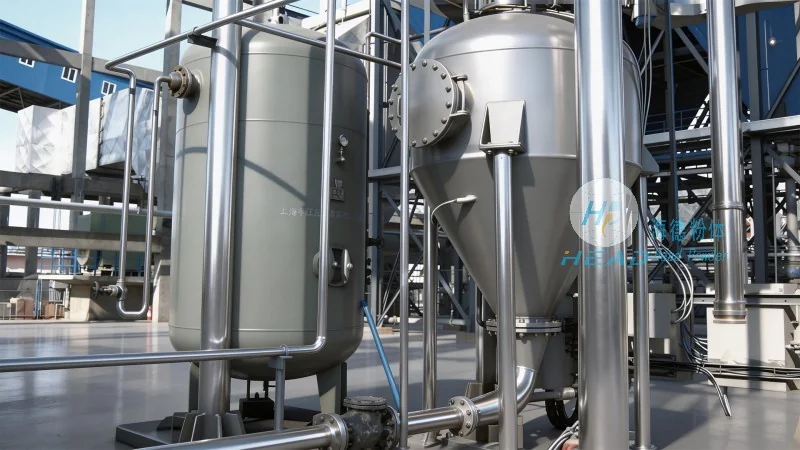
The magnesium sulfate powder conveying system is a specialized piece of industrial equipment used to move powdered magnesium sulfate. This chemical, often used in agriculture, pharmaceuticals, and water treatment, requires careful handling due to its properties. The system typically includes components such as hoppers, conveyors, and control systems, all working in tandem to ensure reliable and consistent material transport. The design of this system is tailored to meet the specific needs of the end-user, considering factors like the volume of material, the distance it needs to be transported, and the environmental conditions of the facility.
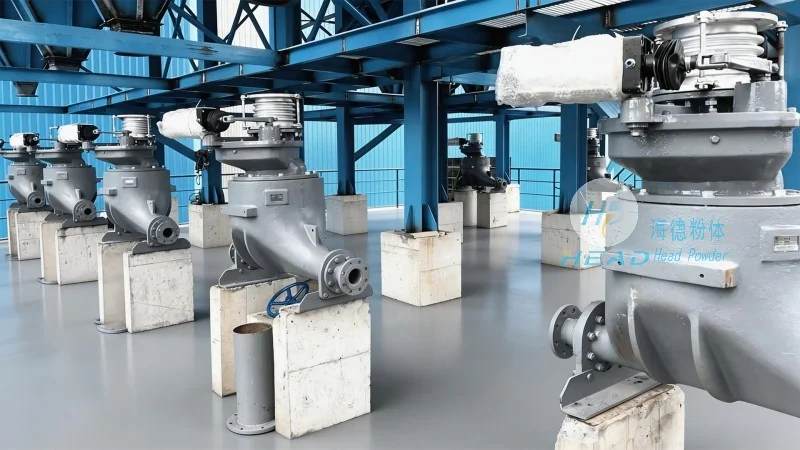
At the core of the magnesium sulfate powder conveying system are several key components that work together to facilitate the transport process. The first component is the hopper, which serves as the storage and feeding unit. It is designed to hold the magnesium sulfate powder and release it in a controlled manner into the conveyor system. The hopper is often equipped with a discharge valve or feeder to regulate the flow of material, preventing overloading or clogging. Next, the conveyor system itself, which can be of various types such as screw conveyors, pneumatic conveyors, or belt conveyors, depending on the specific requirements. Screw conveyors are commonly used for horizontal or slight incline transport, while pneumatic conveyors are ideal for long-distance or vertical transport due to their ability to handle fine powders without clogging. The control system is another critical component, which includes sensors, valves, and a control panel to monitor and adjust the operation of the system in real-time. This ensures that the conveying process is efficient, safe, and meets the desired output parameters.
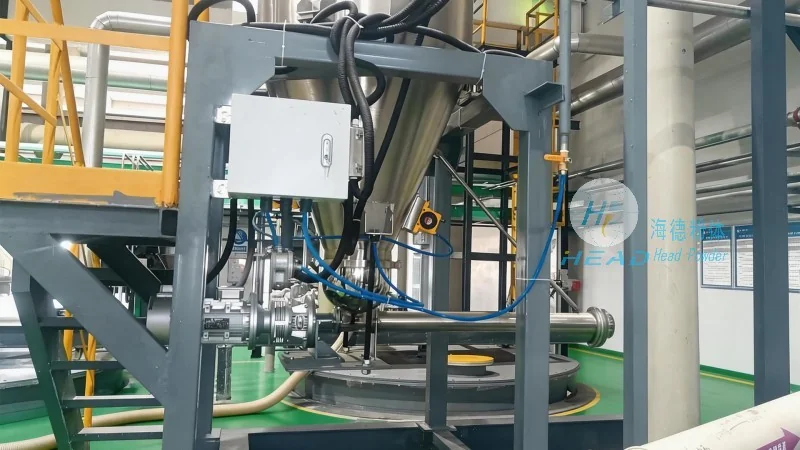
The design principles of the magnesium sulfate powder conveying system are centered on efficiency, safety, and reliability. One of the primary principles is the prevention of material buildup and clogging, which can lead to system downtime and product contamination. This is achieved through the use of appropriate hopper designs, such as conical or wedge-shaped hoppers, which promote material flow and prevent arching or bridging. The conveyor system is also designed with smooth surfaces and appropriate angles to minimize friction and ensure consistent material movement. Another key principle is the consideration of dust control and environmental safety. Magnesium sulfate is a fine powder that can generate dust during handling, which poses health risks and environmental concerns. Therefore, the system is often equipped with dust collection systems, such as cyclones or baghouses, to capture and remove airborne particles. Additionally, the system is designed to comply with industrial safety standards, including explosion-proof features for pneumatic conveyors in hazardous environments. The control system is designed to provide real-time monitoring and alarm capabilities, alerting operators to any issues that may arise, such as blockages or overloads.
The magnesium sulfate powder conveying system finds applications in various industries where this chemical is used. In the agricultural sector, it is used as a fertilizer, and the system helps in transporting it from storage to application equipment. In the pharmaceutical industry, it is used as an excipient or in the production of certain medications, and the system ensures that the powder is handled hygienically and efficiently. In water treatment, it is used to adjust pH levels and control algae growth, and the system facilitates its transport to treatment plants. The benefits of using this system include improved operational efficiency, reduced labor costs, and enhanced safety. By automating the powder transport process, the system minimizes the risk of human error and exposure to the chemical. It also ensures consistent product quality by maintaining a controlled flow of material, which is crucial for downstream processes. Furthermore, the system's design allows for easy maintenance and cleaning, reducing downtime and increasing the overall lifespan of the equipment.
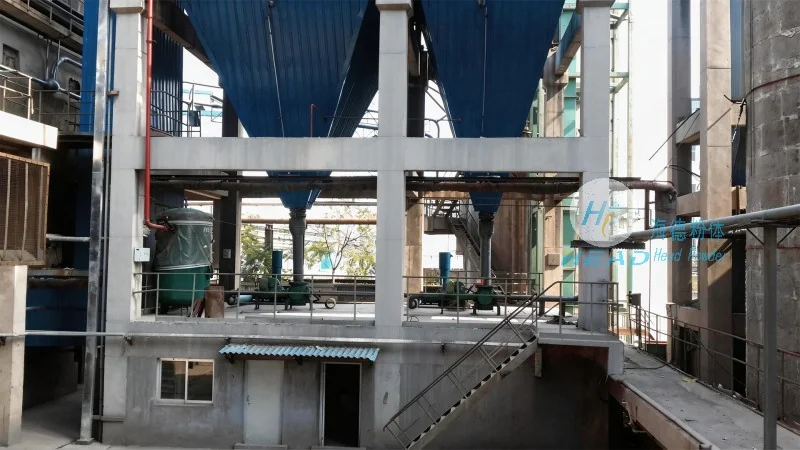
In conclusion, the magnesium sulfate powder conveying system is a vital piece of industrial equipment that plays a crucial role in the efficient and safe handling of this chemical. The design principles behind the system focus on preventing clogging, controlling dust, and ensuring safety, all while maintaining operational efficiency. The key components, including hoppers, conveyors, and control systems, work together to achieve these goals. The system's applications span various industries, providing benefits such as improved productivity, reduced costs, and enhanced safety. For companies dealing with magnesium sulfate, investing in a well-designed conveying system is essential to meet production demands and maintain compliance with industry standards. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, offers high-quality systems tailored to meet the specific needs of their clients, ensuring reliable and efficient powder transport in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top