When it comes to the efficient handling and transportation of fine sand and stone powders, specialized equipment plays a crucial role in industrial processes. The fine sand and stone powder conveying system equipment, as offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to address the unique challenges associated with these materials. This article delves into the core components, operational mechanisms, and design principles that underpin such systems, providing a comprehensive understanding for those seeking to optimize material handling in their operations.
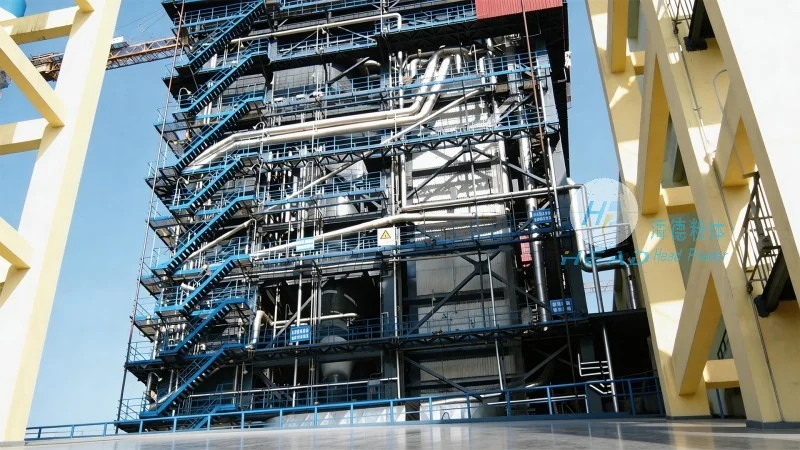
The fine sand and stone powder conveying system equipment typically comprises several critical components that work in tandem to ensure reliable and efficient material transport. These components include feed hoppers, which are designed to evenly distribute the material into the conveying system, preventing blockages and ensuring consistent flow. The conveyor itself, often utilizing screw or pneumatic mechanisms, is engineered to handle the abrasive and fine nature of the sand and stone powders. Additionally, control systems and sensors are integrated to monitor the flow rate, pressure, and other operational parameters, allowing for real-time adjustments and maintenance. The system may also feature dust collection and filtration units to maintain air quality and comply with environmental regulations. Each component is carefully selected and designed to withstand the harsh conditions associated with handling these materials, ensuring durability and long-term performance.
The design of fine sand and stone powder conveying systems is guided by several key principles aimed at maximizing efficiency, minimizing downtime, and ensuring safety. One of the primary principles is the optimization of material flow, which involves designing the system to minimize friction and resistance. This is achieved through the use of smooth, corrosion-resistant surfaces and appropriate conveyor angles. Another critical principle is the integration of robust sealing and dust control measures. Fine powders are prone to dispersion, and effective sealing prevents contamination and ensures that the system operates within safe environmental limits. The design also emphasizes modularity, allowing for easy maintenance and component replacement without extensive system downtime. Furthermore, energy efficiency is a key consideration, with systems engineered to use minimal power while maintaining high throughput. These design principles collectively contribute to a system that is not only effective in conveying materials but also sustainable and cost-effective over its operational lifespan.
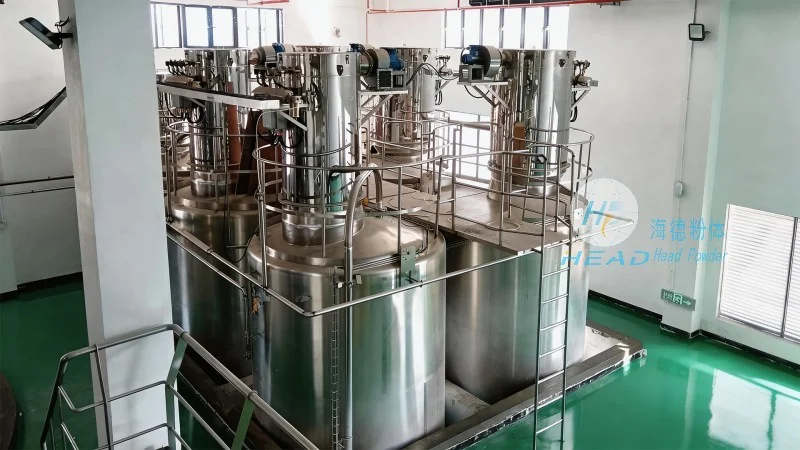
Implementing a fine sand and stone powder conveying system equipment offers numerous operational advantages across various industries. The primary benefit is the significant reduction in labor costs associated with manual handling of these materials. Automated systems ensure consistent and reliable transport, reducing the risk of human error and improving overall productivity. Additionally, the systems enhance safety by minimizing exposure to dust and other hazards, creating a healthier work environment. The equipment is particularly well-suited for applications in construction, mining, and manufacturing, where large volumes of sand and stone powders are processed. For example, in the construction industry, these systems are used to transport sand for concrete production, while in mining operations, they facilitate the handling of crushed stone and fine powders for further processing. The adaptability of the system allows it to be customized to meet the specific needs of different applications, making it a versatile solution for a wide range of industrial requirements.
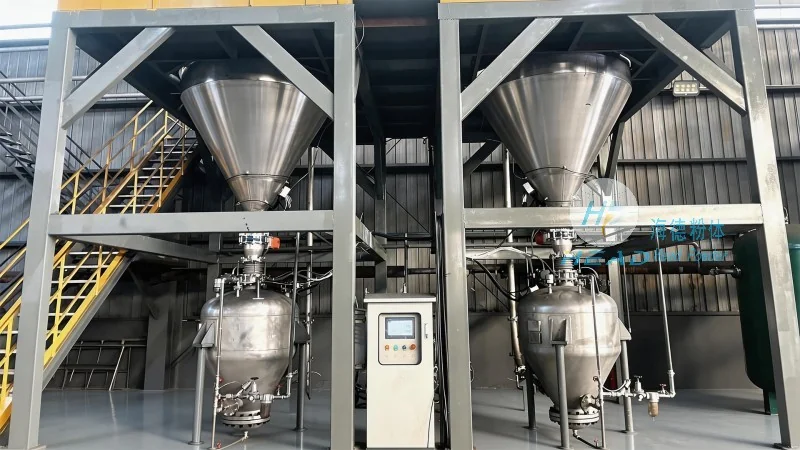
Proper maintenance is essential to ensure the longevity and optimal performance of fine sand and stone powder conveying systems. Regular inspections and maintenance procedures are recommended to identify and address potential issues before they escalate into major problems. This includes checking for wear and tear on conveyor components, ensuring proper lubrication of moving parts, and cleaning the system to prevent the buildup of material residues. The use of high-quality materials, such as stainless steel or specialized alloys, contributes to the system's durability and resistance to corrosion. Additionally, the integration of advanced monitoring systems allows for predictive maintenance, enabling timely repairs and reducing unexpected downtime. By adhering to a comprehensive maintenance schedule, users can extend the operational life of the equipment and maintain its efficiency, ensuring that it continues to deliver reliable performance over the long term.
In conclusion, the fine sand and stone powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient solution for handling these challenging materials. Through careful design, robust components, and adherence to key operational principles, the system ensures reliable transport, enhances safety, and improves overall productivity. The integration of advanced control systems and maintenance strategies further contributes to the system's longevity and cost-effectiveness. For industries that rely on the consistent handling of fine sand and stone powders, investing in such a system is a strategic decision that can significantly enhance operational efficiency and sustainability. As the demand for efficient material handling solutions continues to grow, the fine sand and stone powder conveying system equipment stands as a testament to the innovation and expertise of Shandong HeadPowder Engineering Co., Ltd.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top