Understanding the Molybdenum Oxide Powder Conveying System Equipment and Its Design Principles
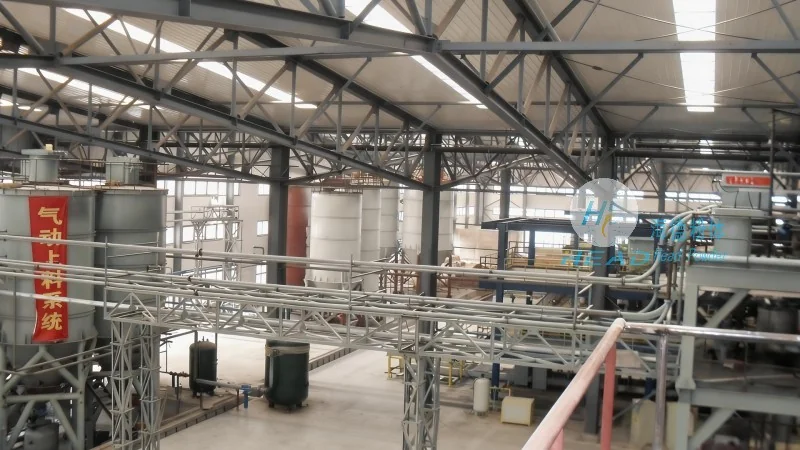
The molybdenum oxide powder conveying system equipment is a specialized industrial solution designed to handle and transport molybdenum oxide powder efficiently and safely. This system is crucial in various industrial applications where molybdenum oxide is used as a raw material or additive. The equipment is engineered to address the unique challenges associated with handling fine powders, ensuring consistent flow, minimal dust generation, and optimal material handling performance. As a key component in material processing, the molybdenum oxide powder conveying system plays a vital role in maintaining product quality and operational efficiency.
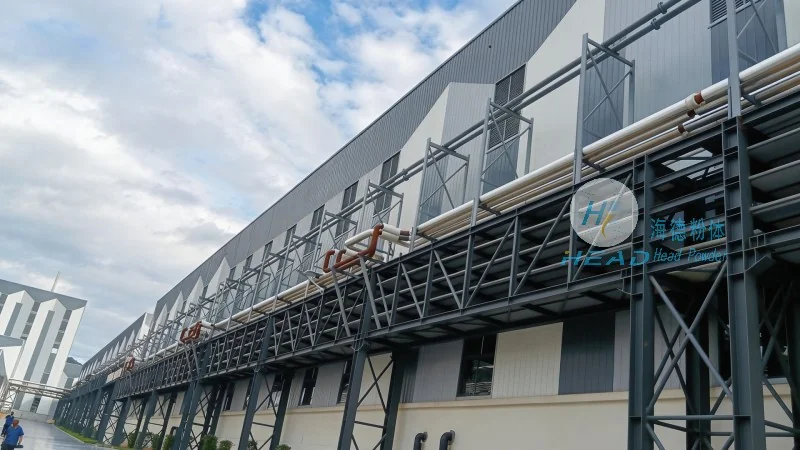
The molybdenum oxide powder conveying system typically consists of several core components that work in tandem to achieve effective material transport. These components include a hopper for material storage, a feeder to control the flow rate, a conveying mechanism such as a pneumatic or mechanical conveyor, and a dust collection system to ensure environmental compliance. Each component is carefully selected and integrated to meet the specific requirements of molybdenum oxide powder, which is known for its fine particle size and potential for static charge accumulation. The hopper is designed with smooth, non-stick surfaces to prevent material buildup and ensure uniform feeding. The feeder, often a rotary valve or screw feeder, regulates the flow of powder into the conveying line, preventing overloading and maintaining consistent pressure. The conveying mechanism, whether pneumatic (using air pressure) or mechanical (using belts or screws), is chosen based on the material's properties and the required transport distance. The dust collection system, including filters and cyclones, captures any airborne particles, protecting both the environment and personnel from exposure to molybdenum oxide dust.
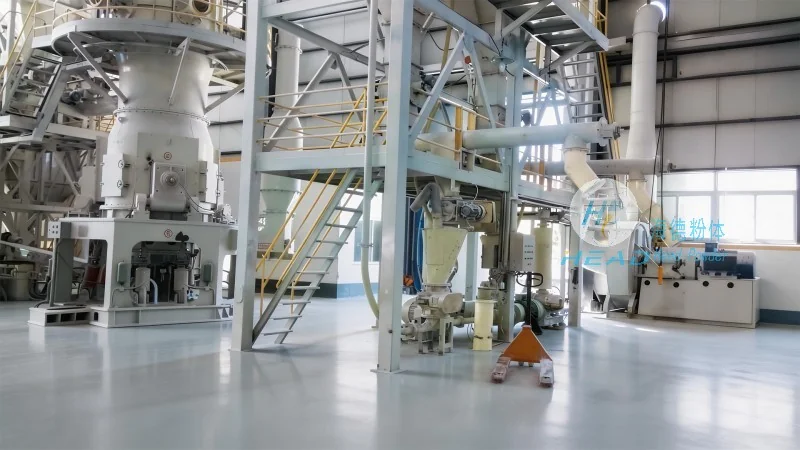
The design principles of the molybdenum oxide powder conveying system are centered on ensuring safety, efficiency, and reliability. One of the primary design considerations is the prevention of material degradation and contamination. Molybdenum oxide is sensitive to moisture and can react with certain materials, so the system is constructed from materials that are compatible with the powder, such as stainless steel or specialized coatings that resist corrosion and prevent adhesion. The system also incorporates static control measures, such as grounding and antistatic additives, to prevent static buildup that could lead to dust explosions or material sticking. Another critical design principle is the minimization of pressure drop and energy consumption. The conveying system is optimized to reduce friction and resistance, ensuring that the material moves smoothly through the pipeline with minimal energy input. This is achieved through the use of appropriate pipe diameters, smooth internal surfaces, and efficient conveying mechanisms. Additionally, the system is designed for easy maintenance and cleaning, with access points for inspection and cleaning of components like the hopper and feeder. This ensures that the system can be kept in optimal condition, reducing downtime and maintaining consistent performance over time.
The molybdenum oxide powder conveying system is widely used in various industrial sectors, including the production of molybdenum compounds, steel alloys, and catalysts. In these applications, the system ensures that molybdenum oxide is delivered to processing equipment in a controlled and consistent manner, which is essential for maintaining product quality and process stability. The benefits of using this system include improved material handling efficiency, reduced labor costs, and enhanced safety due to the enclosed design that minimizes dust exposure. Additionally, the system helps in maintaining a clean and safe working environment, which is crucial for compliance with environmental regulations. The ability to handle fine powders without clogging or blockages makes the system particularly suitable for molybdenum oxide, which has a tendency to agglomerate under certain conditions. By providing a reliable and efficient means of transporting molybdenum oxide powder, the system contributes to the overall productivity and profitability of industrial operations.
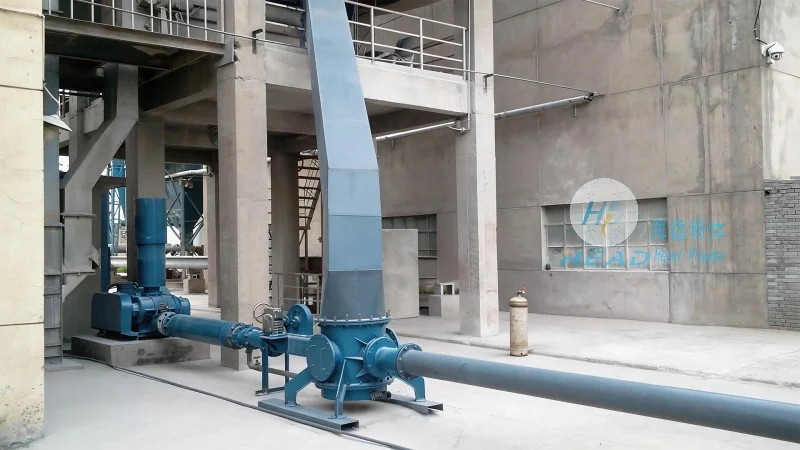
In conclusion, the molybdenum oxide powder conveying system equipment is a sophisticated industrial solution that combines advanced design principles with robust construction to handle the unique challenges of molybdenum oxide powder. The system's components are carefully selected and integrated to ensure efficient, safe, and reliable material transport, which is critical for maintaining product quality and operational efficiency in various industrial applications. As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its molybdenum oxide powder conveying systems meet the highest standards of performance and safety. Based in Shandong, China, HeadPowder leverages its expertise and experience to deliver reliable solutions that enhance the productivity and sustainability of industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top