HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced gravity dust removal and pneumatic conveying systems. These systems are engineered to efficiently handle bulk material transport while ensuring optimal air quality and operational reliability. The following overview details the core components, technical advantages, and practical applications of such systems, tailored to meet diverse industrial needs.
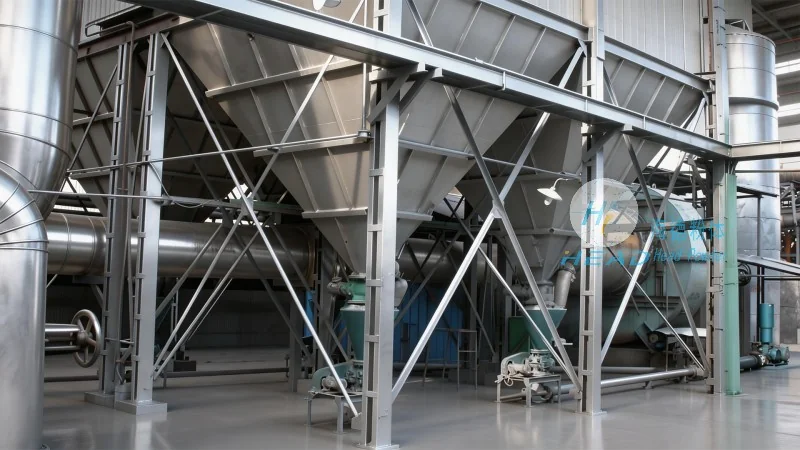
The gravity dust removal and pneumatic conveying system integrates several key components to achieve efficient material handling and air purification. At its foundation is a gravity dust collector, which uses gravitational forces to separate dust particles from the air stream. This component is typically equipped with a hopper and a discharge mechanism to collect and store the collected dust. Complementing this is the pneumatic conveying system, which utilizes air pressure to transport bulk materials from one location to another. The system may include a blower or compressor to generate the necessary airflow, along with pipelines and control valves to direct the material flow. Together, these components form a cohesive solution that addresses both dust control and material transport challenges in industrial settings.
One of the primary advantages of this system is its high efficiency in dust removal. The gravity dust collector employs a simple yet effective design that minimizes energy consumption while maximizing dust capture rates. By leveraging gravitational forces, the system reduces the need for high-pressure air, leading to lower operational costs and increased energy savings. Additionally, the pneumatic conveying portion of the system offers flexibility in material transport, allowing for long-distance or complex route transport without the need for multiple transfer points. The integration of both functions into a single system also streamlines operations, reducing the complexity of material handling processes and enhancing overall productivity. The system is designed to handle a wide range of materials, from fine powders to bulk solids, ensuring versatility across various industrial applications.
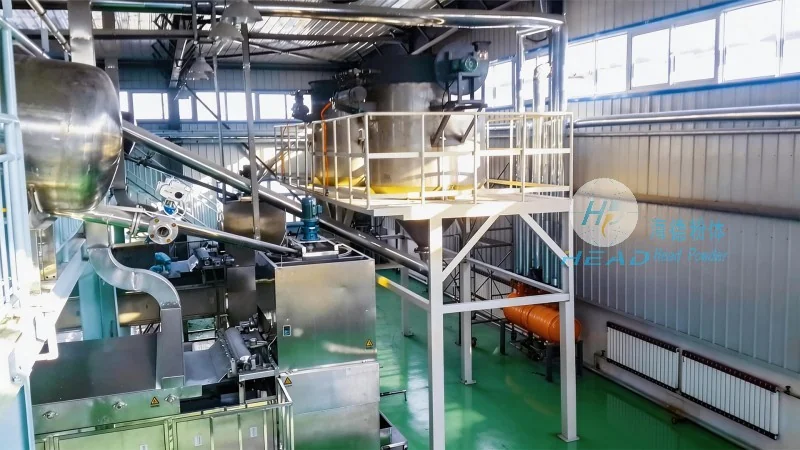
These gravity dust removal and pneumatic conveying systems are widely used in industries such as cement, chemical, and food processing. In cement plants, for example, the system efficiently removes dust from raw material handling and transports finished products or byproducts to storage facilities. In chemical manufacturing, it aids in the safe handling of powders and prevents contamination by capturing airborne particles. The food industry also benefits from this technology, as it ensures compliance with hygiene standards while maintaining the quality of processed materials. Each application is tailored to the specific requirements of the industry, with adjustments made to the system's capacity, pressure, and material handling capabilities to meet operational demands.
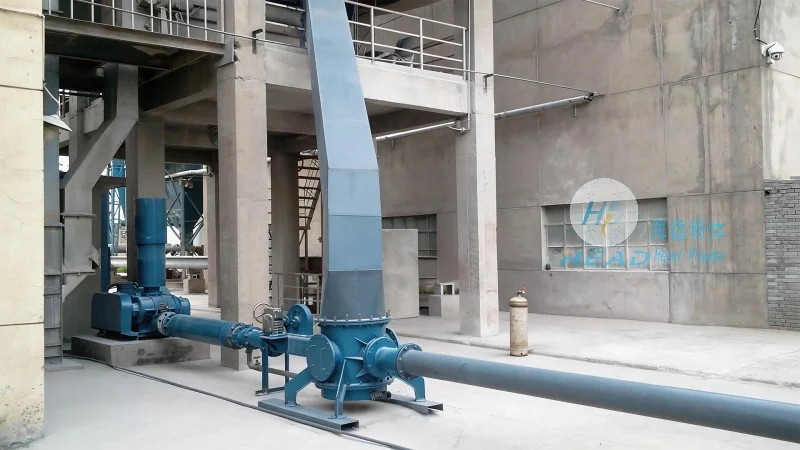
HeadPowder provides comprehensive engineering services to customize these systems according to client-specific needs. The company's team of experts works closely with clients to assess their operational requirements, material characteristics, and site constraints. Through detailed analysis and design, the system is optimized for maximum performance and reliability. This includes selecting appropriate equipment, determining the optimal airflow rates, and ensuring compliance with industry standards and regulations. The customization process also considers factors such as space availability, existing infrastructure, and budget constraints, ensuring that the final solution is both effective and cost-efficient. HeadPowder's commitment to quality and innovation ensures that each system is built to withstand the demands of industrial environments and deliver long-term value.
Gravity dust removal and pneumatic conveying systems represent a sophisticated solution for modern industrial material handling and air quality management. By combining efficient dust capture with reliable material transport, these systems enhance operational efficiency, reduce environmental impact, and improve workplace safety. HeadPowder Engineering Co., Ltd., based in Shandong, China, stands as a trusted partner in delivering such advanced systems. With a focus on engineering excellence and customer satisfaction, the company continues to innovate and provide tailored solutions that meet the evolving needs of industries worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top