HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the food additives industry. Our systems are engineered to meet stringent industry standards, ensuring safe, efficient, and hygienic handling of various food additives, including powders, granules, and other bulk materials. The company, Shandong HeadPowder Engineering Co., Ltd., has established itself as a trusted partner in the food processing sector, delivering customized solutions that enhance operational efficiency and product quality.
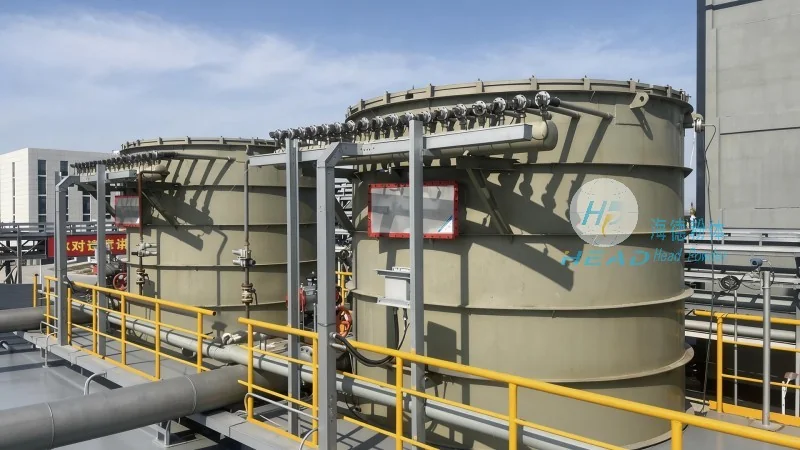
Our pneumatic conveying systems for food additives are built with precision and attention to detail, incorporating several key features that set them apart in the market. First, the systems utilize positive pressure or negative pressure conveying methods, depending on the specific requirements of the food additive being handled. This flexibility allows for the transportation of materials over long distances with minimal degradation. The equipment is constructed from high-quality, food-grade materials such as stainless steel, ensuring compliance with regulatory standards like FDA and EU directives. Additionally, our systems are equipped with advanced control panels that provide real-time monitoring and adjustment capabilities, enabling operators to optimize performance and maintain consistent product quality. The design also incorporates features like dust collection and filtration systems, which are crucial for maintaining a clean and safe working environment in food processing facilities.
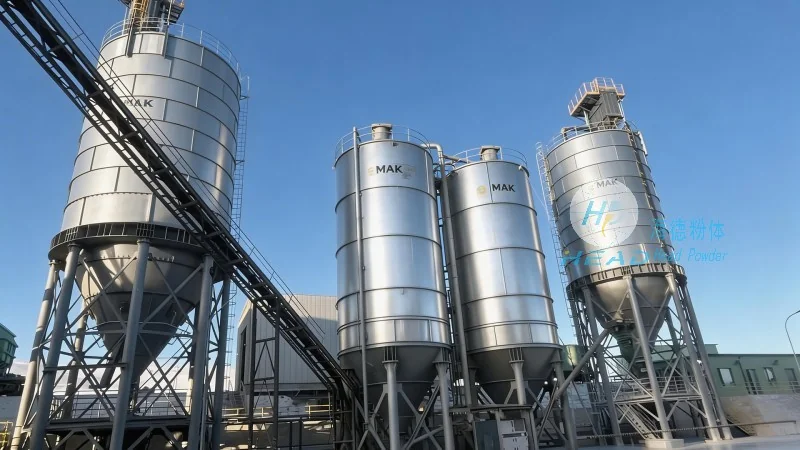
Adopting a pneumatic conveying system for food additives offers numerous benefits that can significantly improve the overall efficiency and safety of food processing operations. One of the primary advantages is the reduction in manual handling, which minimizes the risk of contamination and product loss. The automated system ensures consistent material flow, reducing variability in batch processing and improving product uniformity. Furthermore, the enclosed design of the conveying system prevents cross-contamination between different additives, which is critical in maintaining product integrity and meeting regulatory requirements. The energy efficiency of pneumatic conveying systems also contributes to lower operational costs over time, as they consume less power compared to traditional methods like bucket elevators or belt conveyors. Another key benefit is the ability to handle a wide range of material types, from fine powders to larger granules, without the need for multiple pieces of equipment. This versatility makes our systems suitable for various food additive applications, including flavorings, colorants, preservatives, and other additives used in the food industry.
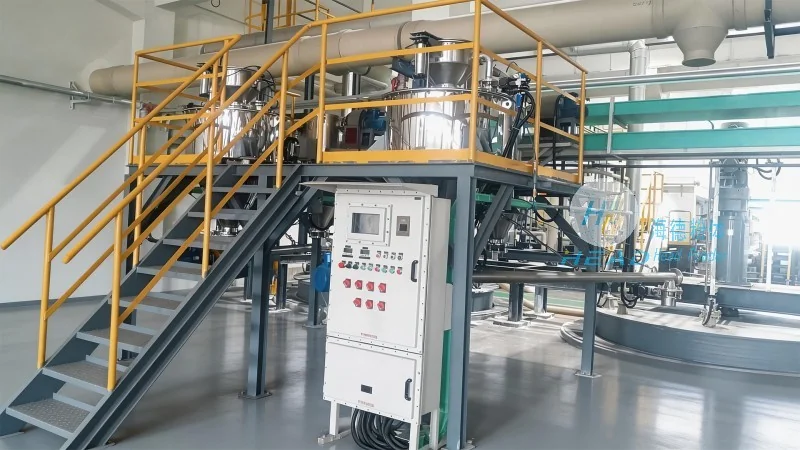
At HeadPowder, we understand that each food processing facility has unique requirements. Therefore, our pneumatic conveying systems are highly customizable to fit specific operational needs. We work closely with clients to design systems that integrate seamlessly with existing production lines, ensuring minimal disruption during installation and operation. Our engineering team conducts thorough assessments of the client's facility, including material characteristics, processing capacity, and space constraints, to develop a tailored solution. The systems can be integrated with other equipment such as mixers, blenders, and packaging machines, creating a fully automated production line. Additionally, we offer options for different conveying modes, such as dilute phase and dense phase, to optimize material handling based on the specific properties of the food additive. The customization also extends to the control systems, which can be programmed to match the client's operational protocols and provide detailed data on system performance.
Ensuring the highest standards of quality and compliance is a top priority at HeadPowder. Our pneumatic conveying systems for food additives are manufactured in accordance with international quality management systems, such as ISO 9001. The production process involves rigorous quality control checks at every stage, from material selection to final assembly. All components are tested for durability, corrosion resistance, and hygienic performance to ensure they meet the demanding requirements of the food industry. The systems are also designed to be easy to clean and maintain, with features like CIP (Clean-in-Place) compatibility, which allows for thorough sanitation without disassembling the equipment. This is essential for maintaining compliance with hygiene regulations and preventing the growth of bacteria or other contaminants. Furthermore, our systems are certified to meet various international standards, including those set by the FDA and EU, providing clients with the confidence that their food additive handling processes are safe and compliant.
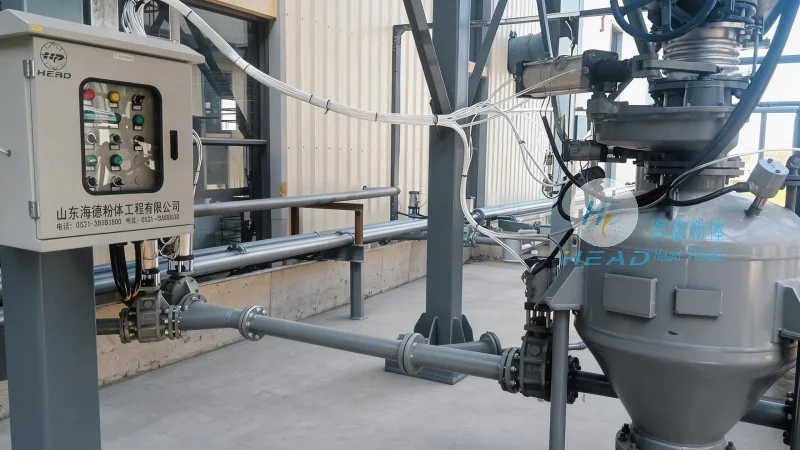
HeadPowder provides comprehensive support throughout the entire lifecycle of our pneumatic conveying systems. From initial design and engineering to on-site installation and commissioning, our team of experienced technicians ensures that the system is installed correctly and operates at peak performance. The installation process is carried out with strict adherence to safety protocols and industry best practices, minimizing downtime for the client's operations. After installation, we offer ongoing maintenance and support services to ensure the system continues to function optimally. Our technical support team is available to address any issues that may arise, providing timely solutions and spare parts as needed. We also provide training to the client's staff on the operation and maintenance of the system, ensuring they can maximize its benefits and extend its lifespan. The after-sales support includes regular inspections, performance audits, and system upgrades to keep the equipment up-to-date with the latest technological advancements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top