For industrial applications requiring efficient and reliable material handling, the use of pneumatic conveying systems has become increasingly prevalent. Among these, systems designed for handling sodium hexafluorophosphate (NaPF₆) present unique challenges due to the chemical's properties, such as its reactivity and the need for precise control during transport. This article provides a comprehensive overview of the pneumatic conveying systems tailored for sodium hexafluorophosphate, highlighting key components, operational principles, and the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field.
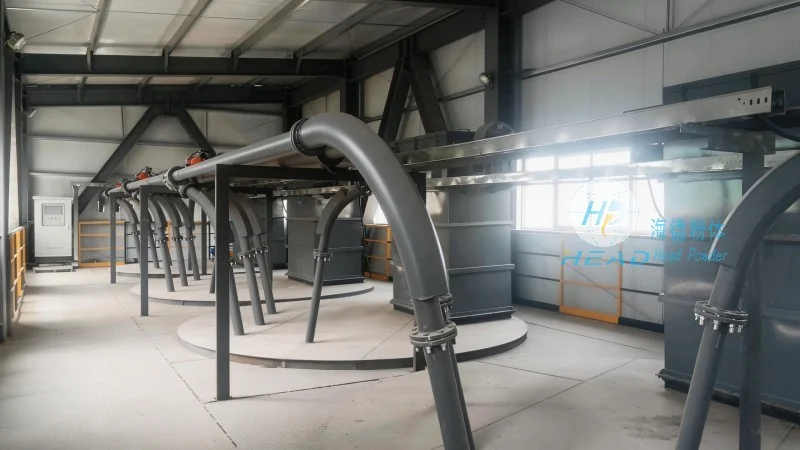
The pneumatic conveying system for sodium hexafluorophosphate typically consists of several critical components that work in tandem to ensure safe and efficient material transport. These include the material hopper, which serves as the storage and feeding unit, equipped with a rotary valve to control the flow of NaPF₆. The hopper is designed with corrosion-resistant materials to withstand the chemical's acidic nature and prevent contamination. A positive displacement blower or a high-pressure air compressor provides the necessary air pressure to move the material through the conveying line. The pipeline system, often made of stainless steel or other inert materials, is engineered to minimize friction and prevent material degradation. Additionally, a filter system is integrated to capture any fine particles and maintain air quality, while a receiver or discharge hopper at the end of the line collects the conveyed material. Each component is carefully selected and configured to meet the specific requirements of sodium hexafluorophosphate, ensuring optimal performance and safety throughout the conveying process.
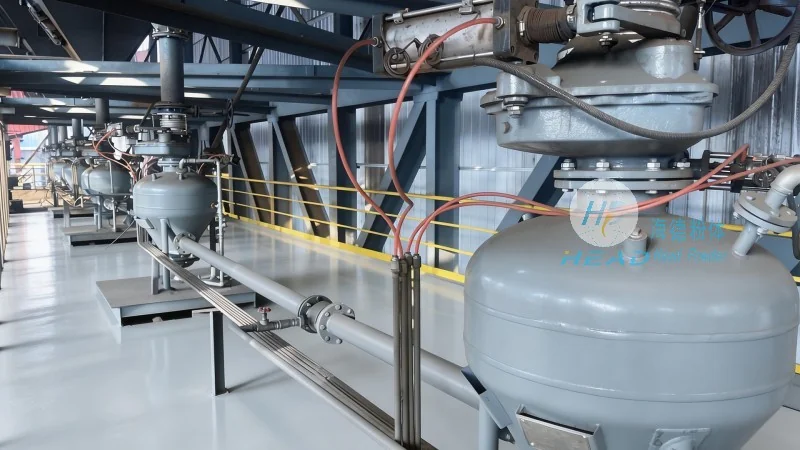
The operation of a sodium hexafluorophosphate pneumatic conveying system follows a systematic process that ensures consistent and controlled material movement. The system starts with the material being fed from the hopper into the conveying line via the rotary valve. The blower then generates the required air pressure, which propels the NaPF₆ particles through the pipeline. The velocity of the air and the particle size are critical factors that determine the efficiency of the conveying process. To maintain a stable flow, the system often incorporates a venturi or a pressure regulator to adjust air pressure as needed. Safety measures are paramount in handling sodium hexafluorophosphate, as the chemical can be hazardous if not managed properly. The system is equipped with pressure relief valves to prevent over-pressurization and explosion risks. Additionally, the use of explosion-proof motors and electrical components is standard to mitigate fire hazards. Regular maintenance and monitoring of the system are also essential to ensure compliance with safety regulations and to prolong the system's lifespan. Shandong HeadPowder Engineering Co., Ltd. adheres to strict safety protocols and industry standards when designing and implementing these systems, providing clients with reliable and secure solutions.
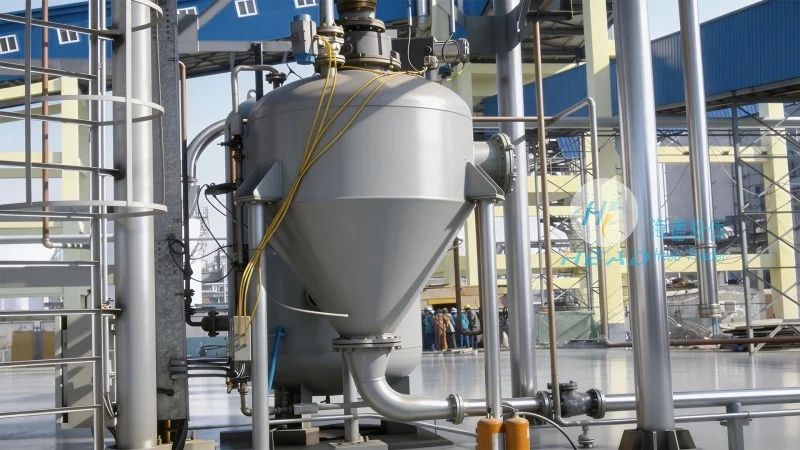
Given the diverse industrial applications of sodium hexafluorophosphate, the pneumatic conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. are highly customizable to meet specific client needs. The company works closely with clients to understand their operational requirements, such as the volume of material to be conveyed, the distance of transport, and the desired discharge point. Based on this information, the system design is tailored to optimize performance and minimize energy consumption. For example, the system can be configured with different hopper sizes, pipeline diameters, or air pressure levels to accommodate varying production scales. The flexibility extends to the integration of additional features, such as dust collection systems or material drying units, depending on the client's process needs. This customization ensures that the conveying system not only meets the functional requirements but also enhances overall operational efficiency. The company's expertise in material handling and pneumatic technology allows them to provide tailored solutions that address the unique challenges associated with sodium hexafluorophosphate, making their systems suitable for a wide range of industrial applications.
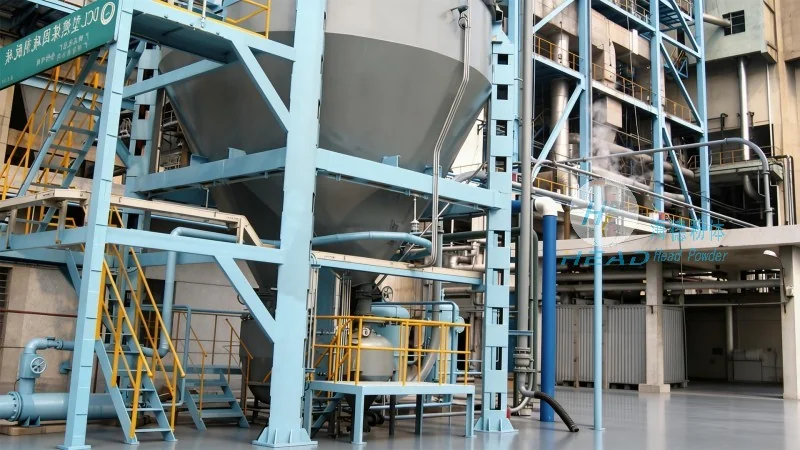
Implementing a specialized pneumatic conveying system for sodium hexafluorophosphate offers several advantages over traditional material handling methods. One of the primary benefits is the reduction in manual handling, which minimizes the risk of exposure to the chemical and improves workplace safety. The automated system also enhances operational efficiency by reducing downtime and increasing throughput. By eliminating the need for manual loading and unloading, the system allows for continuous production, which is crucial for maintaining high productivity. Additionally, the use of a closed system prevents dust emissions and environmental contamination, aligning with modern industrial standards for sustainability. The precise control over material flow ensures consistent product quality, which is essential for applications where NaPF₆ is used as a key ingredient. The system's ability to handle fine particles without clogging the pipeline further enhances its reliability. Shandong HeadPowder Engineering Co., Ltd.'s systems are designed to deliver these advantages, providing clients with a cost-effective and efficient solution for their sodium hexafluorophosphate handling needs. The company's commitment to quality and innovation ensures that their pneumatic conveying systems are not only effective but also durable and long-lasting.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top