Understanding the functionality and design principles of sand and granular material conveying lines is crucial for industries that rely on efficient material handling. These systems are engineered to transport loose, free-flowing materials such as sand, gravel, and other granular substances from one location to another, often over considerable distances. The core purpose of such equipment is to enhance productivity, reduce labor costs, and improve safety in material handling operations.
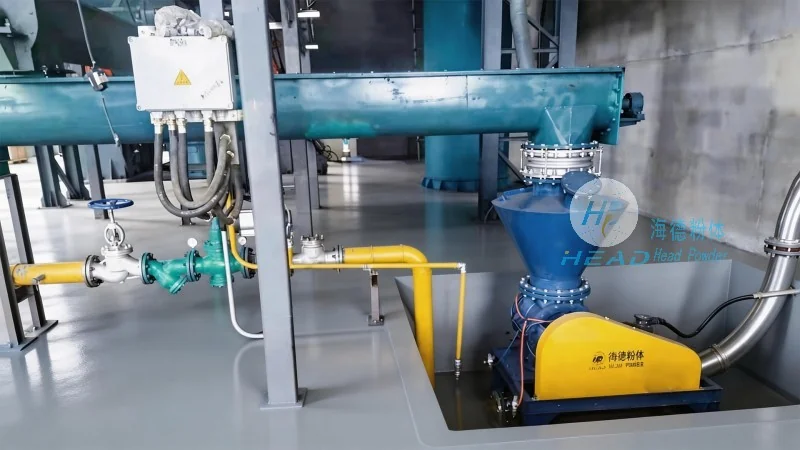
A typical sand and granular material conveying line consists of several key components that work in tandem to ensure smooth material transport. The primary elements include a feeding mechanism, a conveyor system (such as a belt conveyor or screw conveyor), a drive unit, and a control system. The feeding mechanism is responsible for introducing the material into the conveyor, while the conveyor itself moves the material along its path. The drive unit provides the necessary power to operate the conveyor, and the control system manages the operation, ensuring the system runs efficiently and safely.
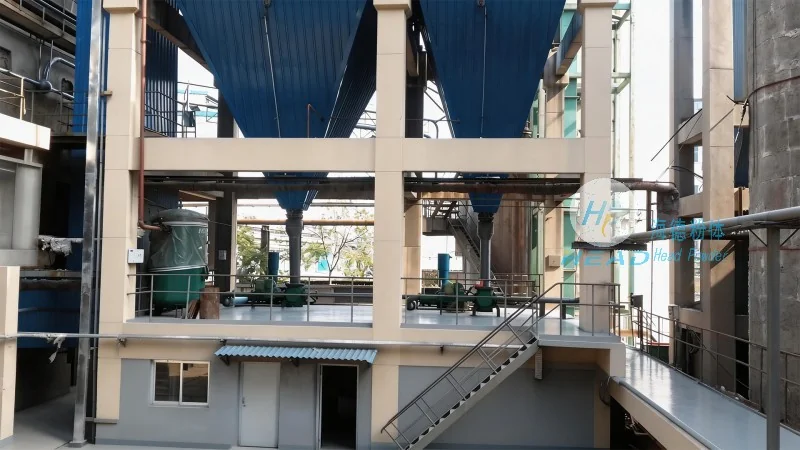
The design of a sand and granular material conveying line is guided by several fundamental principles aimed at optimizing performance and reliability. First, the system must be designed to handle the specific characteristics of the material being conveyed, including its size, density, and flowability. This involves selecting appropriate conveyor types and components that can accommodate the material's properties without causing blockages or damage. Second, the design emphasizes energy efficiency and operational cost reduction. Engineers aim to minimize power consumption while maximizing throughput, which is achieved through proper sizing of the conveyor, selection of efficient drive systems, and optimization of the material flow path. Third, safety is a critical design consideration. Conveying lines are equipped with safety features such as emergency stop buttons, protective guards, and overload protection to prevent accidents and ensure compliance with safety regulations. Additionally, the design must account for the environmental conditions where the system will operate, such as temperature, humidity, and exposure to dust or debris, to ensure long-term durability and performance.
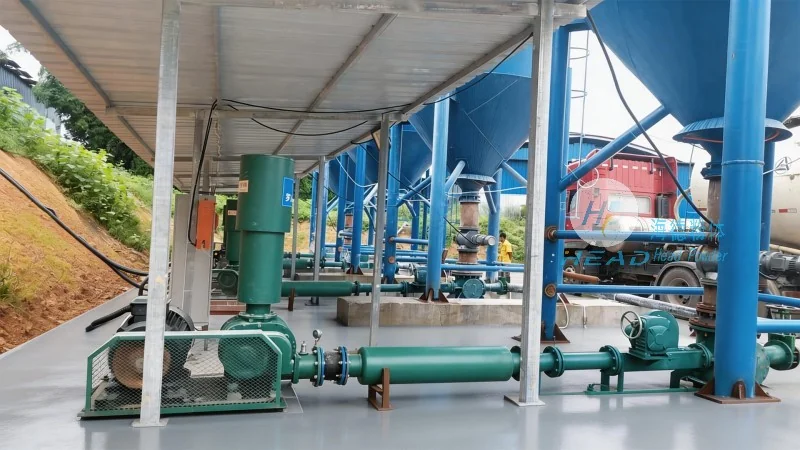
Each component of a sand and granular material conveying line plays a vital role in the overall operation. The feeding mechanism, often a hopper or a feeder, ensures a consistent and controlled flow of material into the conveyor. This prevents overloading and ensures the conveyor operates at its optimal capacity. The conveyor system, which can be a belt conveyor, screw conveyor, or bucket elevator, is chosen based on the material's characteristics and the required transport distance. Belt conveyors are commonly used for long-distance horizontal or slight incline transport, while screw conveyors are ideal for vertical or inclined transport of smaller granular materials. The drive unit, typically an electric motor connected to a gearbox or direct drive system, provides the mechanical power to move the conveyor. The control system, which may include sensors, controllers, and monitoring devices, manages the speed, direction, and operation of the conveyor, allowing for adjustments based on the material load and system conditions.
Sand and granular material conveying lines are widely used across various industries, including construction, mining, agriculture, and manufacturing. In the construction industry, these systems are essential for transporting sand, gravel, and other aggregates to building sites, ensuring a steady supply of materials for concrete production and road construction. In mining operations, they are used to move ore and other minerals from extraction sites to processing facilities, improving the efficiency of material handling and reducing the time and cost associated with manual transport. In agriculture, conveying lines are employed to transport grains, seeds, and other agricultural products from storage facilities to processing plants or distribution centers. Additionally, in manufacturing, they are used to transport raw materials and finished products within production lines, enhancing the overall efficiency of the manufacturing process.
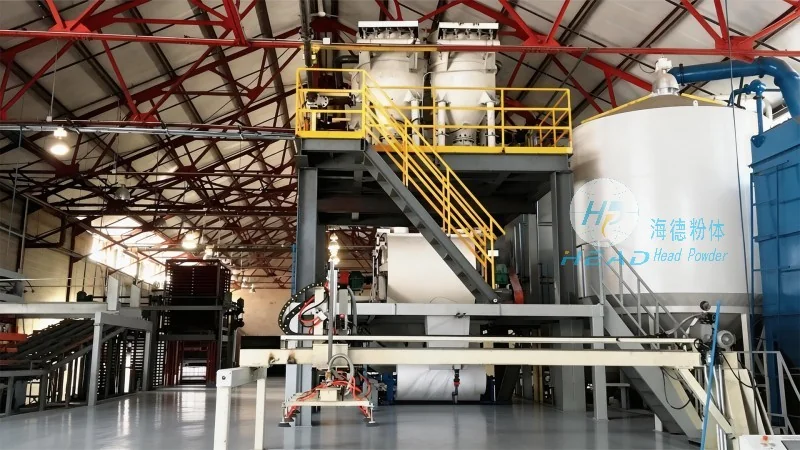
Implementing a sand and granular material conveying line offers numerous benefits to businesses. First, it significantly increases productivity by automating the material handling process, reducing the need for manual labor and minimizing downtime. This leads to higher throughput and faster production cycles. Second, it improves safety by eliminating the need for workers to handle heavy or bulky materials manually, reducing the risk of injuries and accidents. Third, it enhances cost-effectiveness by reducing labor costs, minimizing material loss due to spillage or damage, and optimizing energy consumption. Fourth, it improves the quality of the material handling process by ensuring consistent and controlled transport, which is crucial for maintaining product quality and meeting industry standards. Finally, it provides flexibility in terms of material transport, allowing for easy integration with existing production lines and the ability to adapt to changing production needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top