Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial and agricultural applications. The pneumatic conveying system designed for transporting this material efficiently is a critical piece of equipment for many processing facilities. This article explores what such a system entails and the underlying design principles that ensure its optimal performance, with a focus on systems developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
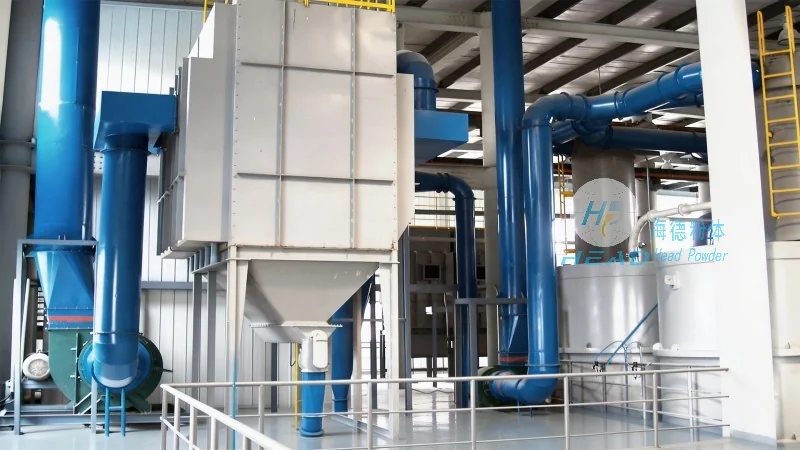
The heptahydrate magnesium sulfate pneumatic conveying system is a specialized equipment setup used to transport dry or bulk heptahydrate magnesium sulfate from one location to another within a processing plant or between different facilities. Unlike traditional mechanical conveyors, which rely on belts, screws, or buckets, pneumatic conveying systems use compressed air or other gases to move the material through a pipeline. This method offers several advantages, including the ability to transport materials over long distances, through vertical or horizontal paths, and even around obstacles, making it highly versatile for complex layouts.
At its core, a heptahydrate magnesium sulfate pneumatic conveying system consists of several key components that work in tandem to ensure smooth material transport. The primary components include the material hopper or feeder, the air compressor or blower, the conveying pipeline, the control valves, and the receiving hopper or silo. Each component plays a crucial role in the overall operation of the system.
The material hopper or feeder is responsible for storing and feeding the heptahydrate magnesium sulfate into the system. It is typically designed with a hopper that allows for uniform material flow, often equipped with a rotary valve or a star feeder to control the discharge rate. This ensures that the material is introduced into the pipeline at a consistent rate, preventing blockages and maintaining system efficiency.
The air compressor or blower is the heart of the pneumatic system, providing the necessary pressure and airflow to move the material through the pipeline. The choice of compressor depends on the system's requirements, such as the material's properties, the distance to be conveyed, and the desired flow rate. High-pressure blowers are often used for short-distance or high-volume conveying, while low-pressure systems are suitable for longer distances or when handling more delicate materials.
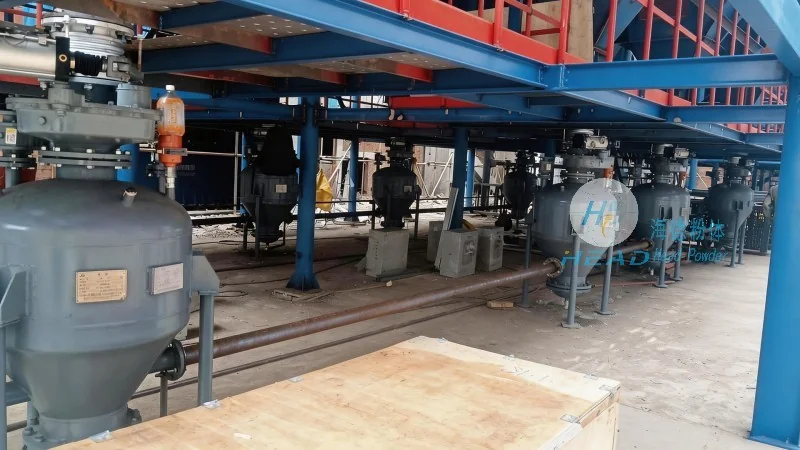
The conveying pipeline is a network of pipes that transports the material and air mixture. The material is suspended in the air stream, and the pipeline is designed to handle the pressure and flow conditions. The pipeline may include elbows, tees, and other fittings to direct the material to the desired destination. The material of construction is critical, as it must be resistant to corrosion and wear from the heptahydrate magnesium sulfate and the air stream.
The control valves, including the inlet and outlet valves, are used to regulate the flow of air and material. These valves allow operators to control the system's operation, such as starting and stopping the conveyor, adjusting the flow rate, and diverting material to different destinations. The control system may include sensors to monitor pressure, flow, and material level, providing real-time feedback to the operator.
The receiving hopper or silo is where the heptahydrate magnesium sulfate is deposited after being conveyed. It is designed to store the material safely and efficiently, often with a discharge system to transfer the material to the next processing step or for packaging.
The design of a heptahydrate magnesium sulfate pneumatic conveying system involves several key principles to ensure efficient and reliable operation. The first principle is the selection of the appropriate air velocity. The air velocity must be high enough to suspend the material particles in the air stream but not so high as to cause excessive wear on the pipeline or equipment. The optimal air velocity depends on the particle size, density, and shape of the heptahydrate magnesium sulfate, as well as the system's pressure and flow rate.
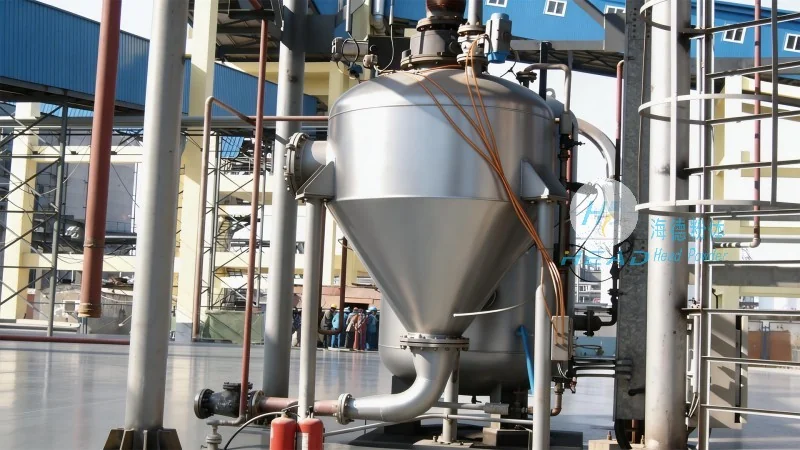
The second principle is the consideration of the system's pressure drop. The pressure drop in the pipeline is a measure of the energy required to move the material through the system. It is influenced by factors such as the pipeline length, diameter, fittings, and the material's properties. The design must ensure that the pressure drop is within acceptable limits to avoid excessive energy consumption or system failure. Proper sizing of the pipeline and the use of efficient fittings can help minimize the pressure drop.
The third principle is the selection of the right material of construction. The heptahydrate magnesium sulfate is a corrosive material, and the conveying system must be resistant to its chemical properties. Materials such as stainless steel, polyethylene, or special alloys are commonly used for the pipeline and equipment components to prevent corrosion and ensure long-term durability.
The fourth principle is the consideration of the system's capacity and flow rate. The design must be able to handle the required material throughput, ensuring that the system can meet the production demands without bottlenecks. The flow rate is determined by the air velocity, the material's bulk density, and the pipeline diameter. Proper sizing of the components, including the hopper, feeder, and compressor, is essential to achieve the desired flow rate.
The fifth principle is the inclusion of safety features. The pneumatic conveying system must be designed with safety in mind, including pressure relief valves, emergency shut-off valves, and proper ventilation to prevent the buildup of dust or fumes. These features help ensure the safety of the operators and the integrity of the system.
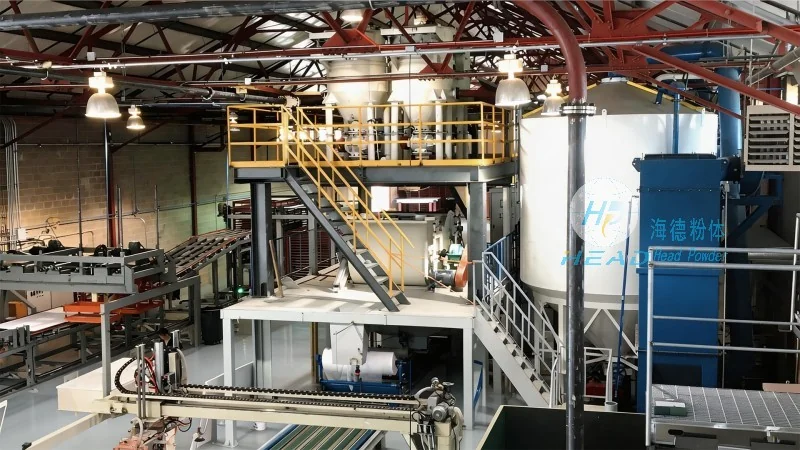
The heptahydrate magnesium sulfate pneumatic conveying system is used in a variety of applications, including the chemical industry, agriculture, and pharmaceuticals. In the chemical industry, it is used to transport the material between processing units, such as from a dryer to a packaging line. In agriculture, it is used to transport the material from storage facilities to farms or processing plants. In the pharmaceutical industry, it is used to transport the material to manufacturing facilities for further processing.
One of the primary benefits of the pneumatic conveying system is its ability to transport heptahydrate magnesium sulfate over long distances without the need for intermediate storage or handling. This reduces the risk of material loss or contamination and improves overall efficiency. Another benefit is the system's ability to handle a wide range of material properties, including different particle sizes and shapes, making it suitable for various applications.
The system also offers cost savings compared to traditional mechanical conveyors. The lack of moving parts in the pipeline reduces maintenance costs and increases the system's lifespan. Additionally, the system can be easily integrated into existing facilities, minimizing the need for major construction or modifications.
The heptahydrate magnesium sulfate pneumatic conveying system is a critical piece of equipment for many processing facilities, providing an efficient and reliable method for transporting this important chemical compound. The design of the system involves careful consideration of several key principles, including air velocity, pressure drop, material of construction, capacity, and safety features. By adhering to these principles, manufacturers can ensure that the system operates at optimal levels, meeting the production demands while minimizing costs and risks. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems, leveraging years of experience to deliver high-quality solutions tailored to the specific needs of their clients in China and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top