For food manufacturers, the efficient and safe handling of food additives is a critical aspect of production processes. Pneumatic conveying technology offers a reliable solution for transporting these materials, ensuring precision and maintaining product integrity. This article explores the fundamental principles of pneumatic conveying systems, the various classification methods used, and their practical applications in the food additive industry.
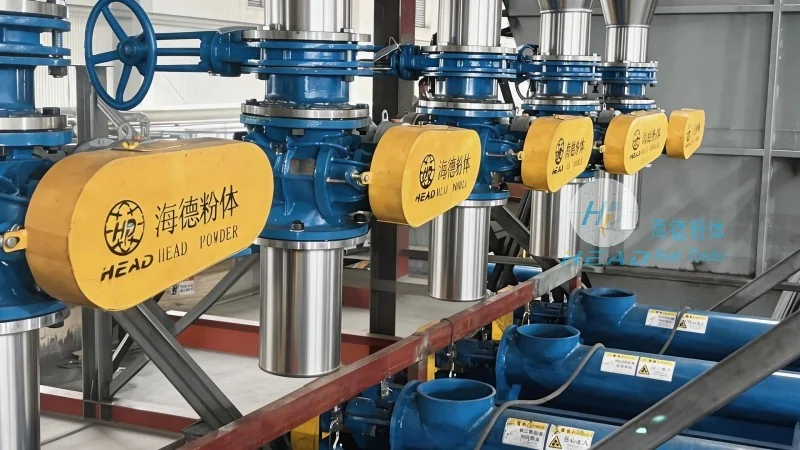
Pneumatic conveying works by using a gas stream, typically air, to transport solid particles through a pipeline. The core principle involves creating a pressure differential between the inlet and outlet of the system. As air is introduced into the conveying line, it creates a flow that lifts and propels the solid particles forward. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational reliability. The system's design, including the type of air flow (positive or negative pressure) and the particle characteristics, directly impacts its efficiency and suitability for different food additive types.
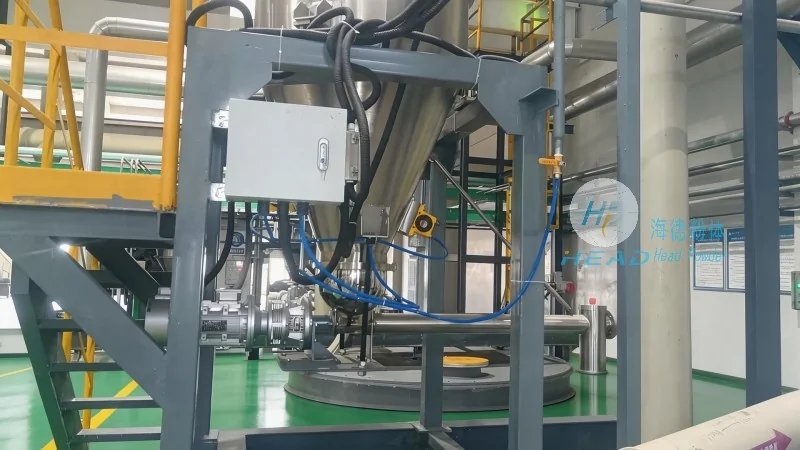
Pneumatic conveying systems are broadly classified into two main categories: positive pressure and negative pressure systems. Positive pressure systems operate by blowing air into the conveying line, pushing the material forward. These systems are ideal for long-distance transport and are commonly used for bulk materials with high moisture content or those that are prone to dusting. Negative pressure systems, on the other hand, draw material into the system using a vacuum, pulling it through the pipeline. This method is often preferred for applications requiring a dust-free environment or when handling materials that are sensitive to air exposure.
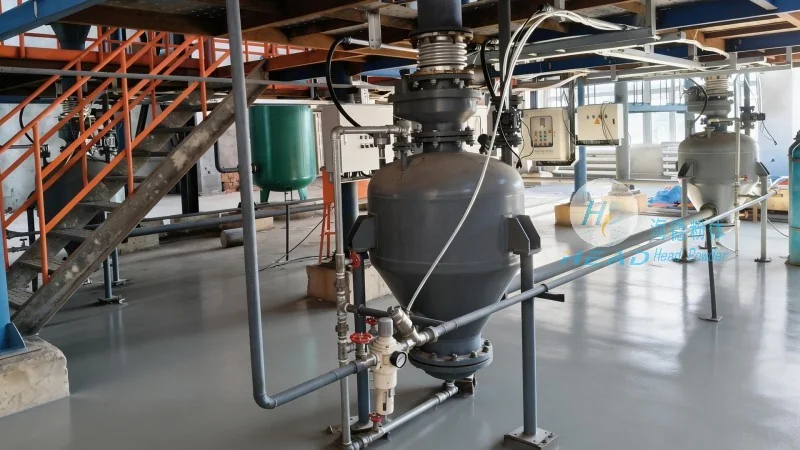
The versatility of pneumatic conveying makes it suitable for a wide range of food additive applications. For instance, in the production of flavor enhancers and colorants, pneumatic systems can efficiently transport powders like monosodium glutamate or food colorings from storage silos to processing equipment. This ensures consistent dosing and reduces the risk of contamination. Similarly, in the handling of preservatives and antioxidants, the system's ability to maintain a controlled environment prevents degradation of sensitive ingredients. Additionally, the technology is used in the blending of multiple additives, allowing for precise mixing ratios to meet product specifications.
Implementing pneumatic conveying in food additive processing offers several advantages. These include improved hygiene, as the enclosed system minimizes exposure to contaminants and reduces the risk of cross-contamination. It also enhances safety by eliminating manual handling of powders, which can cause respiratory issues or dust explosions. However, the selection of a suitable system depends on factors such as the particle size, density, and moisture content of the additives. For example, fine powders may require higher air velocities to prevent clogging, while larger particles might benefit from a combination of positive and negative pressure to optimize flow.
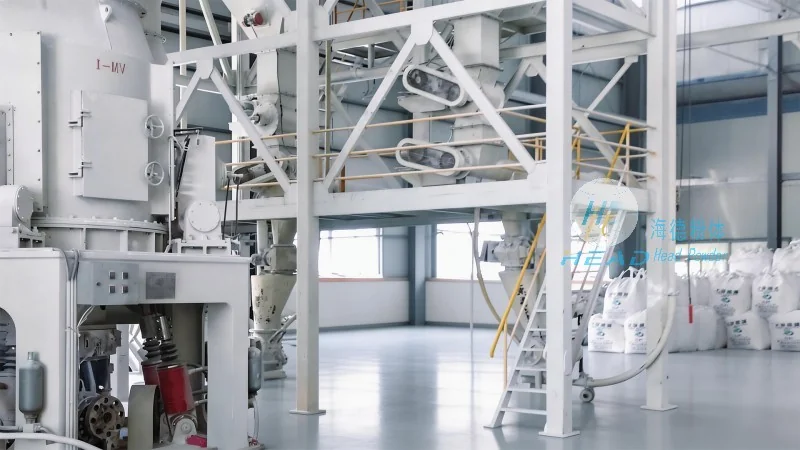
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the food additive industry. With a focus on precision and safety, HeadPowder's systems are engineered to meet the stringent requirements of food processing facilities. The company's expertise lies in customizing solutions that address specific challenges, such as handling sensitive ingredients or ensuring compliance with regulatory standards. By leveraging advanced technology and a deep understanding of material behavior, HeadPowder delivers reliable and efficient conveying systems that enhance production efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top