When it comes to transporting denitrification urea via pneumatic systems, the choice between positive pressure and negative pressure conveying is a critical decision that impacts efficiency, cost, and operational safety. Understanding the fundamental differences and specific applications of each method is essential for selecting the most suitable solution for your industrial needs. This article will explore the key distinctions between positive and negative pressure systems, providing insights into how to differentiate between them and make an informed choice.
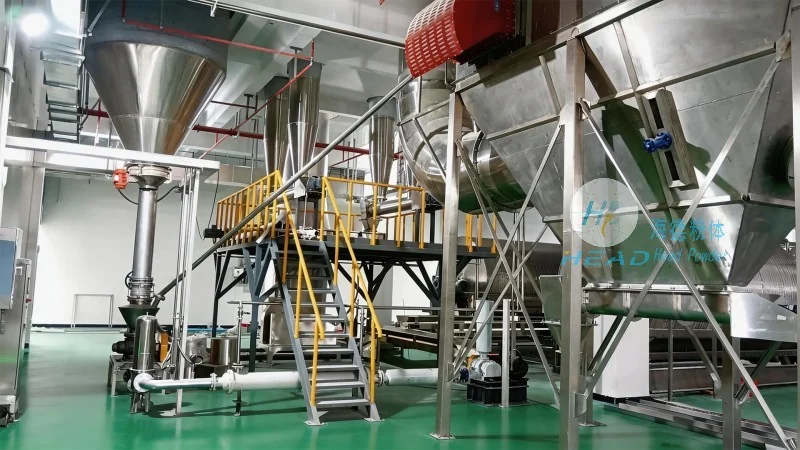
Pneumatic conveying is a widely used method for transporting bulk materials like denitrification urea, which is essential in flue gas desulfurization and denitrification processes in power plants and industrial facilities. The primary goal is to move the urea from storage to the injection point efficiently and reliably. Two main types of pneumatic conveying systems are commonly employed: positive pressure and negative pressure. Each has its own advantages and limitations, making the selection process dependent on factors such as material properties, distance, system complexity, and environmental considerations.
Positive pressure pneumatic conveying systems operate by blowing air or a gas mixture into the conveying line, creating a pressure higher than the ambient air pressure. The material is then drawn into the line by the pressure differential and transported to the destination. This method is particularly effective for transporting materials over longer distances or through complex piping networks. The positive pressure system typically uses a blower or compressor at the inlet to generate the necessary pressure, ensuring consistent material flow. The advantages of positive pressure systems include their ability to handle abrasive or sticky materials, as the high pressure helps to maintain material velocity and prevent blockages. Additionally, these systems are generally more suitable for applications where the material needs to be delivered to multiple points or where the receiving point is at a higher elevation than the source.
Positive pressure systems are characterized by their high-pressure operation, which allows for the transportation of materials at higher velocities compared to negative pressure systems. This results in shorter conveying times and the ability to handle materials with higher moisture content or larger particle sizes. The system components, including the blower, filter, and control valves, are typically located at the inlet of the conveying line, making them easily accessible for maintenance. The positive pressure method is also less susceptible to external air infiltration, which can be a concern in negative pressure systems, especially when dealing with dust or other airborne contaminants. However, the high-pressure operation may require more robust equipment and higher energy consumption, which can increase operational costs.
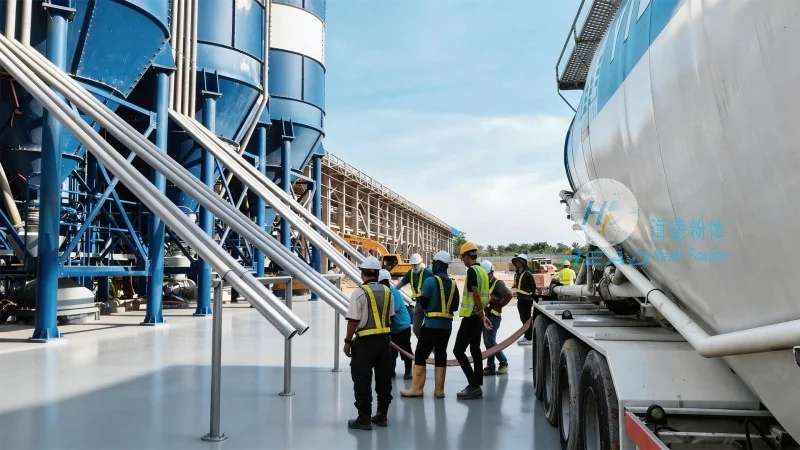
Negative pressure pneumatic conveying, also known as vacuum conveying, operates by creating a vacuum in the conveying line, which draws the material from the source into the line. The material is then transported to the receiving point by the vacuum created by a vacuum pump or fan. This method is commonly used for shorter distances and when the receiving point is at a lower elevation than the source. Negative pressure systems are particularly effective for handling fine powders or materials that are sensitive to pressure, as the low-pressure environment reduces the risk of material degradation or agglomeration. The system components, including the vacuum pump and filter, are typically located at the receiving end of the line, which can help to contain dust and prevent environmental contamination.
Negative pressure systems are characterized by their low-pressure operation, which results in lower energy consumption compared to positive pressure systems. However, the lower velocity of material flow may require longer conveying times, especially for longer distances. The system is also more susceptible to external air infiltration, which can affect the material's quality and the overall efficiency of the process. The vacuum pump and filter are critical components in negative pressure systems, as they need to maintain a consistent vacuum level and filter out any dust or particles that may be drawn into the system. The lower pressure environment also makes it easier to handle materials that are prone to caking or agglomeration, as the reduced pressure helps to prevent the formation of clumps.
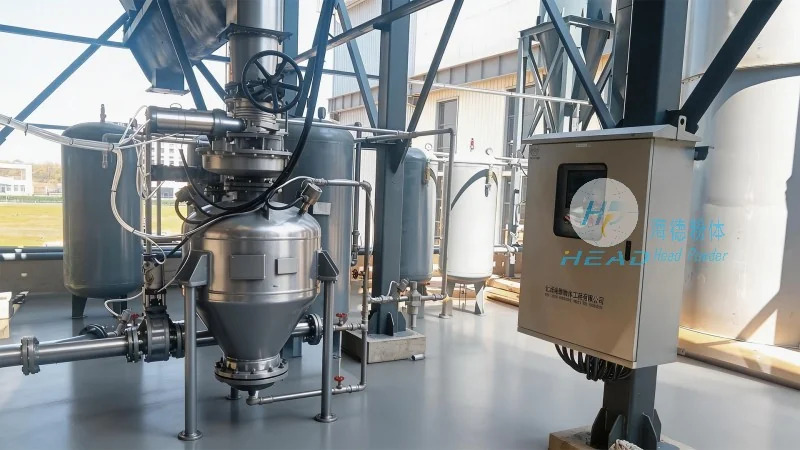
The primary way to distinguish between positive and negative pressure pneumatic conveying systems is based on the pressure differential within the conveying line. In positive pressure systems, the pressure inside the line is higher than the ambient air pressure, while in negative pressure systems, the pressure inside the line is lower than the ambient air pressure. Another key difference is the location of the main air-moving equipment: positive pressure systems use a blower or compressor at the inlet, while negative pressure systems use a vacuum pump at the receiving end. The application requirements also play a significant role in the selection. For example, positive pressure systems are often preferred for long-distance or high-elevation transport, while negative pressure systems are suitable for short-distance or low-elevation transport. The material properties, such as particle size, moisture content, and flowability, also influence the choice, as each system has specific advantages in handling different material characteristics.
When deciding between positive and negative pressure pneumatic conveying for denitrification urea, several factors need to be considered. The first is the distance between the source and the receiving point. Longer distances typically favor positive pressure systems due to their higher material velocity and ability to maintain flow over extended lengths. Shorter distances, on the other hand, may be more efficiently handled by negative pressure systems. The elevation difference is another critical factor; if the receiving point is at a higher elevation than the source, positive pressure systems are generally more suitable, as they can overcome the gravitational force more effectively. The material characteristics, including particle size, moisture content, and flowability, also impact the system choice. For example, positive pressure systems are better suited for handling coarse or abrasive materials, while negative pressure systems are more appropriate for fine powders that are prone to caking. The system complexity and maintenance requirements are also important considerations. Positive pressure systems may require more robust equipment and regular maintenance of the blower, while negative pressure systems may need more frequent filter changes due to the higher risk of dust accumulation.
Selecting the appropriate pneumatic conveying system for denitrification urea is a crucial step in ensuring efficient and reliable operation of flue gas treatment processes. Positive pressure and negative pressure systems each offer unique advantages and are suited to different applications. By understanding the fundamental differences between them and considering factors such as distance, elevation, material properties, and operational requirements, you can make an informed decision that optimizes performance and minimizes costs. Whether you opt for a positive pressure or negative pressure system, the key is to choose a solution that aligns with your specific industrial needs and operational goals. For further assistance in selecting the right pneumatic conveying system for your denitrification urea application, you can contact Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for bulk material handling in China.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top