HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the fertilizer industry. This article explores the various types of pneumatic conveying systems utilized in fertilizer transport and their practical applications, highlighting the technological advancements and operational efficiencies they offer.
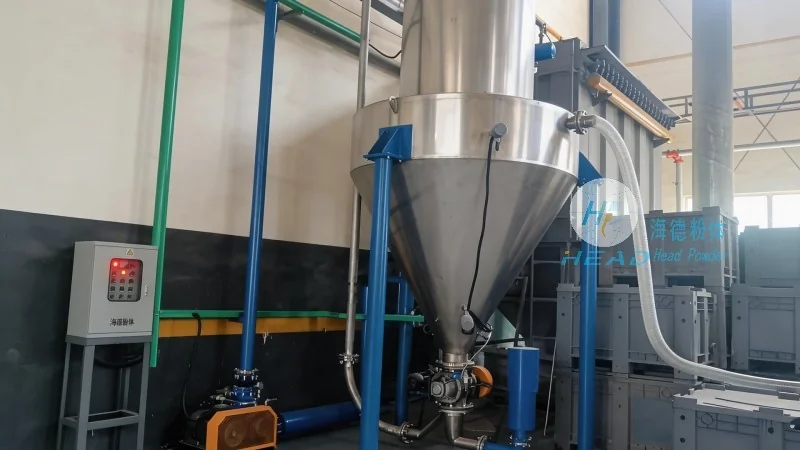
Pneumatic conveying systems have become indispensable in modern fertilizer handling and transportation due to their ability to efficiently move bulk materials like granular or powdered fertilizers over long distances with minimal human intervention. These systems operate by using air or gas to transport solid particles through a pipeline network, offering advantages such as reduced equipment wear, lower maintenance costs, and enhanced safety compared to traditional mechanical conveyors. The choice of system type depends on factors including material characteristics, distance, and throughput requirements, making it crucial for fertilizer producers and distributors to select the most suitable solution for their specific needs.
There are primarily two main categories of pneumatic conveying systems used in fertilizer transport: pressure and vacuum systems. Each type has distinct characteristics and is suited to different operational scenarios.
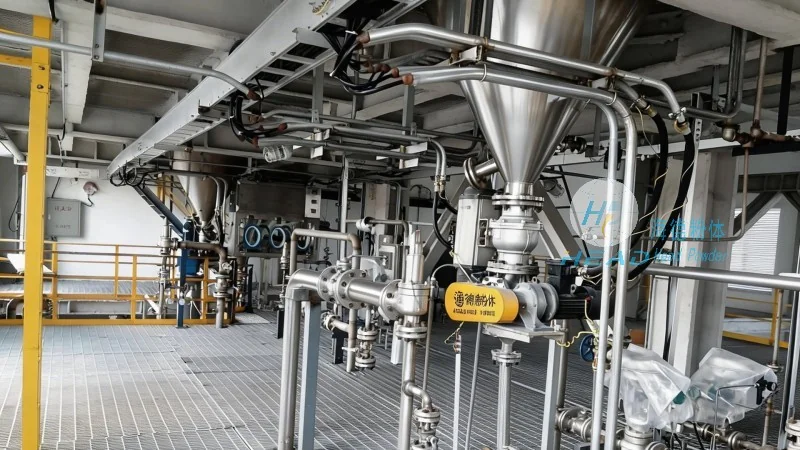
Pressure systems utilize compressed air or gas to push material through the conveying line. They are typically employed for short to medium distances and are ideal for applications where the material is to be transported from a storage silo to a processing or packaging unit. The system operates by introducing high-pressure air into the material, which is then carried along the pipeline. This method is particularly effective for handling free-flowing fertilizers with low to moderate moisture content, as it minimizes material degradation and ensures consistent flow rates.
Vacuum systems, on the other hand, use a vacuum to draw material from a source into the conveying line. These systems are commonly used for longer distances and are suitable for applications requiring material to be transported from multiple points to a central processing facility. The vacuum is created by a fan or blower at the receiving end, which pulls the material through the pipeline. Vacuum systems are advantageous for handling materials with higher moisture content or those that are more prone to caking, as the lower air velocity reduces the risk of material degradation and blockages.
The practical applications of pneumatic conveying systems in the fertilizer industry are diverse and critical to the smooth operation of fertilizer production and distribution processes. These systems are widely used in various stages of the fertilizer lifecycle, from raw material handling to final product packaging.
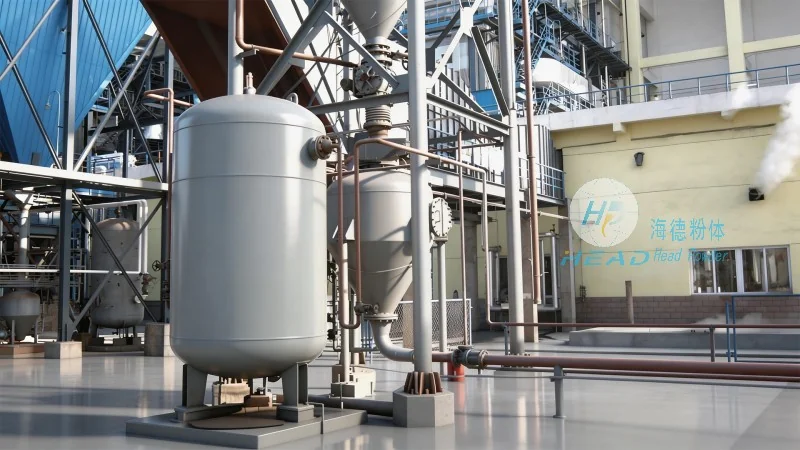
At the initial stage of fertilizer production, raw materials such as phosphate rock, nitrogen compounds, and potassium salts are often received in bulk and stored in silos. Pneumatic conveying systems are used to transfer these raw materials from the storage silos to the processing units, ensuring a continuous and efficient supply of raw materials. The systems can handle large volumes of material with minimal downtime, which is essential for maintaining production schedules.
During the manufacturing process, intermediate products such as granules or powders are often transferred between different processing stages. Pneumatic conveying systems facilitate this transfer by moving materials from one processing unit to another without the need for manual handling or intermediate storage. This integration improves the overall efficiency of the production line and reduces the risk of contamination or material loss.
After the fertilizer is fully processed, it needs to be packaged and transported to distribution centers or end-users. Pneumatic conveying systems are used to move the final product from the packaging line to storage silos or loading facilities. This stage is critical for ensuring that the product reaches its destination in optimal condition, with minimal handling and risk of spillage or contamination.
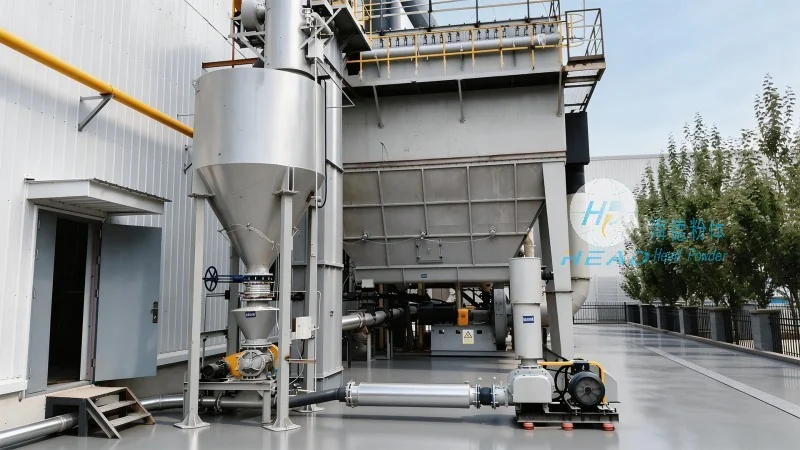
Implementing pneumatic conveying systems in fertilizer transport offers several operational advantages, including improved safety, reduced labor costs, and enhanced material handling efficiency. However, there are also considerations that need to be addressed to ensure optimal performance. These include the selection of appropriate air velocities to prevent material degradation, the use of corrosion-resistant materials to handle acidic or alkaline fertilizers, and the implementation of proper maintenance schedules to minimize system downtime.
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, provides comprehensive solutions for the design, installation, and maintenance of pneumatic conveying systems tailored to the specific needs of the fertilizer industry. By leveraging advanced technology and industry expertise, HeadPowder helps fertilizer producers and distributors enhance their operational efficiency, reduce costs, and ensure the safe and reliable transport of bulk fertilizers. The practical applications and operational advantages of pneumatic conveying systems make them a preferred choice for modern fertilizer handling and transportation, contributing to the overall sustainability and productivity of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top