Phosphate fertilizer is a fundamental component in modern agricultural practices, supplying essential nutrients for plant growth. The efficient and reliable transportation of phosphate powder from production sites to processing or application areas is critical for maintaining operational efficiency and product quality. This article introduces the phosphate powder pneumatic conveying equipment, detailing its structure and working principles, as provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
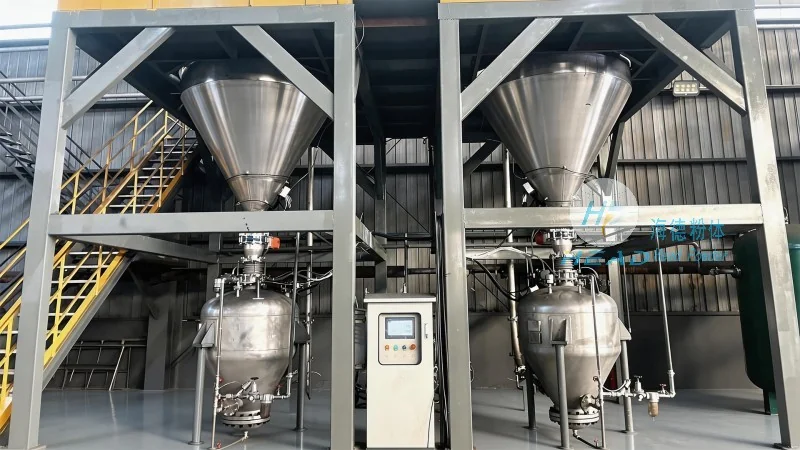
Phosphate powder pneumatic conveying equipment is a specialized system engineered to transport fine phosphate powders through a pressurized or vacuum air stream. Unlike traditional mechanical conveying methods such as screw or belt conveyors, pneumatic systems offer advantages including flexibility, minimal product contamination, and the ability to handle materials with high moisture content or abrasive properties. The equipment is widely utilized in the phosphate fertilizer industry to ensure safe and efficient material handling from storage silos to processing lines.
The phosphate powder pneumatic conveying system comprises several critical components that function together to achieve effective material transport. These components include the material hopper, which stores the phosphate powder; the air compressor or vacuum pump, which generates the necessary pressure or vacuum; the conveying line, typically constructed from stainless steel or other corrosion-resistant materials to prevent material degradation; and the control system, which regulates flow rate and pressure to maintain optimal operation. The system may also incorporate features such as cyclone separators to separate powder from the air stream and dust collectors to ensure environmental compliance.
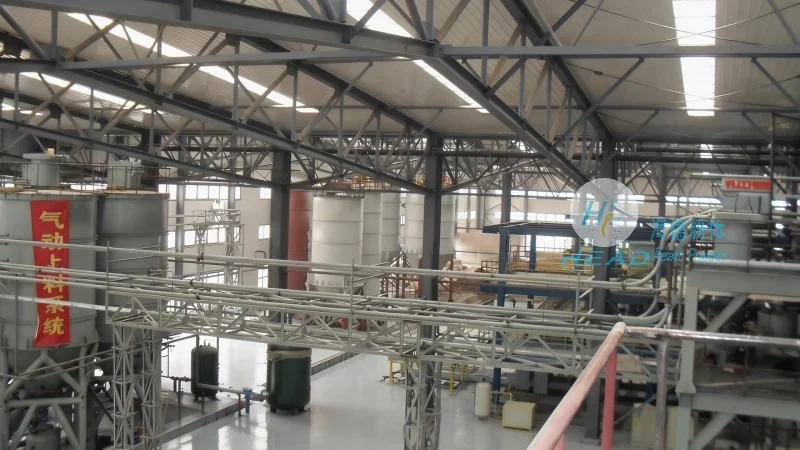
The operation of the phosphate powder pneumatic conveying equipment is based on the principle of air movement to transport solid particles. In a typical positive pressure system, the air compressor generates compressed air, which is then mixed with the phosphate powder in the material hopper. The air-powder mixture is then forced through the conveying line to the destination point, such as a processing plant or storage silo. At the receiving end, a cyclone separator or filter separates the powder from the air, allowing the powder to be collected and the air to be discharged or recirculated. In a negative pressure system, a vacuum pump creates a vacuum that draws the powder from the source into the conveying line. Both systems rely on the velocity of the air stream to suspend and transport the powder particles, ensuring efficient and consistent material movement.
Implementing pneumatic conveying equipment for phosphate powder offers several benefits that enhance operational efficiency and product quality. One primary advantage is the ability to handle fine powders without the risk of blockages or material degradation that can occur with mechanical conveyors. The system also minimizes product contamination, as the conveying line is isolated from external environments, preventing cross-contamination with other materials. Furthermore, pneumatic systems are highly flexible, allowing for changes in material flow rates and destinations without significant modifications to the equipment. This adaptability is particularly valuable in dynamic production environments where material volumes or processing requirements may vary.
Phosphate powder pneumatic conveying equipment is widely applied in various stages of the phosphate fertilizer production process. In the initial stages, the equipment is used to transport raw phosphate ore from storage silos to grinding mills for size reduction. After grinding, the fine phosphate powder is conveyed to the mixing and granulation units, where it is combined with other nutrients and binders. The system also plays a crucial role in transporting finished phosphate fertilizer products from the production line to storage facilities or packaging areas. By ensuring consistent and reliable material transport, the equipment contributes to maintaining high production throughput and product consistency.
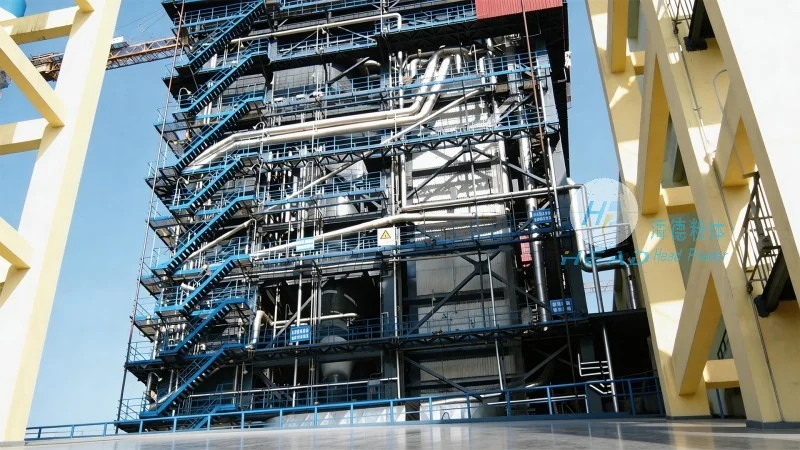
Proper maintenance and operational management are essential for maximizing the performance and lifespan of phosphate powder pneumatic conveying equipment. Regular inspection of the conveying line for blockages or wear is necessary to prevent system failures. The air compressor or vacuum pump should be maintained according to manufacturer specifications to ensure consistent pressure or vacuum levels. Additionally, the cyclone separators and dust collectors should be cleaned regularly to prevent clogging and maintain efficiency. Proper training of operators on the system's controls and safety procedures is also critical to ensure safe and effective operation. By adhering to these maintenance and operational guidelines, users can ensure the reliable and efficient performance of the equipment.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying equipment for the powder handling industry. With a focus on innovation and quality, the company has developed advanced solutions tailored to the specific needs of the phosphate fertilizer sector. HeadPowder's products are designed to meet the highest standards of performance, reliability, and durability, ensuring long-term operational efficiency for its clients. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, providing comprehensive support from equipment design and installation to maintenance and after-sales service.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top