Guar gum powder is a versatile thickening agent and stabilizer widely utilized across industries such as food, pharmaceuticals, and cosmetics. The efficient and safe transportation of this hygroscopic powder from storage to processing units is essential for maintaining product integrity and operational efficiency. Pneumatic conveying systems have become a preferred solution due to their ability to transport materials in a closed environment, minimizing dust exposure and contamination risks.
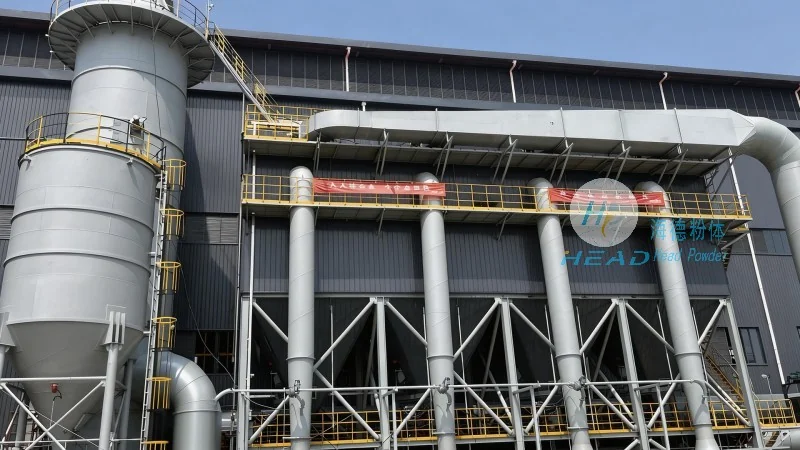
Pneumatic conveying, or air-assisted powder transport, leverages compressed air to move dry powders through a pipeline. This method is particularly suited for guar gum powder because of its sensitivity to moisture and the need for hygienic handling. The core components of a pneumatic conveying system for guar gum powder include a hopper, a rotary valve, a conveyor line, a filter, and a dust collector. Each component is integral to ensuring the system operates smoothly and reliably.
The hopper serves as the primary storage container for the guar gum powder, providing a consistent feed to the system. It is typically designed with a sloped bottom to facilitate the flow of powder into the rotary valve, preventing material bridging or clogging. The rotary valve acts as a controlled gate, regulating the flow rate of the powder into the conveyor line. This component prevents backflow and ensures a steady supply of material, which is critical for maintaining system performance. The conveyor line, usually constructed from stainless steel or other corrosion-resistant materials, forms the main pathway for the powder and air mixture. It is equipped with bends and elbows to navigate the system layout while preserving the integrity of the powder. The filter and dust collector are essential for maintaining air quality and complying with environmental regulations. As the air-powder mixture passes through the filter, the powder is separated from the air, which is then either vented or recirculated. The dust collector ensures that any residual dust is captured, creating a clean working environment.
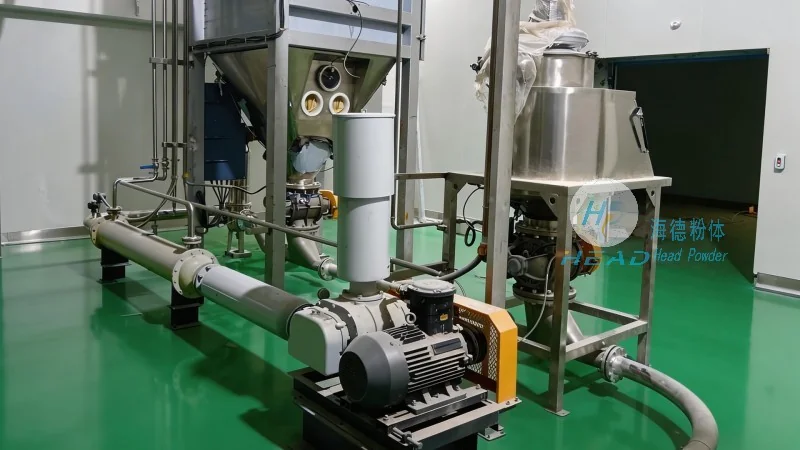
The operation of a pneumatic conveying system for guar gum powder involves several sequential steps. First, the guar gum powder is fed from the hopper into the rotary valve. The rotary valve then opens to allow the powder to enter the conveyor line. Simultaneously, compressed air is introduced into the line, creating a pressure differential that propels the powder forward. The air and powder mixture travels through the pipeline, passing through bends and elbows as required by the system layout. At the receiving end, the mixture is separated in the filter, where the powder is collected and discharged into the target container. The air, now filtered, is either released into the environment or recirculated back into the system to maintain efficiency.
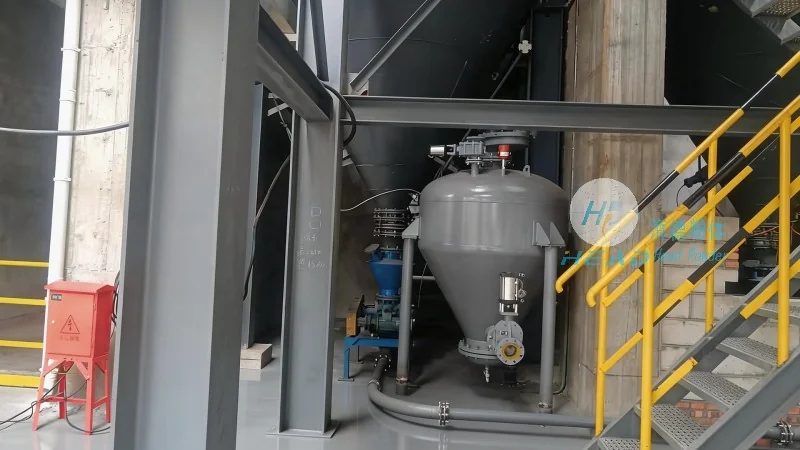
Pneumatic conveying systems offer several key advantages when handling guar gum powder. Firstly, the closed system design minimizes dust exposure and prevents contamination from external sources, which is crucial for food-grade applications where product purity is paramount. Secondly, the system can handle varying flow rates, making it adaptable to different production needs, from small-scale batches to large industrial operations. Additionally, the equipment is relatively compact and can be integrated into existing production lines without major modifications. The closed system also reduces the risk of product degradation due to exposure to air or moisture, ensuring the quality of the guar gum powder is maintained throughout the conveying process. These benefits make pneumatic conveying an ideal choice for industries relying on guar gum powder.
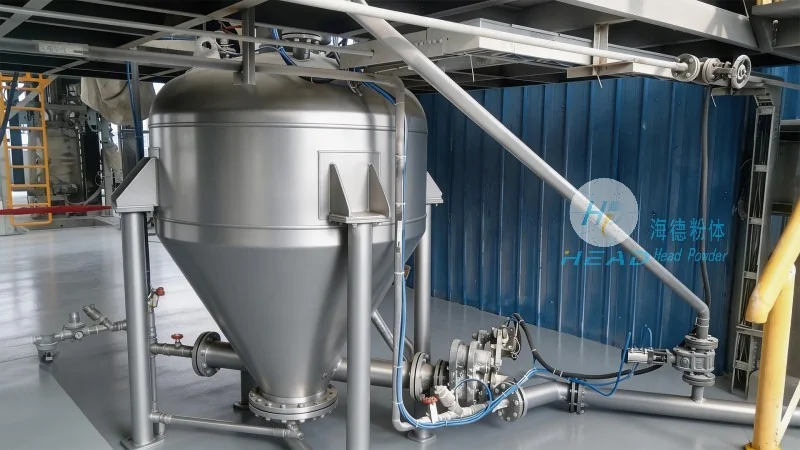
The use of pneumatic conveying systems for guar gum powder is prevalent in multiple sectors. In the food industry, guar gum is used as a thickening agent in dairy products, sauces, and bakery items. The pneumatic system ensures that the powder is transported safely and efficiently from storage to production lines, maintaining the quality of the final products. In the pharmaceutical industry, guar gum is used as a binder and filler in tablets and capsules. The closed and hygienic nature of the pneumatic system is critical for meeting the stringent quality and safety standards of pharmaceutical manufacturing. Similarly, in the cosmetics industry, guar gum is used in creams and lotions as a thickening agent. The system helps in transporting the powder without compromising its purity, which is essential for consumer safety and product efficacy. These applications highlight the importance of reliable powder handling in ensuring product quality and regulatory compliance.
In conclusion, pneumatic conveying equipment is a vital component in the efficient and safe handling of guar gum powder. The system's design, incorporating key components such as the hopper, rotary valve, conveyor line, filter, and dust collector, ensures reliable and hygienic transport. The advantages of using pneumatic conveying, including dust control, adaptability, and product quality maintenance, make it an ideal choice for industries relying on guar gum powder. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems tailored to meet the specific needs of various applications, ensuring optimal performance and compliance with industry standards. The company's expertise in powder handling technology helps clients achieve efficient, safe, and cost-effective operations in their production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top