Understanding the structure and principle of powder pneumatic conveying systems is crucial for industries that handle bulk powders efficiently. These systems are designed to transport dry materials like powders, granules, and fine particles through a pipeline using air or gas as the conveying medium. The technology offers a flexible and efficient solution for material handling, especially in applications where traditional methods like belt conveyors or bucket elevators may not be suitable.
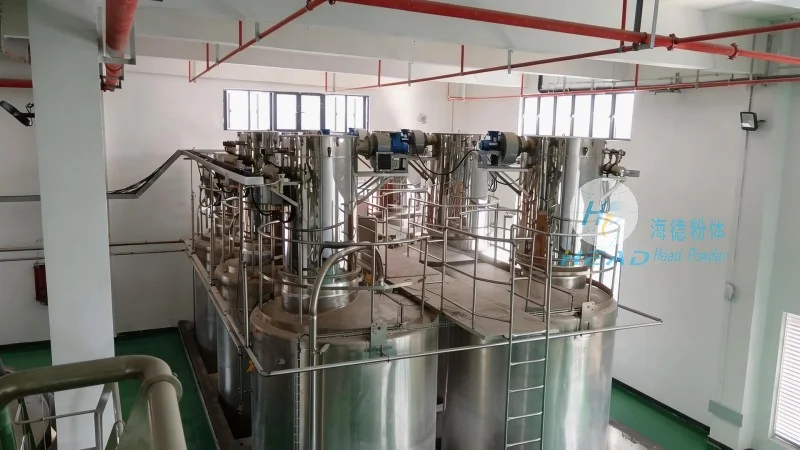
A typical powder pneumatic conveying system consists of several key components that work together to ensure smooth material transport. The main parts include the material feed hopper, the conveying pipeline, the air supply system (blowers or compressors), and the discharge equipment. The feed hopper is responsible for storing and feeding the powder into the system, while the pipeline transports the material from the feed point to the discharge point. The air supply system generates the necessary airflow to move the powder particles through the pipeline. The discharge equipment, such as a receiver or a silo, collects the material at the end of the conveying line.
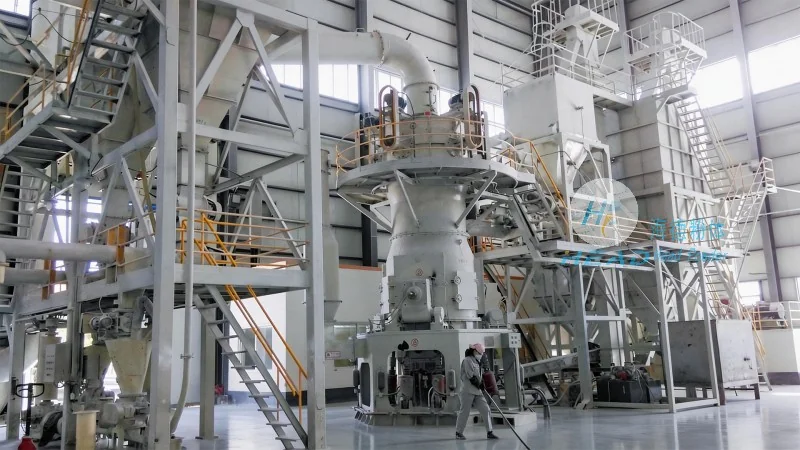
The operation of a powder pneumatic conveying system is based on the principle of fluidization and drag. In the positive pressure system, the air is introduced at a higher pressure than the ambient air, pushing the powder particles through the pipeline. The material is suspended in the air stream, and the velocity of the air ensures that the particles remain in suspension and are transported to the destination. In the negative pressure (or vacuum) system, the air is drawn from the pipeline, creating a vacuum that pulls the powder particles into the system. Both systems rely on the interaction between the air flow and the powder particles to achieve efficient conveying.
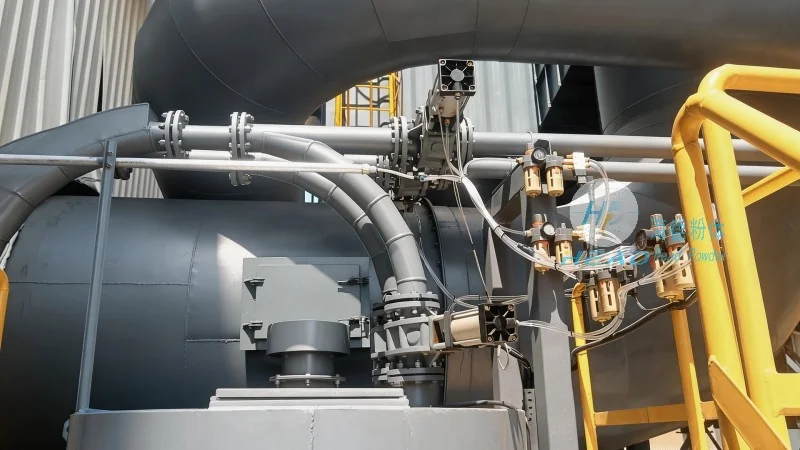
HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and manufacturing high-quality powder pneumatic conveying systems. The company's equipment is engineered to meet the diverse needs of various industries, including food processing, pharmaceuticals, chemicals, and minerals. The systems are known for their reliability, low maintenance requirements, and ability to handle a wide range of powder types. Additionally, the equipment can be customized to fit specific operational requirements, such as conveying distance, material flow rate, and environmental conditions.
Powder pneumatic conveying systems are widely used across multiple sectors due to their versatility. In the food industry, these systems are used to transport ingredients like flour, sugar, and spices from storage to processing lines. In the pharmaceutical industry, they are employed to handle sensitive powders, ensuring contamination-free transport. The chemical industry utilizes them for conveying raw materials and finished products, while the minerals sector uses them for transporting ores and other bulk materials. The adaptability of the systems makes them a preferred choice for many applications where material handling efficiency and safety are paramount.
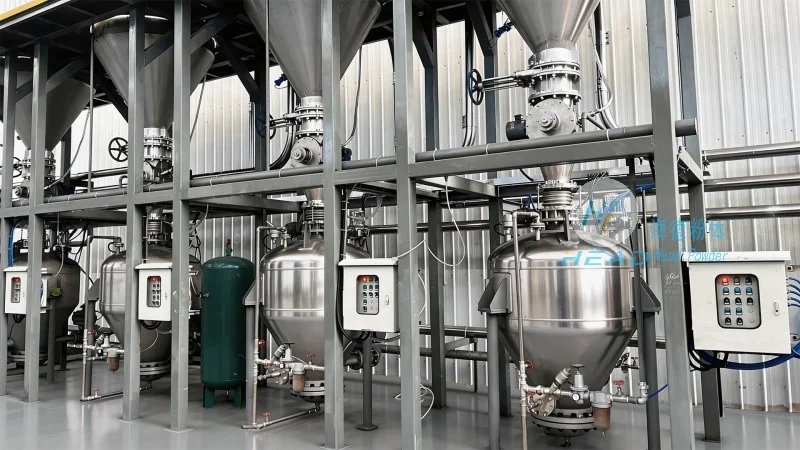
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is committed to providing innovative and reliable powder pneumatic conveying solutions. The company's expertise in designing and manufacturing these systems ensures that clients receive equipment that meets their specific needs and operational standards. By leveraging advanced technology and rigorous quality control, HeadPowder delivers systems that enhance productivity, reduce downtime, and improve overall material handling efficiency. For industries seeking efficient and effective powder transport solutions, HeadPowder's equipment represents a reliable investment in modern material handling technology.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top