Starch pneumatic conveying equipment is a specialized system designed for the efficient transport of starch and other fine powders. As a key component in powder handling, this technology offers a reliable solution for moving bulk materials from one location to another within industrial settings. The equipment operates on the principle of air flow, utilizing pressure or vacuum to move the material through a pipeline network. This method is particularly advantageous for handling materials that are prone to dust, caking, or contamination, making it ideal for applications in the food, pharmaceutical, and chemical industries.
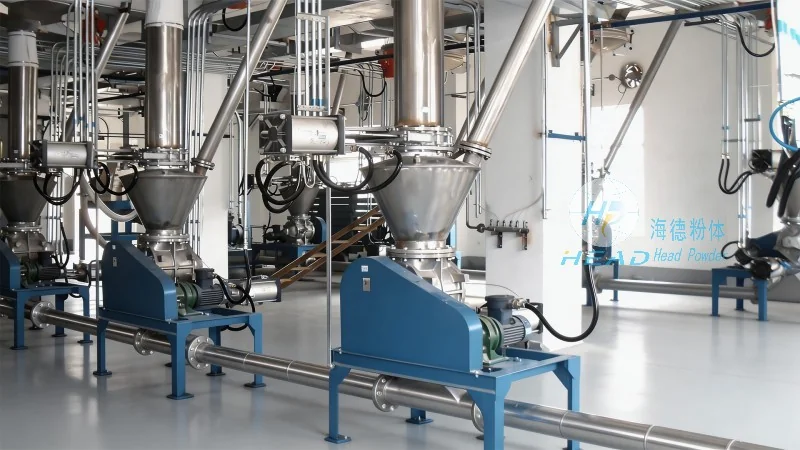
The starch pneumatic conveying system typically consists of several core components that work in concert to ensure smooth material transport. The main elements include a material feeder, a conveying line (often equipped with bends and expansion joints), a dust separator or cyclone, and a receiver or discharge hopper. The material feeder is responsible for introducing the starch into the system, ensuring a consistent flow rate. The conveying line, which may be made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and friction of the material and air mixture. The dust separator plays a crucial role in separating the air from the starch particles, preventing dust accumulation and ensuring the material is delivered in a clean state. The receiver or discharge hopper collects the starch at the destination point, completing the transport process.
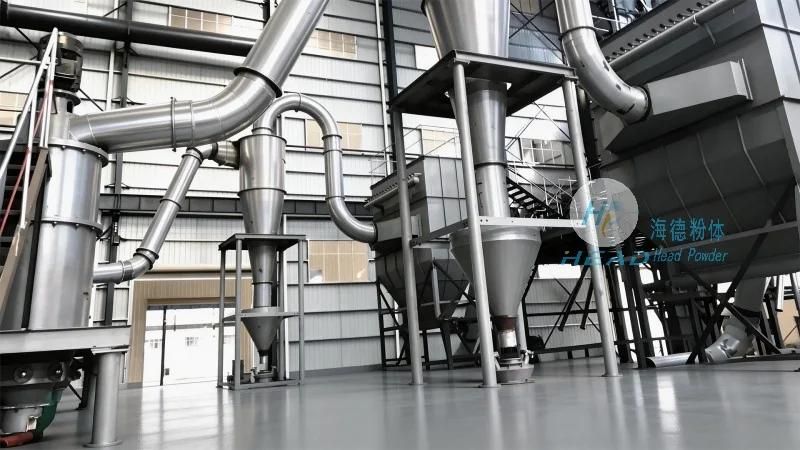
The operation of the starch pneumatic conveying equipment is based on the fundamental principle of fluidization and air movement. In a typical setup, the system can operate under either positive pressure or negative pressure (or a combination of both, known as a hybrid system). Under positive pressure, compressed air is introduced into the conveying line, pushing the starch particles forward. The air velocity is carefully controlled to maintain the material in a suspended state, preventing it from settling or caking. Under negative pressure, the system creates a vacuum that draws the starch particles into the line, moving them from the source to the destination. The choice between positive and negative pressure depends on the specific application, material characteristics, and system layout. For starch, which is a fine powder with low bulk density, positive pressure systems are often preferred as they provide better control over the material flow and reduce the risk of blockages.
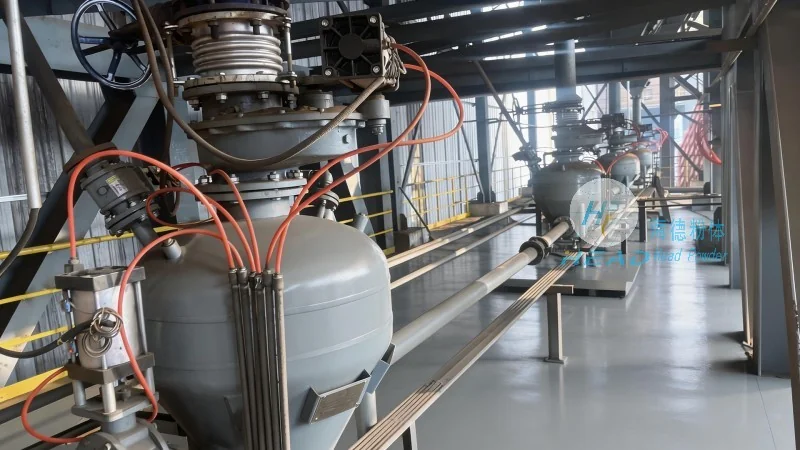
Implementing a starch pneumatic conveying system offers numerous benefits for industrial operations. One of the primary advantages is the ability to handle fine powders without the need for mechanical components that could cause wear or contamination. The enclosed system prevents dust from escaping into the environment, ensuring compliance with environmental regulations and maintaining a clean working environment. Additionally, the system is highly flexible, allowing for changes in the conveying route or destination without major modifications. It also reduces labor costs by automating the material transport process, minimizing the need for manual handling and associated risks. The efficiency of the system in terms of energy consumption and material throughput is another key advantage, as it can transport large quantities of starch over long distances with minimal operational overhead.
Starch pneumatic conveying equipment is widely used in various applications within the starch processing industry. For instance, in the production of modified starches, the equipment is used to transport raw starch from storage silos to processing units, ensuring a continuous supply of material. In the food industry, it is employed to move starch from the milling and screening stages to packaging or further processing steps. The pharmaceutical industry also utilizes this technology for the transport of starch used in tablet manufacturing, where maintaining product purity and preventing contamination is critical. Each application benefits from the system's ability to handle fine powders with precision and maintain product quality throughout the transport process.
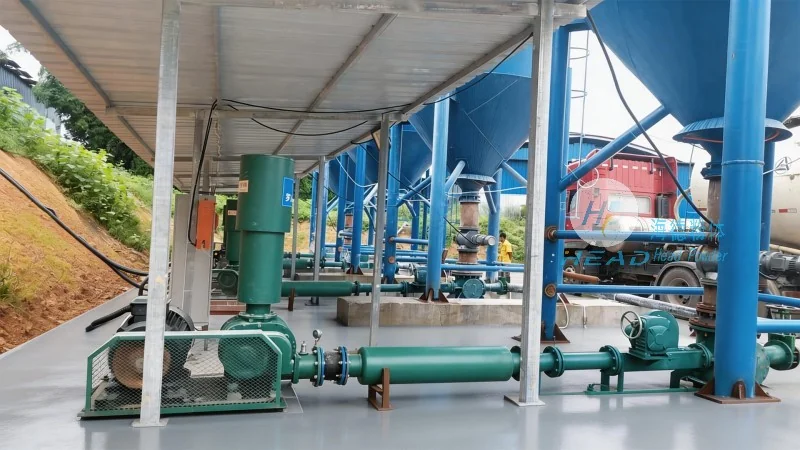
When selecting a starch pneumatic conveying system, several factors must be considered to ensure optimal performance and longevity. The first consideration is the material characteristics of the starch, including its particle size, moisture content, and flowability. These properties influence the choice of system type (positive or negative pressure) and the design of components such as the feeder and dust separator. The system's capacity and the distance to be covered are also critical factors, as they determine the required air volume and pressure. Additionally, the system's material of construction is important, as it must be resistant to the corrosive or abrasive nature of the starch and any additives used in processing. Regular maintenance is essential to keep the equipment operating efficiently. This includes cleaning the conveying line and dust separator to prevent clogging, inspecting the feeder for wear, and checking the air compressor or vacuum pump for proper performance. Proper maintenance not only extends the equipment's lifespan but also ensures consistent material quality and system reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top