Types, Characteristics, and Application Ranges of Malt Pneumatic Conveying Systems
Release time:2026-09-14 10:47:18
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for malt processing industries. This article explores the various types of malt pneumatic conveying systems, their key characteristics, and the diverse applications where these systems excel in ensuring efficient and reliable material transport.
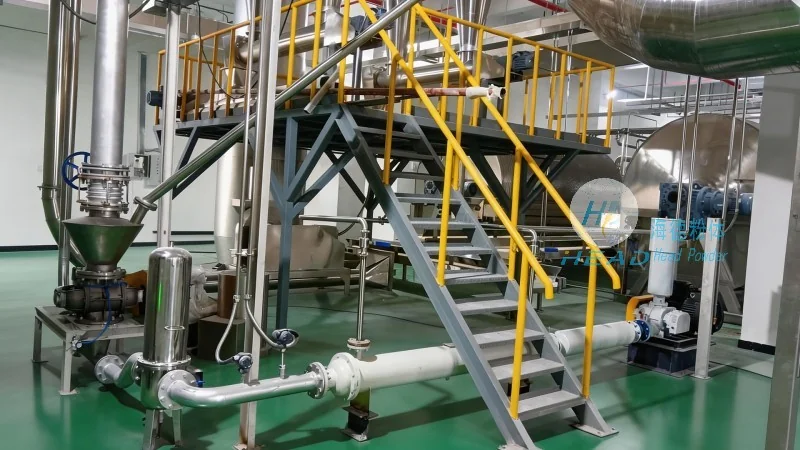
Overview of Malt Pneumatic Conveying Systems
Malt pneumatic conveying systems utilize air or other gases to transport malt grains and other bulk materials from one location to another within a processing facility. These systems are engineered to handle the unique properties of malt, such as its moisture content, density, and susceptibility to breakage, while maintaining high levels of efficiency and product integrity. The primary goal of these systems is to provide a cost-effective, hygienic, and flexible solution for moving malt between storage, processing, and packaging stages.
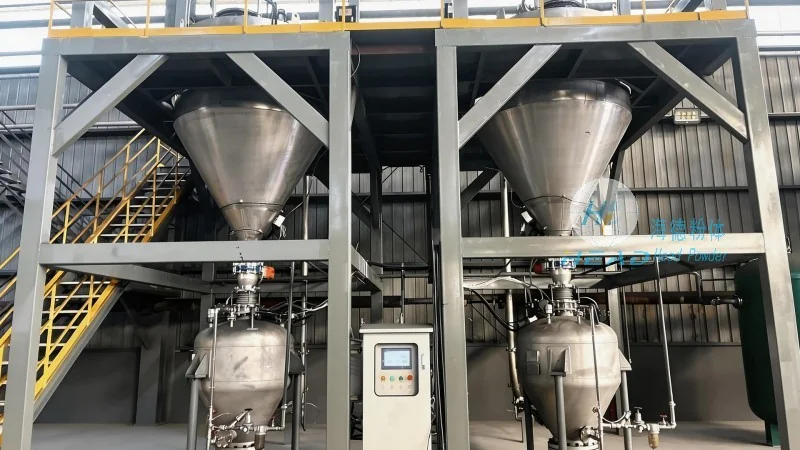
Types of Malt Pneumatic Conveying Systems
There are several distinct types of malt pneumatic conveying systems, each designed to suit different operational requirements and material handling scenarios. The most common types include:
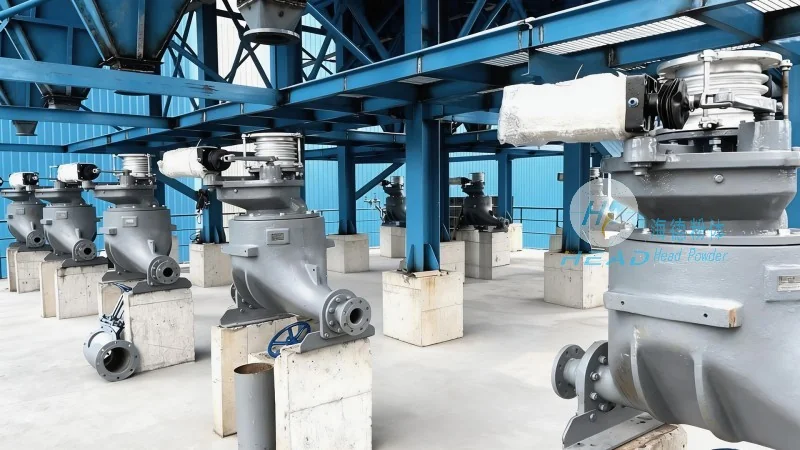
- Positive Pressure Systems: These systems generate air pressure that pushes the material through a pipeline. They are ideal for applications requiring high material flow rates and are commonly used in large-scale malt production facilities. Positive pressure systems offer advantages like reduced material degradation and the ability to handle abrasive materials.
- Negative Pressure (Vacuum) Systems: In contrast, negative pressure systems create a vacuum that draws material into the pipeline. They are well-suited for applications where material is to be collected from multiple points or where the material is sensitive to pressure changes. Negative pressure systems are often preferred in environments where dust control and product cleanliness are critical.
- Combination (Two-Stage) Systems: These systems integrate both positive and negative pressure stages to optimize material transport. The first stage may use a positive pressure system to move material from a central point, while the second stage employs a negative pressure system to deliver material to specific destinations. This approach allows for greater flexibility and efficiency in complex processing layouts.
- Pressure-Swing Systems: A specialized type of pneumatic conveying system that alternates between positive and negative pressure phases. This method is particularly effective for handling materials with varying properties or for applications requiring precise control over material flow. Pressure-swing systems are often used in high-purity applications where product contamination must be minimized.
Key Characteristics of Malt Pneumatic Conveying Systems
Each type of malt pneumatic conveying system possesses unique characteristics that influence its suitability for specific applications. Understanding these features is crucial for selecting the right system for a given operation. Key characteristics include:
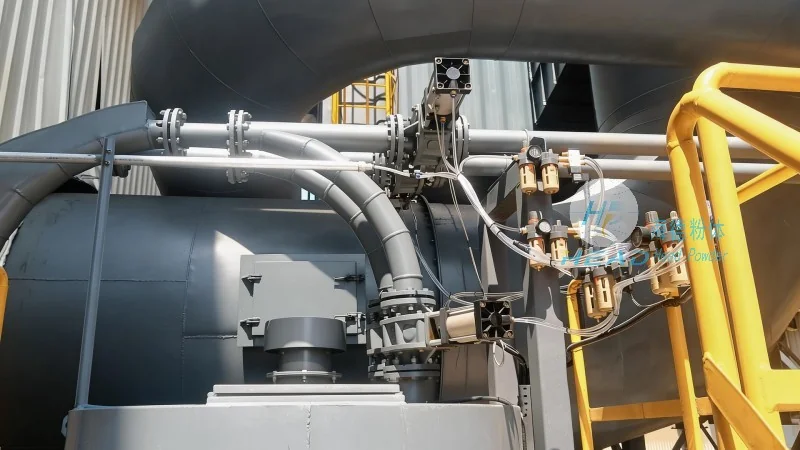
- Material Handling Capacity: The ability of the system to transport a specified volume of malt per unit time. This is influenced by factors such as air velocity, pipeline diameter, and system pressure. Higher capacity systems are typically used in large-scale production environments.
- Energy Efficiency: The efficiency of converting electrical energy into effective material transport. Modern systems incorporate advanced control technologies and aerodynamic designs to minimize energy consumption while maintaining performance. Energy efficiency is a critical factor for long-term operational cost management.
- Product Integrity: The system's ability to preserve the quality of the malt during transport. This includes minimizing particle breakage, preventing moisture loss, and avoiding contamination. Systems with gentle handling mechanisms, such as low air velocity or flexible pipelines, are preferred for maintaining product quality.
- Hygiene and Cleanliness: The ease of cleaning and maintaining the system to meet sanitary standards. Malt processing environments require systems that can be easily disassembled, cleaned, and sanitized to prevent microbial growth and ensure food safety compliance. Stainless steel construction and CIP (Clean-In-Place) capabilities are common features in high-hygiene applications.
- Flexibility and Scalability: The ability to adapt to changing production needs and expand the system's capacity as required. Modular designs and adjustable components allow for easy modifications without extensive downtime. Scalability is essential for businesses planning to grow or diversify their malt processing operations.
Application Ranges of Malt Pneumatic Conveying Systems
Malt pneumatic conveying systems find wide-ranging applications across the malt processing industry. Their versatility and efficiency make them suitable for various stages of malt production and handling. Common applications include:

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
