Understanding the various types, features, and application ranges of fertilizer pneumatic conveying systems is crucial for optimizing material handling in agricultural and industrial settings. These systems utilize air pressure to transport bulk materials like fertilizers, offering efficient and flexible solutions for different operational needs.
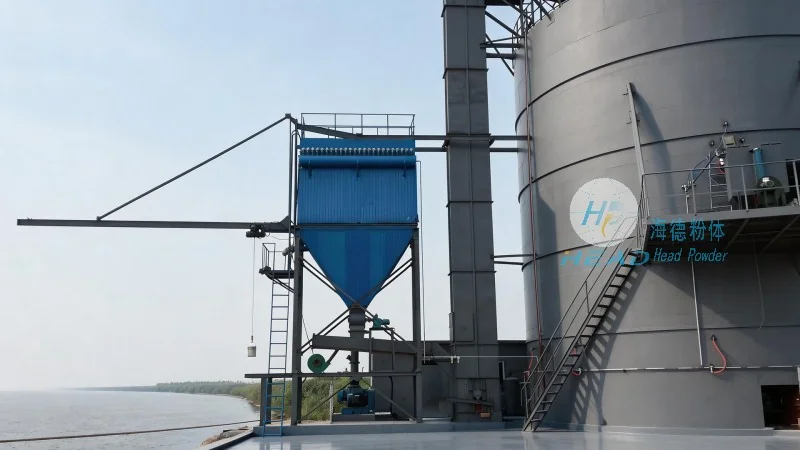
There are primarily two main categories of pneumatic conveying systems used for fertilizers: dilute-phase and dense-phase. Dilute-phase systems operate by moving material in a low concentration of particles suspended in air, typically at high velocities. This method is suitable for short to medium distances and is commonly used in applications where material is transported from storage silos to processing units. Dense-phase systems, on the other hand, transport material in a higher concentration, often using lower air velocities and sometimes with the assistance of positive pressure or vacuum to ensure stable flow. These systems are ideal for longer distances and for handling materials that are more abrasive or sensitive to high-velocity air.
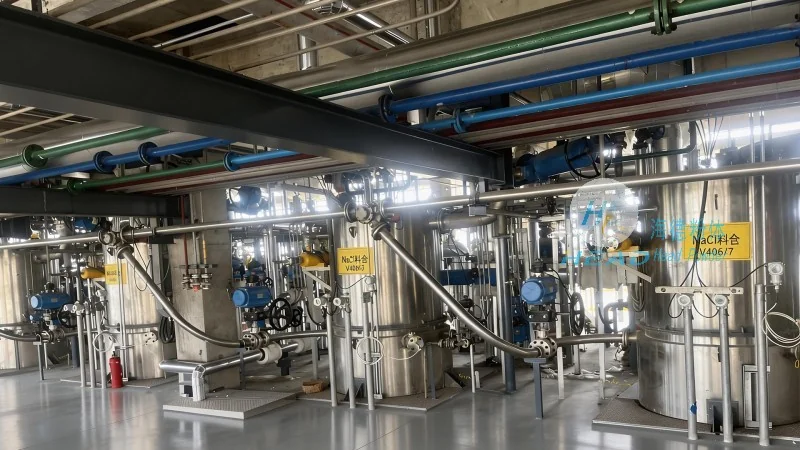
One of the most significant advantages of pneumatic conveying for fertilizers is its ability to handle a wide variety of materials, including granular, powdered, and even some liquid-based fertilizers. The systems are designed to minimize material degradation, ensuring that the nutrient content and quality of the fertilizer remain intact during transport. Additionally, these systems offer high throughput rates, allowing for efficient handling of large volumes of material, which is essential in agricultural and industrial production. Another key feature is the flexibility in system design, as they can be adapted to different plant layouts and operational requirements. The systems also provide a closed-loop operation, which helps in controlling dust emissions and maintaining a clean working environment, aligning with environmental regulations.
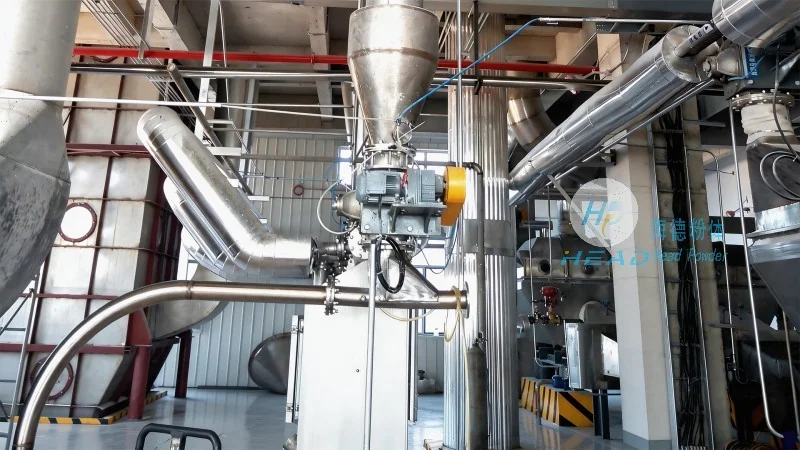
Fertilizer pneumatic conveying systems are widely used across various industries, particularly in the agricultural sector for transporting bulk fertilizers from production facilities to farms or storage depots. They are also utilized in chemical and petrochemical industries where similar bulk materials are processed. The application ranges vary from small-scale operations in local farms to large-scale industrial plants handling thousands of tons of material annually. The systems are suitable for both indoor and outdoor applications, depending on the specific requirements of the facility. For example, in indoor settings, they can be integrated into existing production lines, while outdoor installations may be used for material transfer between storage silos and processing units.
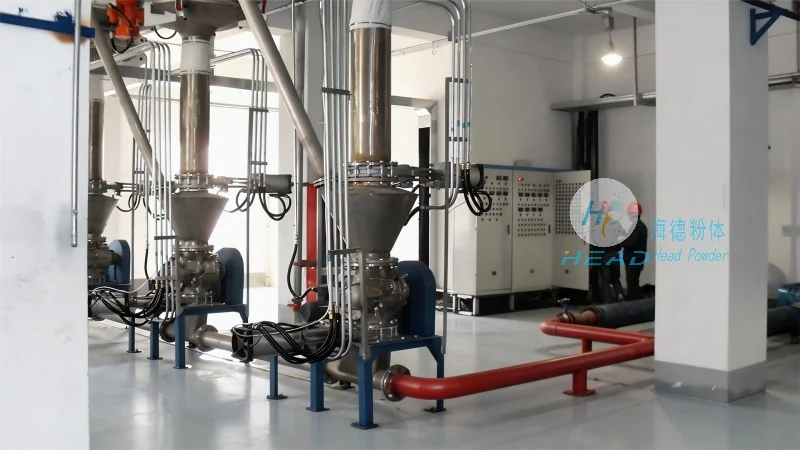
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and installation of advanced pneumatic conveying systems for bulk materials, including fertilizers. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the agricultural and industrial sectors. HeadPowder's expertise lies in providing customized solutions tailored to the specific needs of clients, ensuring efficient and reliable material handling. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-performance systems that meet international standards. By combining advanced technology with practical engineering, HeadPowder aims to enhance operational efficiency and sustainability in material handling processes for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top