In the coal and limestone powder processing industry, pneumatic conveying systems are widely used to transport bulk materials efficiently. Two primary methods dominate this field: positive pressure conveying and negative pressure conveying. Each method has distinct characteristics, advantages, and applications, making the choice between them critical for optimizing material handling operations. This analysis from Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions based in Shandong, China, explores the differences between these two approaches to help industry professionals make informed decisions.
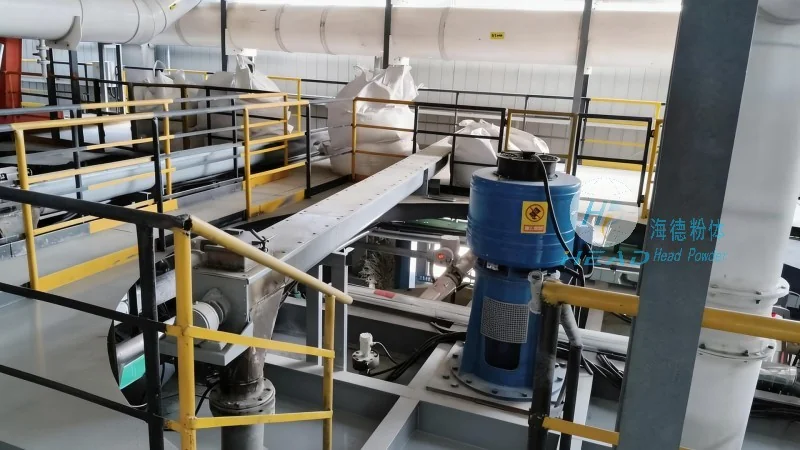
Positive pressure conveying, also known as pressure pneumatic conveying, operates by forcing air and material through a pipeline using a positive displacement or centrifugal blower. The system maintains a positive pressure within the pipeline, which ensures that material is continuously pushed forward. This method is particularly effective for long-distance and high-capacity material transport, as it can handle larger volumes of coal and limestone powder with fewer transfer points. The positive pressure system typically includes a hopper, a rotary valve, a blower, and a pipeline network. The blower generates the necessary pressure to move the material, and the system is designed to prevent backflow and maintain consistent flow rates.
One of the main advantages of positive pressure conveying is its ability to transport materials over long distances without the need for intermediate storage or transfer points. This reduces operational complexity and improves overall efficiency. Additionally, positive pressure systems are generally more straightforward to install and maintain compared to their negative pressure counterparts. They are also well-suited for handling abrasive or corrosive materials, such as coal and limestone powder, as the high-pressure air helps to break up agglomerates and ensure consistent flow. The system's design minimizes the risk of material buildup in the pipeline, which can lead to blockages and downtime.
Despite its benefits, positive pressure conveying has several limitations. The most significant drawback is the potential for dust leakage at the discharge point and along the pipeline. Since the system operates under positive pressure, any seal failure can result in dust escaping into the environment, posing health and safety risks. This requires robust sealing mechanisms and regular maintenance to ensure compliance with environmental regulations. Another challenge is the higher energy consumption compared to negative pressure systems, as the blower must work harder to maintain the pressure. Furthermore, positive pressure systems may not be suitable for transporting materials that are highly sensitive to air exposure, as the constant air flow can cause degradation or moisture loss.
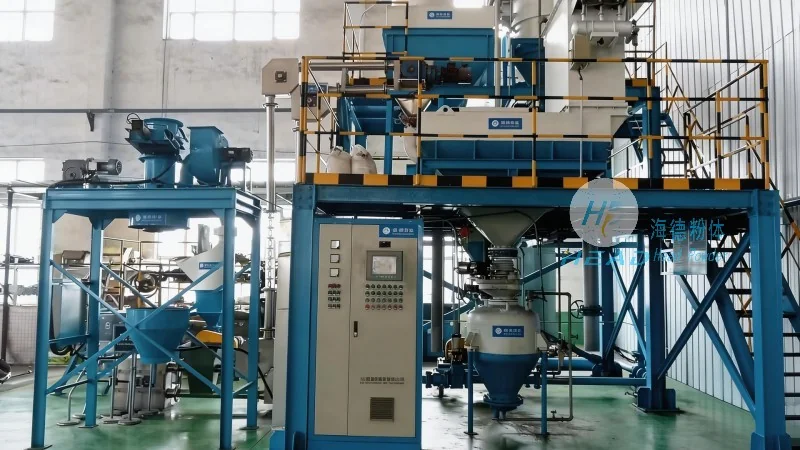
Negative pressure conveying, or suction pneumatic conveying, operates by creating a vacuum in the pipeline using a suction fan. The system draws material from a hopper or storage bin into the pipeline, where it is carried by the suction force. This method is typically used for shorter distances and lower capacities, as the suction force is limited by the fan's capacity and the length of the pipeline. Negative pressure systems are often preferred for applications where dust control is a priority, such as in environments where dust exposure could be hazardous or where material is sensitive to air contact.
The primary advantage of negative pressure conveying is its superior dust control. Since the system operates under a vacuum, any leaks or failures result in air being drawn into the system rather than dust escaping. This makes it ideal for handling materials that are fine, dusty, or potentially hazardous, such as limestone powder. Negative pressure systems also tend to consume less energy compared to positive pressure systems, as the suction fan operates at lower pressures. Additionally, they are more flexible in terms of layout, as the pipeline can be arranged in a more compact manner without the need for constant positive pressure maintenance.
However, negative pressure conveying has its own set of challenges. The most significant limitation is the shorter effective transport distance, typically ranging from a few meters to a few hundred meters, depending on the material and system design. This can require more transfer points or intermediate storage, increasing operational complexity. Another drawback is the higher risk of blockages, as the suction force may not be strong enough to move large agglomerates or wet materials. This necessitates additional equipment, such as rotary valves or vibrators, to prevent clogging. Furthermore, negative pressure systems are more prone to system backflow if the fan is shut down abruptly, which can lead to material spillage and contamination.
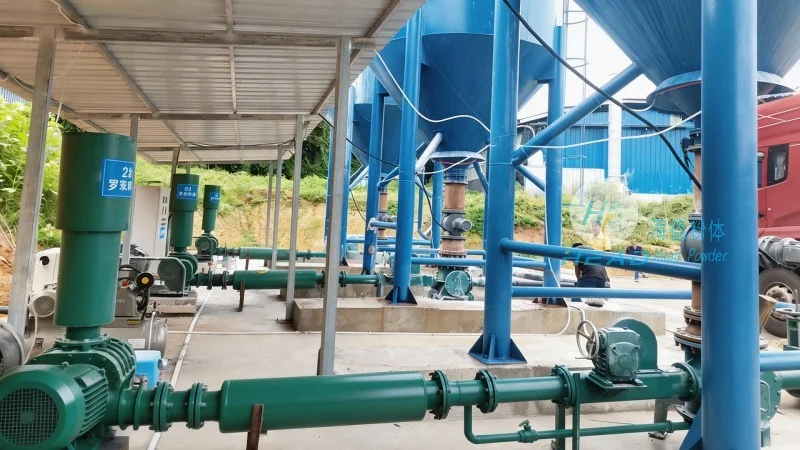
When deciding between positive and negative pressure conveying for coal and limestone powder, several factors must be considered. The most critical factor is the required transport distance. For long-distance applications exceeding 100 meters, positive pressure conveying is generally more efficient and cost-effective. For shorter distances, such as within a processing plant or between adjacent facilities, negative pressure conveying may be more suitable. Another key consideration is the material characteristics. If the material is abrasive or prone to agglomeration, positive pressure conveying may be preferred due to its ability to handle larger particles and maintain consistent flow. Conversely, if the material is fine, dusty, or sensitive to air exposure, negative pressure conveying offers better dust control and material integrity.
Environmental regulations and safety considerations play a significant role in the choice of conveying method. Positive pressure systems require stringent sealing to prevent dust emissions, which can impact air quality and compliance with local regulations. Negative pressure systems, while better at containing dust, may still require additional filtration to meet environmental standards. From a safety perspective, both methods pose risks, but negative pressure systems are generally considered safer for handling hazardous materials due to their sealed design. However, positive pressure systems can be safer for handling non-hazardous materials if proper ventilation and dust collection systems are in place.
Ultimately, the choice between positive and negative pressure conveying for coal and limestone powder depends on a combination of operational requirements, material characteristics, and environmental constraints. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing customized pneumatic conveying systems that address these factors. By evaluating the specific needs of each project, the company can recommend the most efficient and effective conveying method, whether it be positive or negative pressure. This tailored approach ensures optimal performance, reduced downtime, and compliance with industry standards. For businesses in the coal and limestone powder industry, understanding the nuances of both positive and negative pressure conveying is essential to selecting the right material handling solution and maximizing operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top