For industrial operations dealing with fine powders, such as recirculating coke powder, the efficient and reliable transport of these materials is crucial. A specialized system designed for this purpose is the recirculating powder material conveying system. This article explores the fundamental concepts behind such systems, focusing on their design principles and practical applications in industrial settings.
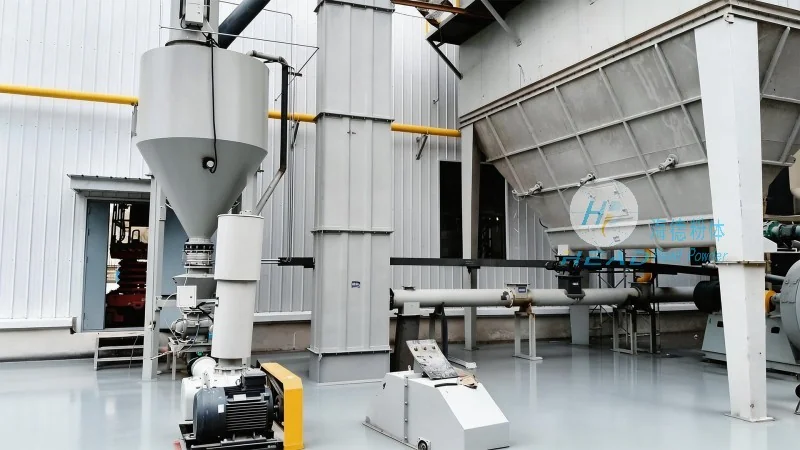
HeadPowder, a leading provider in the field of material handling solutions, specializes in developing advanced systems for powder processing. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for businesses seeking efficient and durable conveying solutions. The company’s expertise lies in understanding the unique challenges associated with handling fine powders like recirculating coke powder, ensuring that their systems are tailored to meet specific operational requirements.
The design of a recirculating powder material conveying system is built on several key principles aimed at optimizing material transport while minimizing issues like clogging, degradation, or loss. The primary goal is to create a closed-loop system that continuously moves the powder from a storage or processing point to a discharge point, often with the capability to return excess or unused material back to the system. This closed-loop approach not only enhances efficiency but also reduces waste and operational costs.
One of the fundamental design elements is the choice of conveying method. Common technologies include pneumatic conveying (using air pressure to move powder), mechanical conveying (such as screw conveyors or belt conveyors), and hybrid systems that combine both. For fine powders like recirculating coke powder, pneumatic conveying is often preferred due to its ability to handle high volumes and minimize particle degradation. The system typically consists of a hopper for material storage, a conveying line (often with multiple segments), and a control system to regulate flow rates and pressure.
Another critical aspect is the system’s ability to handle variations in powder properties. Recirculating coke powder, for example, may have different particle sizes, moisture content, or flow characteristics. The design must accommodate these variations by incorporating adjustable components, such as variable speed drives or pressure regulators, to maintain consistent performance. Additionally, the system is often equipped with features like air filtration and dust collection to ensure environmental compliance and operator safety.
A recirculating powder material conveying system comprises several interconnected components, each playing a vital role in the overall operation. The primary components include:
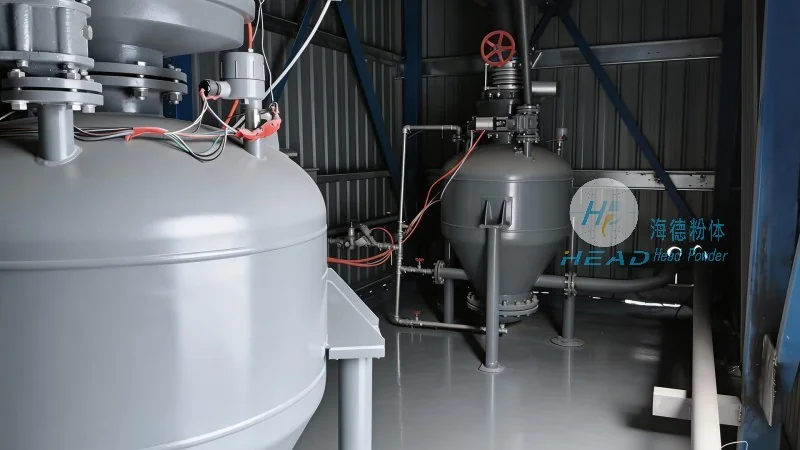
1. Material Hopper: This is the storage unit where the recirculating coke powder is initially held. It is designed to be large enough to accommodate the required volume and often includes a feeding mechanism, such as a rotary valve or a gate, to control the flow of material into the conveying line.
2. Conveying Line: The main pathway for transporting the powder. This can be a flexible hose, a rigid pipe, or a combination of both, depending on the system design. The line is typically made of materials resistant to corrosion and wear, such as stainless steel or specialized plastics, to ensure durability and prevent contamination.
3. Air Compressor or Blower: In pneumatic systems, this component generates the necessary air pressure to move the powder through the line. The choice of compressor depends on the system’s capacity and the specific powder characteristics, with options ranging from rotary lobe compressors to centrifugal blowers.
4. Control System: This includes sensors, valves, and a control panel that monitors and regulates the system’s operation. It ensures that the flow rate, pressure, and temperature are maintained within optimal ranges, preventing issues like overloading or under-conveying.
5. Return Loop: A critical feature for recirculating systems, this component allows excess material to be returned to the hopper or a storage bin. This loop helps maintain a consistent material level and reduces waste by reusing unused powder.
Recirculating powder material conveying systems are widely used in various industries where fine powders are processed. Some common applications include:
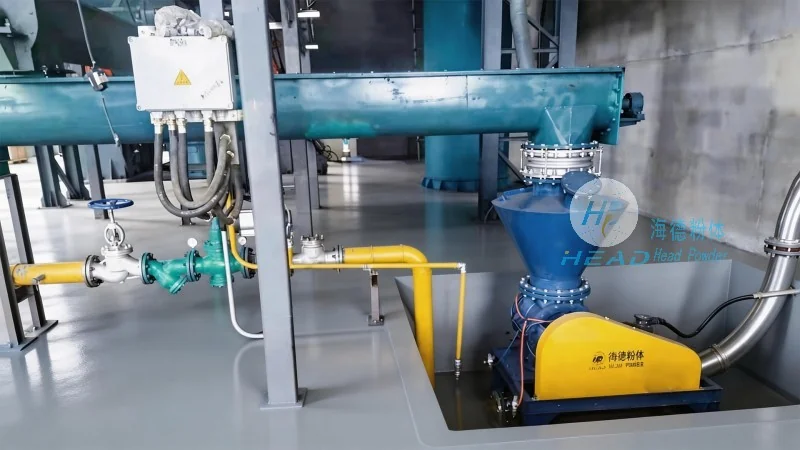
1. Cement and Concrete Production: In these industries, the efficient transport of cement and other powders is essential for maintaining production rates. The system ensures that the powder is delivered to mixing plants without degradation, contributing to the quality of the final product.
2. Chemical Manufacturing: Many chemical processes involve handling fine powders, such as pigments or catalysts. The recirculating system helps maintain consistent material flow, reducing downtime and improving process efficiency.
3. Food and Pharmaceutical Industries: For these sectors, the system must meet strict hygiene and safety standards. The design often includes features like stainless steel components, air filtration, and easy cleaning mechanisms to ensure compliance with regulatory requirements.
4. Mining and Mineral Processing: In mining operations, the system is used to transport crushed minerals or ores. The recirculating design helps manage large volumes of material and reduces the need for manual handling, improving overall operational safety.
Recirculating powder material conveying systems are essential for industries dealing with fine powders, providing an efficient and reliable method for material transport. The design principles, including closed-loop operation, adjustable components, and robust construction, ensure that these systems can handle the unique challenges associated with materials like recirculating coke powder. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in developing and implementing such systems, helping businesses optimize their operations and reduce costs. By understanding the core design principles and key components, industries can select and operate these systems effectively, enhancing productivity and maintaining product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top