For businesses in the coffee processing and distribution industry, selecting the appropriate dry coffee conveying method is crucial for maintaining product quality and operational efficiency. The choice of conveying system directly impacts the integrity of the coffee beans, ensuring they remain free from contamination and damage during transport. This article explores various dry coffee conveying methods offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, focusing on their effectiveness and suitability for different operational needs.
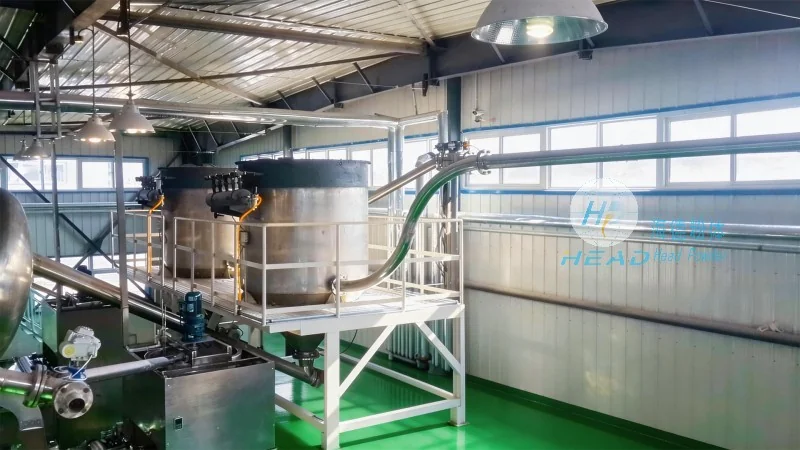
Belt conveyors are one of the most common and versatile dry coffee conveying solutions. They are ideal for transporting coffee beans over short to medium distances within a processing facility. The system typically consists of a continuous loop of a flexible belt, which moves the coffee beans from one point to another. This method is particularly effective for handling bulk quantities of coffee, as it can accommodate large volumes with minimal labor. The smooth surface of the belt reduces friction and prevents the coffee beans from being crushed or broken, preserving their flavor and aroma. HeadPowder’s belt conveyor systems are designed with high-quality materials, ensuring durability and low maintenance costs. They are equipped with adjustable speed controls and can be customized to fit specific production line configurations, making them a reliable choice for coffee processing plants.
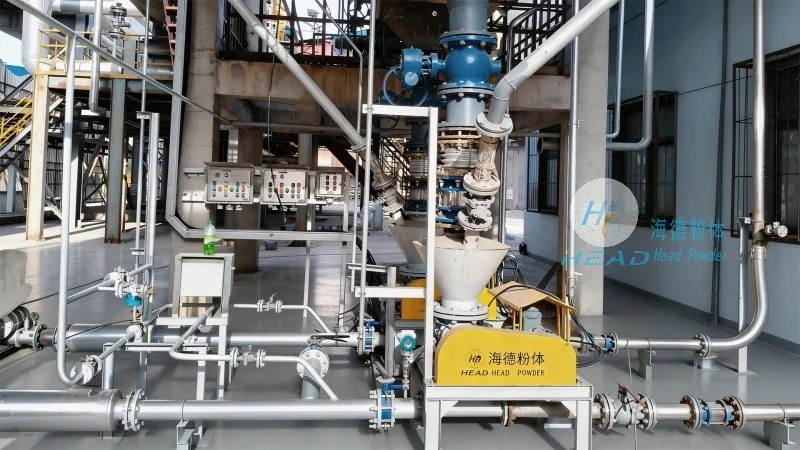
Screw conveyors, also known as auger conveyors, are another popular option for dry coffee conveying. These systems use a rotating screw or auger to move coffee beans through a tube or trough. Screw conveyors are well-suited for vertical or inclined transport, allowing coffee to be moved from lower to higher levels without the need for additional equipment. They are particularly effective for handling fine or powdery coffee products, as the screw design prevents material from sticking to the sides of the conveyor. HeadPowder’s screw conveyors are constructed with stainless steel components, which are resistant to corrosion and easy to clean, meeting the stringent hygiene standards required in the food industry. The variable speed and direction controls enable precise control over the flow rate, ensuring consistent and controlled transport of coffee beans. This makes screw conveyors an excellent choice for applications where product integrity and uniformity are paramount.
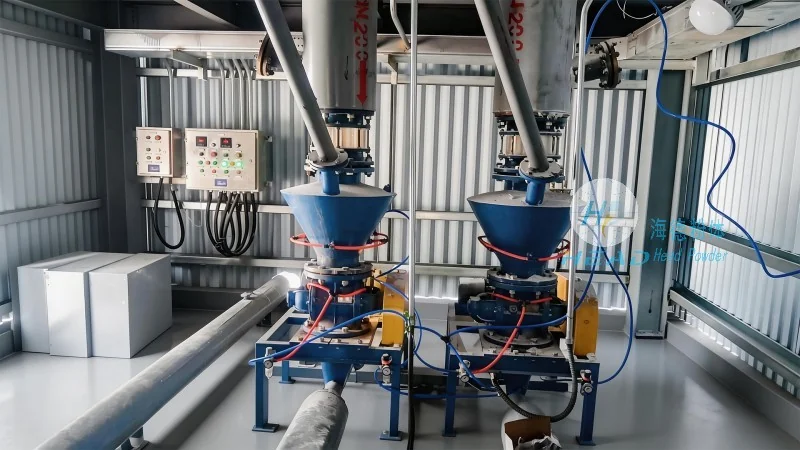
Pneumatic conveying systems utilize air pressure to transport dry coffee beans through a network of pipes. This method is highly efficient for long-distance transport and can handle both bulk and granular coffee products. The system operates by creating a vacuum or pressure differential that moves the coffee beans through the pipeline. Pneumatic conveyors are particularly advantageous for applications where dust control and contamination prevention are critical. They are also suitable for transporting coffee beans in a closed system, reducing exposure to environmental factors and maintaining product freshness. HeadPowder’s pneumatic conveying systems are designed with high-efficiency air pumps and filtration units, ensuring minimal air loss and optimal performance. The flexible piping allows for easy integration into existing production lines, and the system can be configured for both positive and negative pressure operation. This versatility makes pneumatic conveying an ideal solution for coffee processing facilities that require efficient and hygienic transport over extended distances.
Bucket elevators are specialized dry coffee conveying equipment used for vertical transport of coffee beans. These systems consist of a vertical or inclined conveyor with a series of buckets attached to a chain or belt. As the conveyor rotates, the buckets scoop up coffee beans from a lower hopper and lift them to a higher level. Bucket elevators are highly efficient for vertical transport, capable of moving large volumes of coffee with minimal power consumption. They are particularly effective for applications where space is limited and vertical space is available. HeadPowder’s bucket elevators are constructed with heavy-duty materials, ensuring durability and long service life. The buckets are designed to minimize product spillage and damage, preserving the quality of the coffee beans. The system is equipped with safety features such as overload protection and emergency stop buttons, ensuring safe operation in industrial environments. This makes bucket elevators a reliable choice for coffee processing plants that require vertical transport of coffee beans to upper levels of the facility.
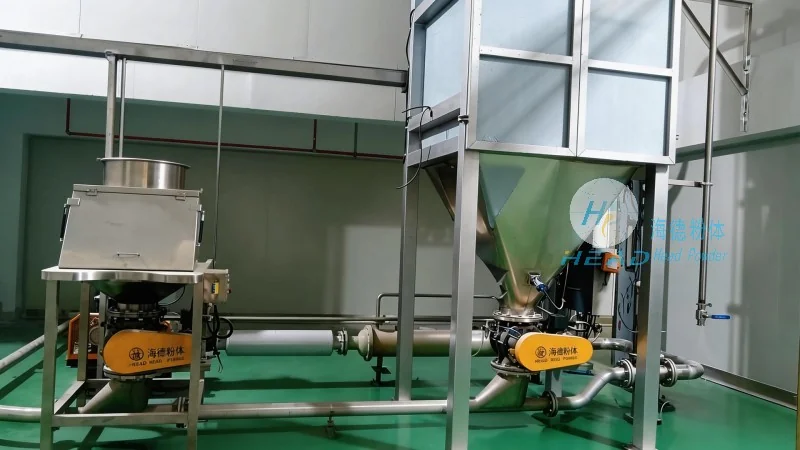
Vibrating conveyors are a gentle yet effective method for dry coffee conveying. These systems use vibration to move coffee beans along a trough or conveyor bed. The vibration is typically generated by an electric motor or a mechanical drive, causing the coffee beans to move forward in a controlled manner. Vibrating conveyors are ideal for handling delicate or fragile coffee products, as they minimize the risk of breakage or damage. They are particularly effective for transporting coffee beans over long distances with minimal energy consumption. HeadPowder’s vibrating conveyors are designed with adjustable vibration frequencies and amplitudes, allowing for precise control over the transport speed and direction. The troughs are made of non-stick materials, preventing coffee beans from sticking to the surface and ensuring smooth movement. This method is especially suitable for applications where product quality and integrity are critical, such as for specialty coffee beans or high-value coffee products. The gentle handling provided by vibrating conveyors helps maintain the natural flavor and aroma of the coffee beans, making them a preferred choice for premium coffee processing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top