Understanding negative pressure dilute phase pneumatic conveying systems is crucial for industries that rely on efficient material handling solutions. These systems represent a sophisticated approach to transporting bulk materials through a pipeline using air as the primary medium, operating under a negative pressure environment. This method is particularly effective for handling a wide range of materials, from powders to granules, while ensuring minimal product degradation and contamination.
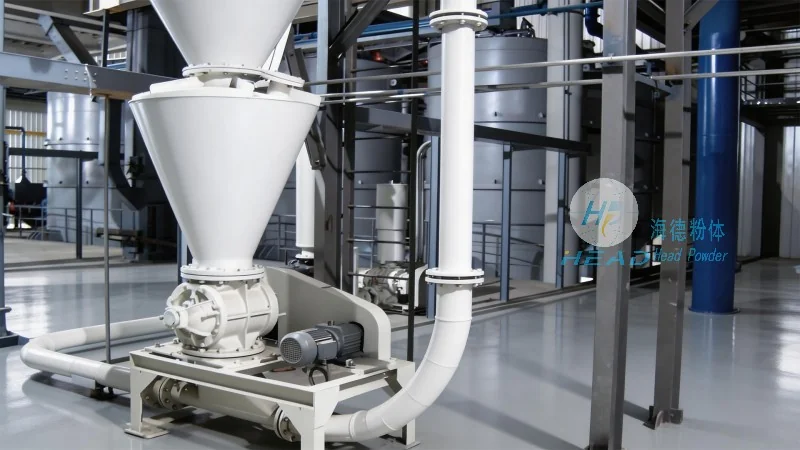
A negative pressure dilute phase pneumatic conveying system is a type of pneumatic conveying technology that uses a vacuum or negative pressure to draw material from a source into a conveying line. The system operates by creating a pressure differential between the material source and the receiving end, allowing air to flow through the pipeline while carrying the material particles. This approach is often preferred in applications where product purity and gentle handling are critical, as the low velocity and dilute phase (where material is dispersed in air) minimize the risk of material degradation or agglomeration.
The design of a negative pressure dilute phase system involves several key components that work in tandem to ensure efficient material transport. The primary components include a material feed hopper, a rotary airlock valve, a vacuum pump or fan, a conveying pipeline, and a receiving hopper or silo. The process begins with the material being fed into the hopper, where it is then discharged into the pipeline through the rotary airlock valve. The vacuum pump creates a negative pressure in the pipeline, drawing air and material particles from the source into the line. As the material travels through the pipeline, it is suspended in the air stream and transported to the receiving end. The receiving hopper collects the material, and the air is typically filtered and recycled back into the system.
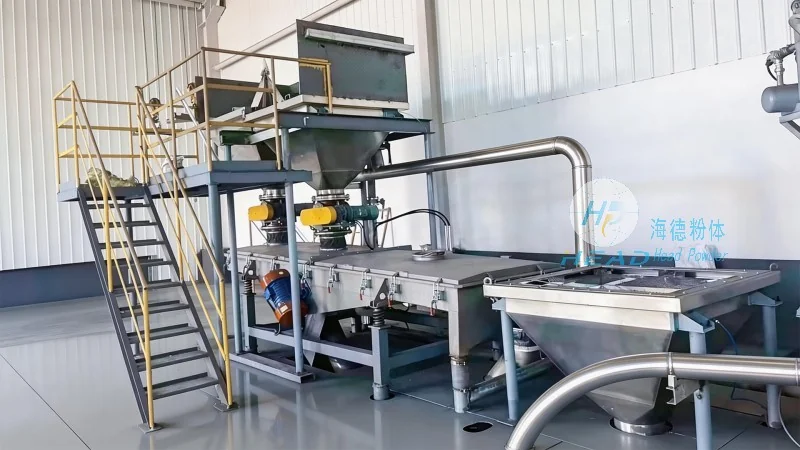
The design of a negative pressure dilute phase system must consider several critical factors to ensure optimal performance and reliability. One of the most important considerations is the material characteristics, such as particle size, density, and flowability, as these factors directly impact the conveying velocity and pressure requirements. The system must be designed to handle the specific material properties while maintaining a stable flow and preventing blockages or clogging. Additionally, the pipeline layout and length are crucial, as they affect the pressure drop and energy consumption. Proper sizing of the pipeline diameter and the vacuum pump capacity is essential to ensure that the system can handle the required material flow rate without excessive energy use. The system also needs to incorporate features like air filtration and moisture control to maintain product quality and prevent equipment damage.
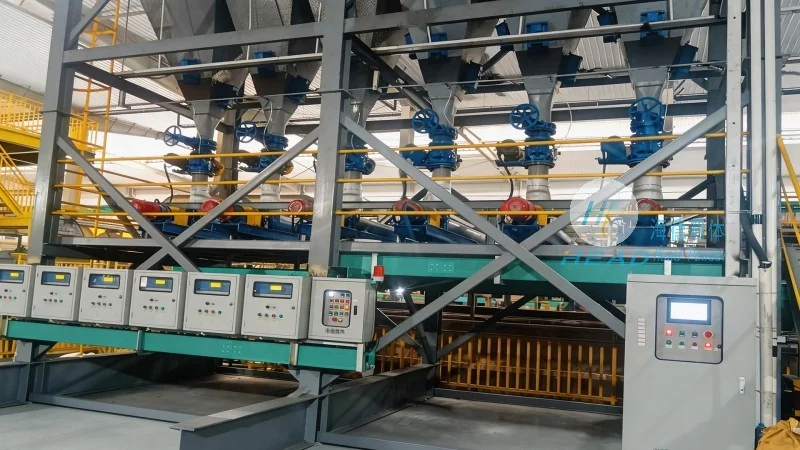
Negative pressure dilute phase pneumatic conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. These systems offer several advantages over other material handling methods, such as reduced product contamination, minimal material degradation, and the ability to handle a wide range of materials. The negative pressure operation also helps in controlling dust emissions and maintaining a clean working environment. Furthermore, the system's flexibility allows for easy integration into existing production lines and can be adapted to handle different material types and flow rates. The benefits of using this technology include improved process efficiency, reduced labor costs, and enhanced product quality, making it a preferred choice for many industries.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a strong focus on innovation and quality, HeadPowder specializes in designing and manufacturing negative pressure dilute phase pneumatic conveying systems tailored to meet the specific needs of various industries. The company's expertise lies in understanding the unique challenges of material handling and developing customized solutions that enhance operational efficiency and product quality. HeadPowder's commitment to excellence is reflected in its state-of-the-art manufacturing facilities, rigorous quality control processes, and dedicated customer support. Based in Shandong, China, HeadPowder serves clients globally, providing reliable and efficient material handling systems that help businesses optimize their production processes and achieve their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top