When it comes to the efficient and safe transportation of sulfur materials in industrial settings, specialized equipment is essential. The sulfur material handling conveyor, a critical component in many processing and storage operations, is designed to address the unique challenges associated with handling this specific material. This article explores the fundamental aspects of sulfur material handling conveyors, including their design principles and operational benefits.
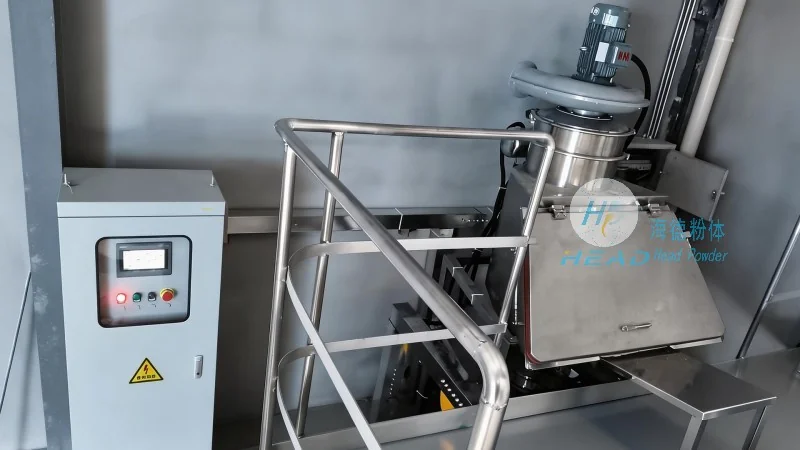
In industrial applications, sulfur is often handled in bulk quantities, requiring reliable and efficient equipment to move it from one point to another. Sulfur material handling conveyors are engineered to meet these demands, providing a safe and effective solution for transporting sulfur in various forms, such as granules, powder, or solid blocks. These systems are particularly important in industries like chemical manufacturing, mining, and energy production, where sulfur is a key raw material or byproduct.
The design of a sulfur material handling conveyor is based on several critical principles to ensure optimal performance and safety. First, material compatibility is paramount. The conveyor components, including the belt, idlers, and frame, must be constructed from materials that can withstand the corrosive and abrasive nature of sulfur. Common materials used include stainless steel, high-grade alloys, and specialized polymers that resist chemical attack and wear. This ensures the longevity of the equipment and prevents contamination of the sulfur material.
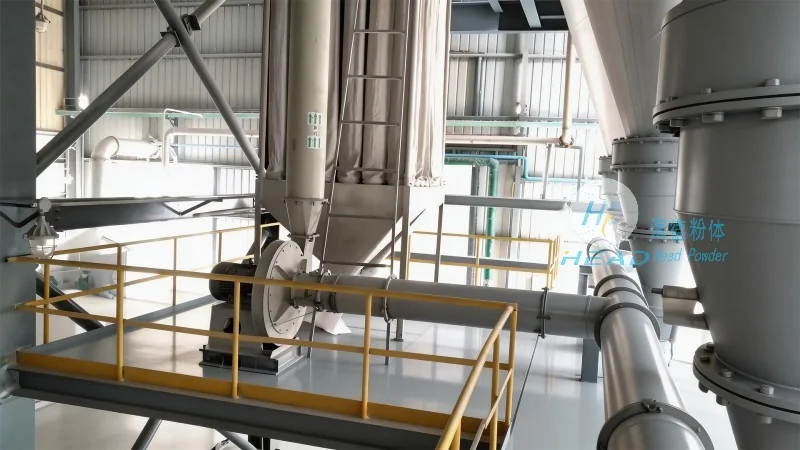
Second, the conveyor system must be designed to handle the specific physical properties of sulfur. Sulfur can vary in form and density, and the conveyor must be capable of accommodating these variations. For example, some systems may include adjustable feed mechanisms or variable speed drives to control the flow rate and prevent overloading. Additionally, the design may incorporate features like temperature control or cooling systems to manage the thermal properties of sulfur, which can be sensitive to temperature changes.
A typical sulfur material handling conveyor consists of several key components that work together to ensure smooth operation. The primary component is the conveyor belt, which is responsible for carrying the sulfur material. The belt is typically made from a durable material, such as rubber or polyurethane, and is reinforced with steel or other strong fibers to withstand heavy loads and abrasion. The idlers, which support the belt as it moves, are also designed to be robust and resistant to sulfur's corrosive effects.
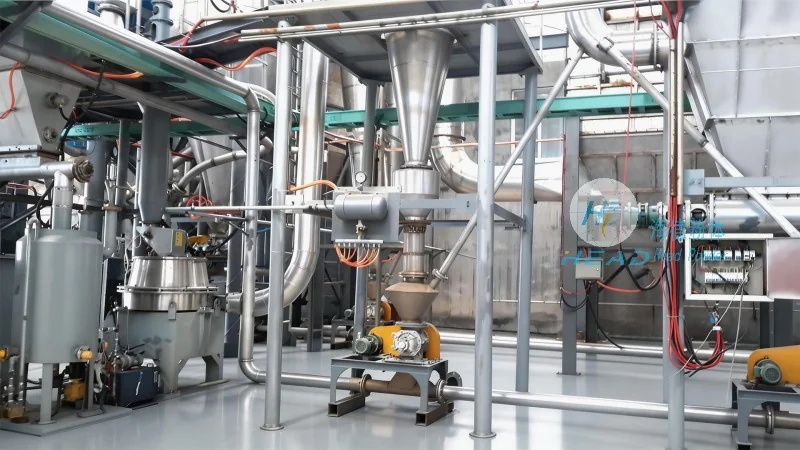
The drive system, which powers the conveyor, is another critical component. It may include electric motors, gearboxes, and pulleys that work in tandem to maintain consistent speed and tension. The tensioning system is essential to keep the belt properly aligned and prevent slippage or sagging, which could lead to material spillage or equipment failure. Additionally, the conveyor may include safety features such as emergency stop buttons, overload protection, and sensors to detect blockages or misalignments.
The use of sulfur material handling conveyors offers numerous benefits for industrial operations. By automating the transportation of sulfur, these systems reduce the need for manual handling, which can be hazardous due to the material's potential to cause skin irritation or respiratory issues. Automated conveyors also improve efficiency by maintaining consistent flow rates and reducing downtime caused by human error or fatigue. Furthermore, the design of these systems minimizes material loss and contamination, ensuring that the sulfur remains in its intended form and quality.
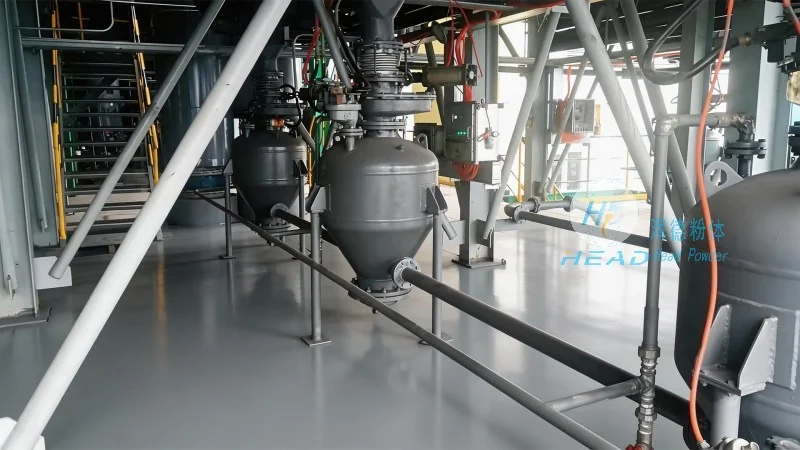
In practical applications, sulfur material handling conveyors are used in a variety of settings. For example, in chemical plants, they may be used to transport sulfur from storage silos to processing units, where it is converted into other products like sulfuric acid. In mining operations, they can be employed to move sulfur ore from the mine to processing facilities. The versatility of these conveyors makes them suitable for a wide range of industrial processes where sulfur is a key component.
Sulfur material handling conveyors are essential equipment for industries that rely on the efficient and safe transportation of sulfur materials. Their design, based on principles of material compatibility, durability, and operational efficiency, ensures that they can meet the demands of modern industrial applications. As a leading provider of engineering solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality sulfur material handling conveyors tailored to the specific needs of its clients. With a focus on safety, reliability, and performance, the company's products help businesses optimize their operations and ensure the smooth flow of sulfur materials in their processes. Based in China, Shandong HeadPowder Engineering Co., Ltd. serves a global market, providing customized solutions that enhance productivity and reduce operational risks.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top