Red mud, a byproduct of bauxite processing in the aluminum industry, poses significant handling and transportation challenges due to its high moisture content, abrasive nature, and potential environmental hazards. The efficient and reliable transport of red mud from processing facilities to disposal or recycling sites is critical for industrial operations, and pneumatic conveying systems have emerged as a preferred solution. This article provides a technical analysis of red mud pneumatic conveying systems, focusing on the comparison between positive pressure and negative pressure conveying modes, with insights from Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions based in Shandong, China.
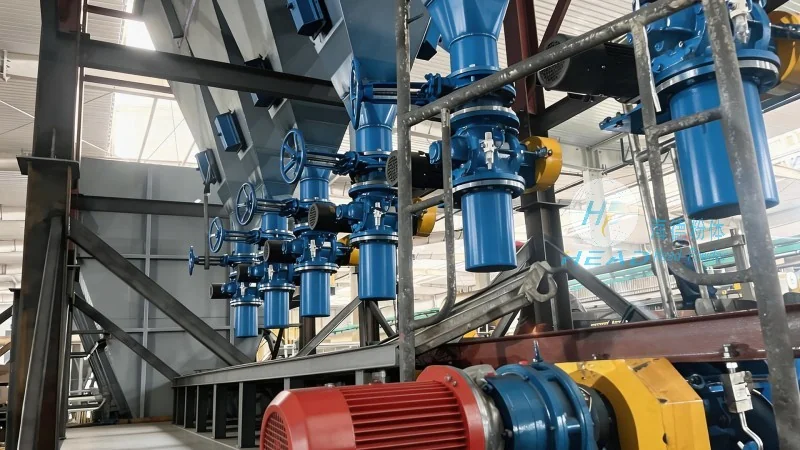
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored to the unique requirements of red mud handling. With years of experience in the field, the company has developed expertise in optimizing system performance, ensuring durability under harsh operating conditions, and minimizing operational costs. The following sections delve into the technical aspects of both positive and negative pressure conveying modes, highlighting their applications, advantages, and limitations in red mud transportation.
Positive pressure pneumatic conveying systems operate by generating air pressure within the conveying line, which forces the material to move from the source to the destination. In the context of red mud, this mode typically involves a high-pressure blower or compressor that supplies air to the system, creating a positive pressure environment. The material is fed into the conveying line via a hopper or feeder, and the air flow propels the red mud particles through the pipeline. This method is particularly effective for long-distance and high-capacity transportation, as it can handle larger particle sizes and higher moisture content compared to negative pressure systems.
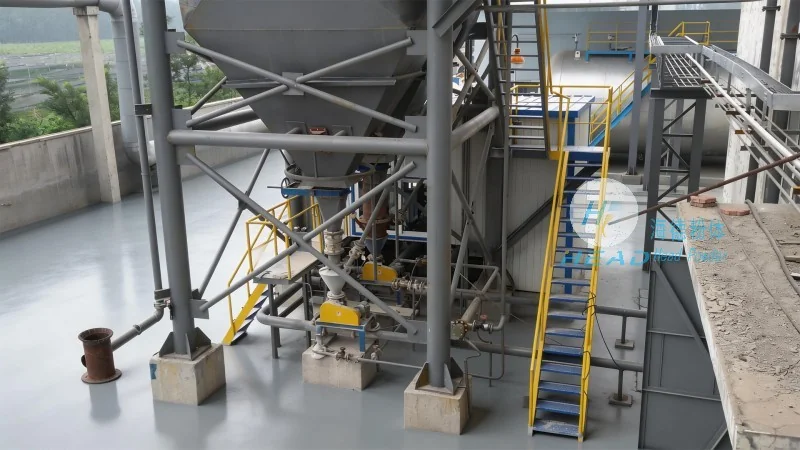
Key components of a positive pressure red mud conveying system include the air compressor, feed hopper, conveying line, and discharge equipment. The air compressor is responsible for maintaining the required pressure, while the feed hopper ensures a consistent material supply. The conveying line, often made of corrosion-resistant materials such as stainless steel or polyethylene, is designed to withstand the abrasive nature of red mud. Discharge equipment, such as rotary valves or airlocks, controls the release of material at the destination. Positive pressure systems are also equipped with filtration and dust collection systems to manage air emissions and ensure compliance with environmental regulations.
Negative pressure pneumatic conveying systems, also known as suction or vacuum systems, operate by creating a vacuum in the conveying line, which draws the material from the source to the destination. This mode is typically used for shorter distances and lower capacity applications, as the suction force is generally lower than the pressure force in positive systems. In red mud handling, negative pressure systems are often employed for transporting material from storage silos or processing units to a central collection point.
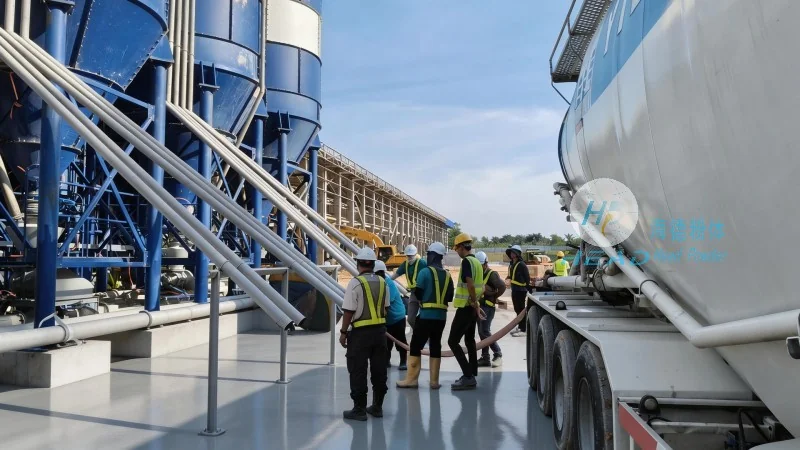
The core components of a negative pressure red mud conveying system include a vacuum pump, feed hopper, conveying line, and discharge equipment. The vacuum pump generates the necessary suction force, while the feed hopper provides the material feed. The conveying line is designed to maintain the vacuum, and the discharge equipment controls the material release. Unlike positive pressure systems, negative pressure systems may require additional filtration and air treatment to manage the intake of ambient air and prevent dust contamination. This mode is generally more suitable for handling fine particles and lower moisture content materials, as the suction force may not be sufficient to transport larger or more abrasive particles efficiently.
When selecting a pneumatic conveying system for red mud transportation, it is essential to evaluate the suitability of both positive and negative pressure modes based on specific operational requirements. The choice between the two depends on factors such as distance, capacity, material characteristics, and environmental considerations.
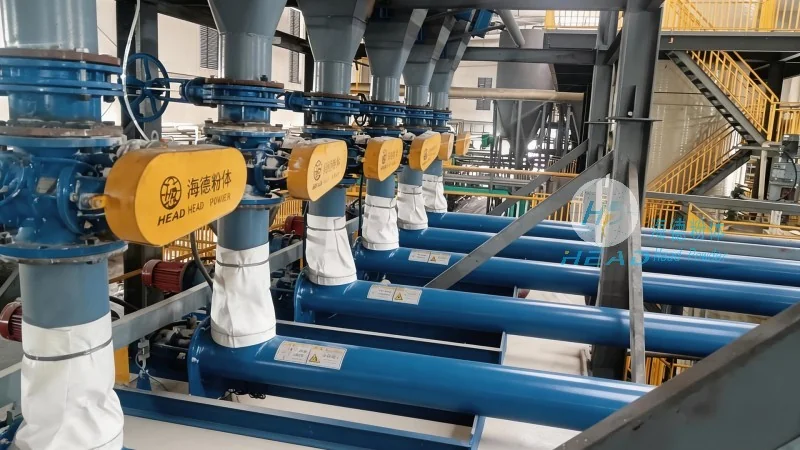
Positive pressure systems offer higher conveying capacity and are more effective for long-distance transport, making them ideal for large-scale red mud handling operations. They can handle a wider range of particle sizes and moisture levels, and the positive pressure environment reduces the risk of material clogging in the pipeline. However, positive pressure systems require more robust equipment, higher energy consumption, and more stringent safety measures due to the high-pressure air supply. Additionally, the cost of corrosion-resistant materials for the conveying line and the need for comprehensive filtration systems can increase the overall investment and operational costs.
Negative pressure systems, on the other hand, are more energy-efficient and require less maintenance compared to positive systems. They are suitable for shorter distances and lower capacity applications, and the vacuum environment helps to minimize dust emissions at the source. However, negative pressure systems have lower conveying capacity and are less effective for handling large or abrasive particles. The suction force may not be sufficient to transport material over long distances, and the system is more susceptible to clogging due to the lower air velocity. Environmental regulations may also impose stricter requirements on negative pressure systems, as the intake of ambient air can lead to increased dust and particulate matter emissions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top