For industrial applications involving the transport of bulk materials like cement fly ash, selecting the right pneumatic conveying system is crucial for efficiency, cost-effectiveness, and operational safety. This article provides a technical analysis of cement fly ash pneumatic conveying systems, focusing on the comparison between positive pressure and negative pressure conveying modes. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, with the company's headquarters located in Shandong, China.
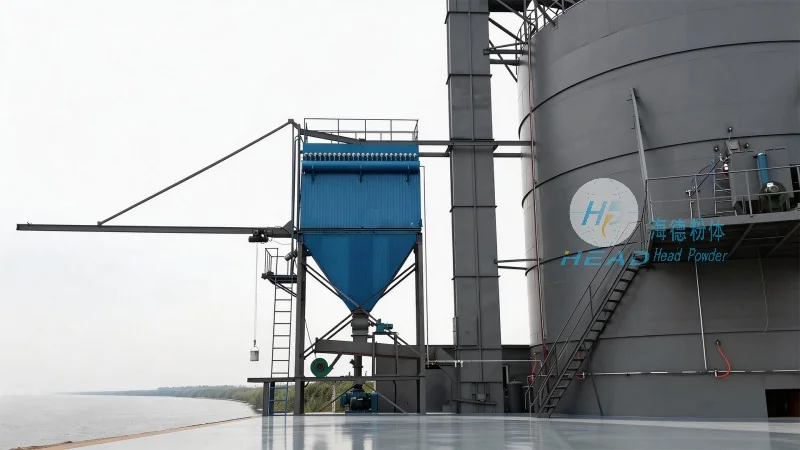
Pneumatic conveying systems are widely used in the cement and construction industries to transport cement fly ash, a byproduct of cement production, from storage silos to processing or disposal sites. These systems utilize air or gas to move the material through a pipeline, offering advantages such as reduced labor costs, improved safety (as it eliminates manual handling), and the ability to transport materials over long distances. The primary challenge in designing an effective system lies in choosing the appropriate conveying mode—positive pressure or negative pressure—based on the specific requirements of the application.
Positive pressure conveying systems operate by blowing air or gas into the material to be transported, creating a pressure higher than the ambient air pressure. This method is often referred to as "blow" or "pressure" conveying. In a positive pressure system, the material is fed into a hopper or silo, and a fan or blower generates the necessary pressure to push the material through the pipeline. The system typically includes a dust collector to capture any airborne particles and a control system to regulate the flow rate.
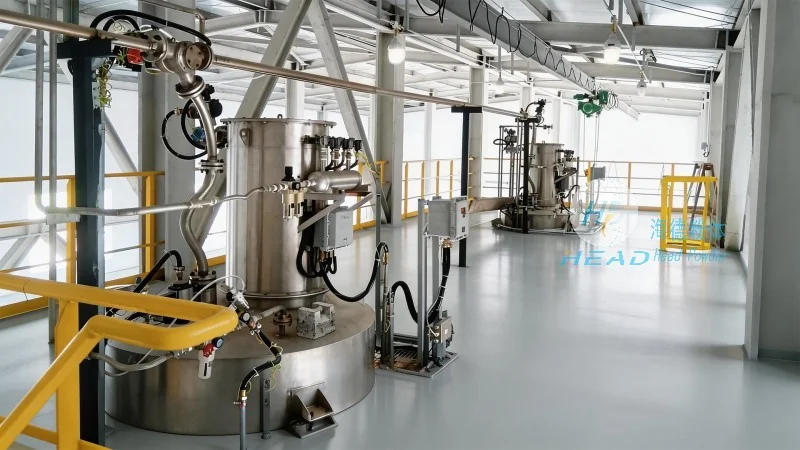
Key advantages of positive pressure conveying include its ability to handle high material loads, its suitability for long-distance transport, and its effectiveness in conveying abrasive materials like cement fly ash. However, this mode may require more robust equipment to withstand higher pressures and can be more expensive to install and maintain. Additionally, positive pressure systems may generate more noise and require proper ventilation to manage air emissions.
Negative pressure conveying, also known as "suction" or "vacuum" conveying, operates by creating a vacuum in the pipeline, drawing the material into the system. The material is fed into a hopper or silo, and a vacuum pump creates a pressure lower than the ambient air pressure, pulling the material through the pipeline. Unlike positive pressure systems, negative pressure systems do not require high-pressure fans and can be more compact in design.
Advantages of negative pressure conveying include lower initial costs, reduced noise levels, and the ability to handle materials with lower moisture content. However, this mode is generally less suitable for long-distance transport or high material loads, as the vacuum pressure may not be sufficient to move large quantities of material efficiently. Negative pressure systems are also more prone to clogging and may require more frequent maintenance to prevent material buildup in the pipeline.
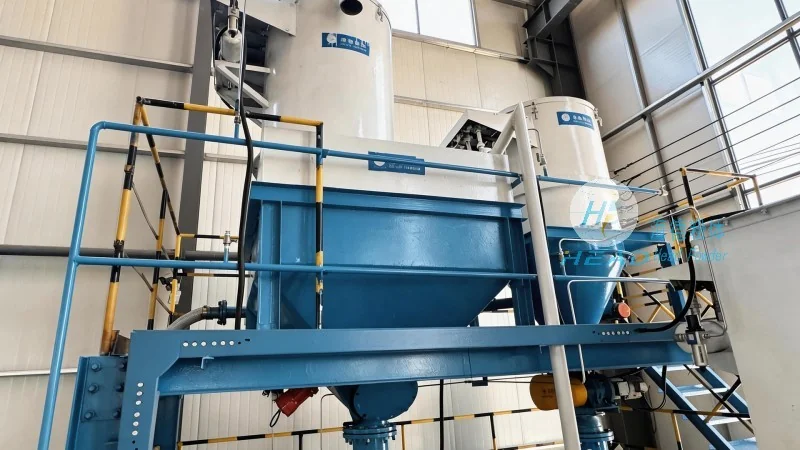
When selecting between positive pressure and negative pressure conveying for cement fly ash, several factors must be considered, including the distance of transport, the material's properties (such as moisture content and abrasiveness), the required flow rate, and the available space for equipment installation. The choice of system directly impacts operational efficiency, energy consumption, and overall cost.
For applications requiring long-distance transport or high material throughput, positive pressure conveying is often the preferred option due to its ability to handle high loads and maintain consistent flow rates over extended distances. The robust design of positive pressure systems ensures reliable operation even with abrasive materials like cement fly ash, which can cause wear and tear on equipment. However, the higher pressure requirements mean that positive pressure systems may require more powerful fans and additional safety measures to prevent leaks or pressure buildup.
On the other hand, negative pressure conveying is ideal for shorter transport distances or applications where noise reduction and lower initial costs are priorities. The compact design of negative pressure systems makes them suitable for installations with limited space, and the lower pressure requirements reduce energy consumption compared to positive pressure systems. However, negative pressure systems may struggle with high material loads or long distances, as the vacuum pressure may not be sufficient to move large quantities of material efficiently. Additionally, the risk of clogging is higher in negative pressure systems, which can lead to operational disruptions and increased maintenance costs.
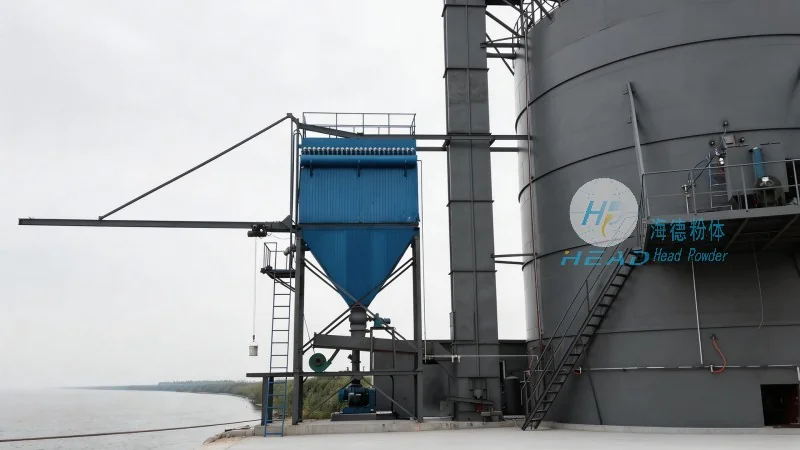
Several technical and operational factors influence the decision between positive and negative pressure conveying for cement fly ash. These factors include:
Both positive pressure and negative pressure conveying systems have their advantages and limitations when used for cement fly ash transport. The optimal choice depends on the specific requirements of the application, including distance, material properties, and operational constraints. Shandong HeadPowder Engineering Co., Ltd. offers comprehensive solutions for both modes, providing customized systems that meet the unique needs of each client. By carefully evaluating the factors discussed above, industrial facilities can select the most efficient and cost-effective pneumatic conveying system for their cement fly ash handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top