For industries dealing with mineral powders, optimizing transport efficiency while maintaining a clean and safe working environment is a critical challenge. Traditional methods like belt conveyors or bucket elevators often struggle with dust generation, material degradation, and operational inefficiencies. This is where pneumatic conveying technology emerges as a superior solution, offering a clean, efficient, and versatile approach to mineral powder transport. This article delves into the principles, benefits, and practical applications of pneumatic conveying systems, highlighting why it is the ideal choice for modern mineral processing operations.
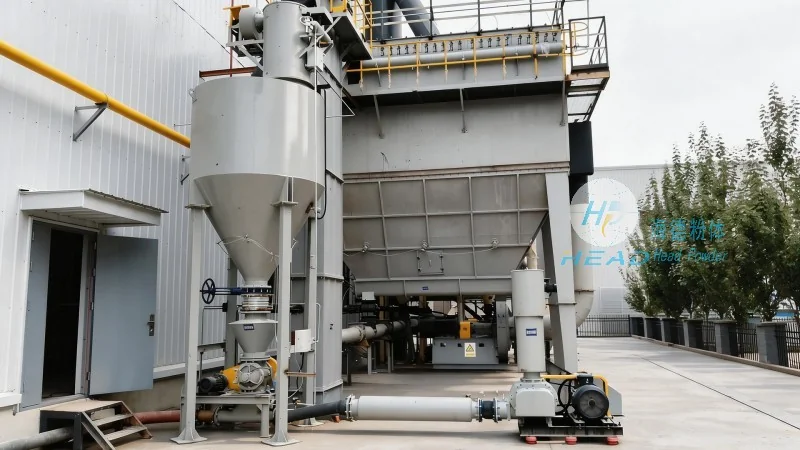
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like mineral powders through a pipeline using a stream of air. Unlike mechanical systems that rely on physical contact and friction, pneumatic systems use air pressure to move materials, minimizing wear and tear on the product. This technology is particularly well-suited for fine powders, granules, and other dry bulk materials commonly found in mining, cement, chemical, and food processing industries. The core of a pneumatic conveying system consists of a hopper for material storage, a conveyor line (often a pipeline), and a blower or compressor to generate the air flow. The system can operate in either positive pressure (where air pushes the material) or negative pressure (where air pulls the material), depending on the application and material characteristics.
One of the most significant advantages of pneumatic conveying is its ability to deliver mineral powders in a dust-free environment. Unlike traditional bulk handling methods that generate airborne dust, which poses health risks and contamination concerns, pneumatic systems enclose the material within a sealed pipeline. This not only protects workers from respiratory hazards but also prevents product contamination, ensuring the purity of the mineral powder is maintained throughout the transport process. Additionally, pneumatic conveying reduces material degradation by minimizing friction and impact, which is crucial for delicate or high-value mineral powders. The technology also offers high transport efficiency, with the ability to move materials over long distances (up to several kilometers) with minimal energy loss. This makes it ideal for large-scale industrial applications where traditional conveyors may be impractical or inefficient.
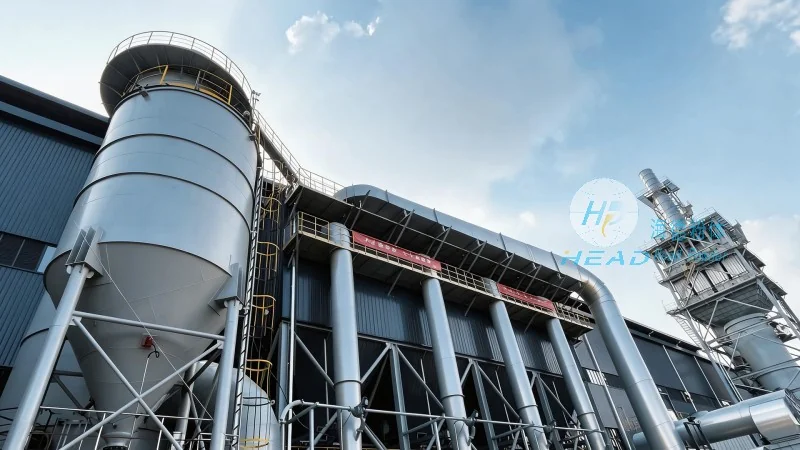
The operation of a pneumatic conveying system involves several key components and processes. First, the mineral powder is loaded into a hopper or feeder, which feeds the material into the conveyor line. The blower or compressor then generates a high-pressure air stream that propels the material through the pipeline. In positive pressure systems, the air pushes the material forward, while in negative pressure systems, the air pulls the material from the source. The system may include additional components such as cyclones or filters to separate the material from the air stream at the destination, ensuring the material is deposited accurately and the air is cleaned before release. The control system manages the flow rate, pressure, and direction of the air, ensuring smooth and consistent transport. This automation allows for precise control over the conveying process, reducing downtime and improving overall operational efficiency.
Pneumatic conveying technology is widely used across various industries dealing with mineral powders. In the mining sector, it is employed to transport ore from crushers to storage silos or processing plants, ensuring a continuous and clean supply of raw materials. In cement production, it is used to convey raw materials like limestone, clay, and iron ore to the kilns, where precise control over material flow is essential for optimal combustion. The chemical industry utilizes pneumatic conveying for transporting powders such as pigments, catalysts, and reagents, where contamination control is critical. Even in the food and pharmaceutical industries, where hygiene and product purity are paramount, pneumatic systems are preferred for handling powders like flour, sugar, or pharmaceutical powders. The versatility of pneumatic conveying makes it adaptable to a wide range of applications, from small-scale laboratory operations to large-scale industrial plants.
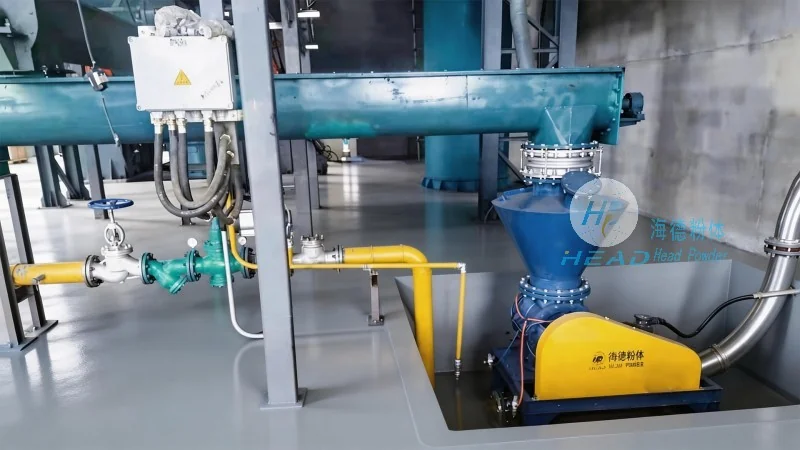
When selecting a pneumatic conveying system for mineral powder transport, several factors must be considered to ensure optimal performance and efficiency. The first consideration is the material characteristics, including particle size, density, and flowability. Fine powders with high moisture content may require specialized equipment, such as a positive pressure system with a high-capacity blower, to prevent clogging. The distance and elevation changes between the source and destination are also critical factors, as they determine the required air pressure and system design. For long-distance transport, a combination of positive and negative pressure stages may be used to minimize energy consumption. The system's capacity and reliability are equally important, as downtime can lead to significant production losses. Additionally, the environmental and safety requirements of the operation must be considered, as pneumatic systems must comply with regulations regarding dust control and air quality. Consulting with a specialized engineering company, such as Shandong HeadPowder Engineering Co., Ltd., can help in selecting the most suitable system based on specific operational needs and material characteristics.
Pneumatic conveying technology represents a significant advancement in mineral powder transport, offering a clean, efficient, and versatile solution that addresses the limitations of traditional bulk handling methods. By minimizing dust generation, reducing material degradation, and improving operational efficiency, pneumatic systems are increasingly becoming the preferred choice for modern industrial applications. As industries continue to prioritize sustainability and operational excellence, the adoption of advanced pneumatic conveying systems will likely grow, driving further innovation in mineral processing and bulk material handling. For companies dealing with mineral powders, investing in a well-designed pneumatic conveying system is not just a technological upgrade but a strategic move towards enhanced productivity, safety, and environmental compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top