For industrial applications involving borax, the choice of transport method significantly impacts operational efficiency, product quality, and overall cost-effectiveness. Traditional methods like belt conveyors or bucket elevators often face challenges such as material degradation, contamination risks, and limited flexibility in handling fine or hygroscopic powders like borax. In response to these challenges, pneumatic conveying technology has emerged as a superior solution, offering a clean, efficient, and versatile approach to borax transport. This article delves into the benefits and technical aspects of pneumatic conveying systems, highlighting how they enhance borax handling while maintaining high standards of cleanliness and operational reliability.
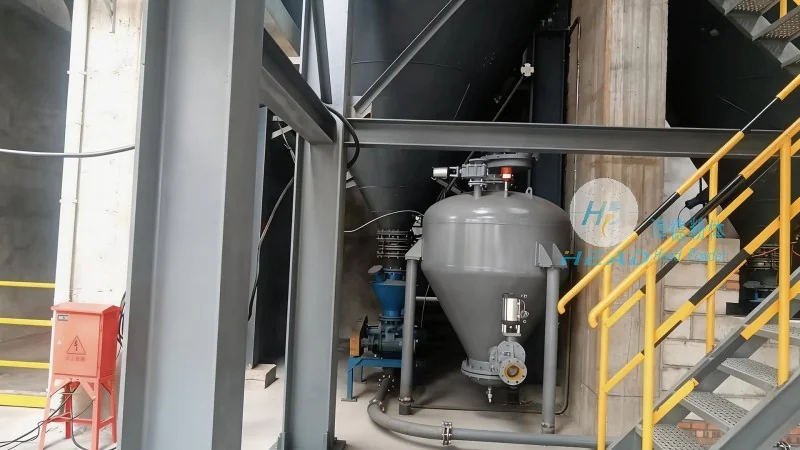
Pneumatic conveying, also known as air conveying, utilizes compressed air or gas to transport bulk materials through a pipeline system. Unlike mechanical systems that rely on physical contact with the material, pneumatic conveying minimizes direct contact, reducing the risk of product contamination and degradation. This makes it particularly suitable for handling sensitive materials like borax, which can be prone to caking or moisture absorption. The core components of a pneumatic conveying system typically include a material feeder, a conveying line, a separation or collection device, and a control system. Each component plays a critical role in ensuring smooth and efficient transport of borax from the source to the destination.
One of the primary benefits of pneumatic conveying for borax is its ability to maintain product integrity. By avoiding direct contact with machinery, the system reduces the risk of contamination from oils, lubricants, or other residues that may be present in mechanical systems. This is crucial for applications where borax is used in pharmaceuticals, food processing, or chemical manufacturing, where purity is paramount. Additionally, pneumatic conveying offers superior flexibility in handling varying material characteristics. It can accommodate different particle sizes, moisture contents, and flow rates, making it adaptable to diverse industrial needs. The system's ability to transport materials over long distances without the need for intermediate storage or handling points also streamlines operations and reduces downtime.
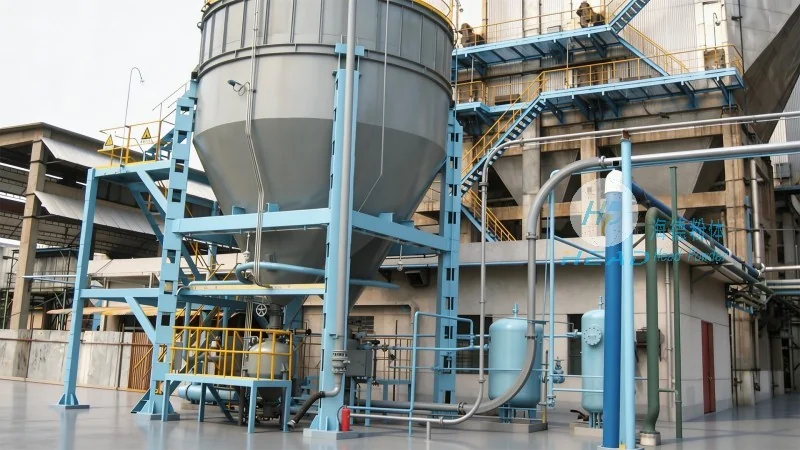
From an operational perspective, pneumatic conveying systems provide significant efficiency gains. Unlike traditional methods that may require multiple transfer points or manual handling, pneumatic systems can transport borax directly from storage silos to processing equipment, minimizing the need for manual intervention. This not only reduces labor costs but also enhances safety by eliminating the need for workers to handle bulk materials manually. Furthermore, the reduced maintenance requirements of pneumatic systems contribute to lower long-term operational costs. With fewer moving parts and less wear and tear compared to mechanical conveyors, the system requires less frequent repairs and replacements, leading to higher overall reliability and lower downtime.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of borax handling applications. With years of experience in the industry, HeadPowder understands the unique challenges associated with transporting fine, hygroscopic materials like borax. The company's team of engineers leverages advanced technology and engineering principles to develop systems that optimize efficiency, minimize contamination risks, and ensure consistent performance. HeadPowder's solutions are designed to meet the stringent requirements of various industries, including chemical, pharmaceutical, and food processing, where product purity and operational reliability are non-negotiable.
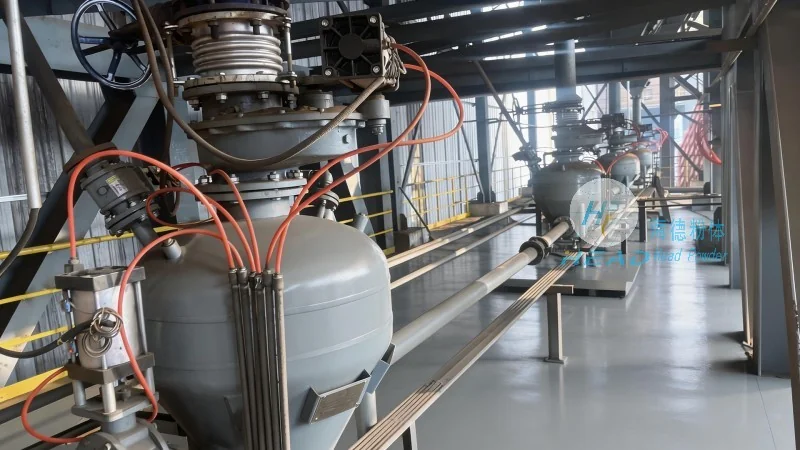
When implementing a pneumatic conveying system for borax transport, several factors must be carefully considered to ensure optimal performance. First, the material characteristics of borax, such as its particle size distribution, moisture content, and flowability, must be thoroughly analyzed. This information is critical in selecting the appropriate conveying system design, including the type of air flow (positive or negative pressure), the diameter of the conveying line, and the placement of components like feeders and separators. Second, the distance and layout of the transport route need to be evaluated to determine the most efficient system configuration. HeadPowder's engineers work closely with clients to conduct comprehensive assessments, ensuring that the system is tailored to the specific operational requirements and constraints of the facility. Additionally, factors such as energy consumption, maintenance requirements, and safety features must be considered to ensure the system aligns with the client's long-term goals and operational standards.
In conclusion, pneumatic conveying technology represents a significant advancement in the efficient and clean transport of borax. By leveraging compressed air to move materials through a pipeline system, these systems offer superior product integrity, operational flexibility, and cost savings compared to traditional mechanical methods. For industries relying on borax in their production processes, investing in a well-designed pneumatic conveying system is a strategic decision that enhances operational efficiency, maintains product quality, and reduces long-term costs. With expertise and experience in the field, companies like Shandong HeadPowder Engineering Co., Ltd. are positioned to provide tailored solutions that meet the evolving needs of the industry, ensuring that borax transport remains clean, efficient, and reliable for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top