Efficient and reliable long-distance pneumatic fertilizer transport systems are crucial for modern agricultural operations, enabling the safe and efficient movement of bulk fertilizers over extended distances. These systems leverage pneumatic conveying technology to transport materials like granular or powdered fertilizers from storage facilities to application sites, such as farms or processing plants. The design and implementation of such systems require careful consideration of factors including material properties, distance, and operational requirements to ensure optimal performance and minimal loss.
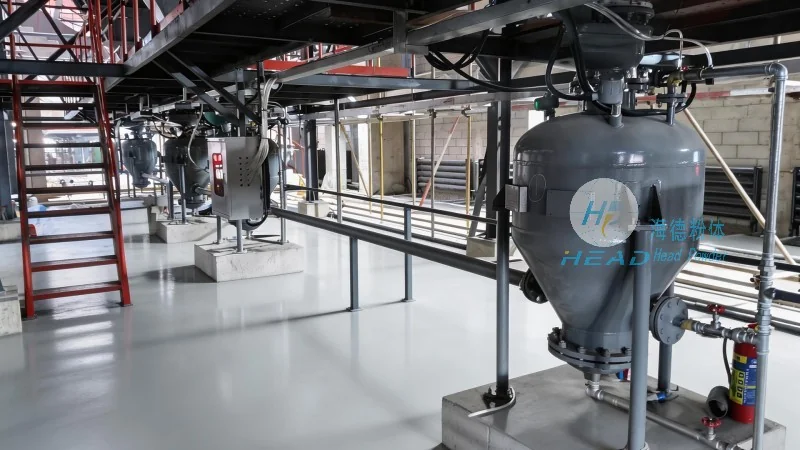
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the fertilizer industry. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for agricultural and industrial clients seeking efficient material handling solutions. The company’s expertise spans the entire lifecycle of pneumatic transport systems, from initial project consultation to final commissioning and after-sales support.
The long-distance pneumatic fertilizer transport system developed by HeadPowder incorporates several key features that enhance its performance and reliability. One of the primary advantages is the ability to transport bulk fertilizers over significant distances without the need for intermediate storage or manual handling. This is achieved through a combination of high-pressure air systems, specialized ductwork, and efficient material separation mechanisms. The system is designed to handle various types of fertilizers, including nitrogen-based, phosphorus-based, and potassium-based products, ensuring compatibility with a wide range of agricultural needs.
Another critical feature is the system’s ability to maintain consistent material flow rates and pressure levels, which minimizes product degradation and reduces the risk of blockages or system failures. Advanced control systems are integrated into the design, allowing for real-time monitoring and adjustment of operational parameters. This ensures that the system operates within optimal conditions, maximizing throughput while maintaining energy efficiency. The use of high-quality materials, such as stainless steel and corrosion-resistant components, further enhances the system’s durability and longevity, reducing maintenance costs over time.
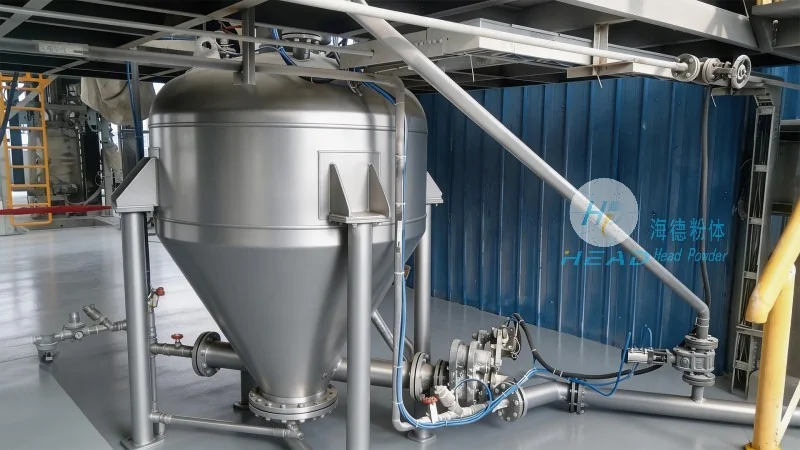
HeadPowder’s long-distance pneumatic fertilizer transport system is engineered to meet stringent industry standards for efficiency and reliability. The system typically operates at pressures ranging from 0.5 to 1.5 bar, depending on the distance and material characteristics. The conveying velocity is optimized to prevent material degradation and ensure smooth flow through the ductwork. The system’s capacity can range from several tons per hour to over 100 tons per hour, depending on the specific application requirements. This flexibility allows the system to be customized for both small-scale farm operations and large-scale industrial fertilizer plants.
The system’s design incorporates features such as air filtration and dust collection to maintain a clean and safe working environment. This is particularly important in agricultural settings where dust can affect both equipment performance and worker health. The integration of automated controls and sensors enables proactive maintenance and reduces downtime, ensuring continuous operation. Additionally, the system is designed for easy integration with existing infrastructure, minimizing the need for major modifications to existing facilities.
The long-distance pneumatic fertilizer transport system is widely used in various agricultural and industrial applications. In farming operations, it allows for the efficient distribution of fertilizers from central storage to multiple fields, reducing transportation costs and time. This is especially beneficial for large-scale farms where traditional trucking methods may be inefficient or impractical. The system also supports the integration of fertilizers into precision agriculture practices, enabling targeted application based on soil and crop needs.
For industrial fertilizer plants, the system facilitates the movement of raw materials and finished products between processing stages, improving overall production efficiency. The ability to handle bulk materials over long distances reduces the need for multiple handling steps, which can increase operational costs and introduce points of failure. The system’s reliability and low maintenance requirements contribute to significant cost savings over its operational life.
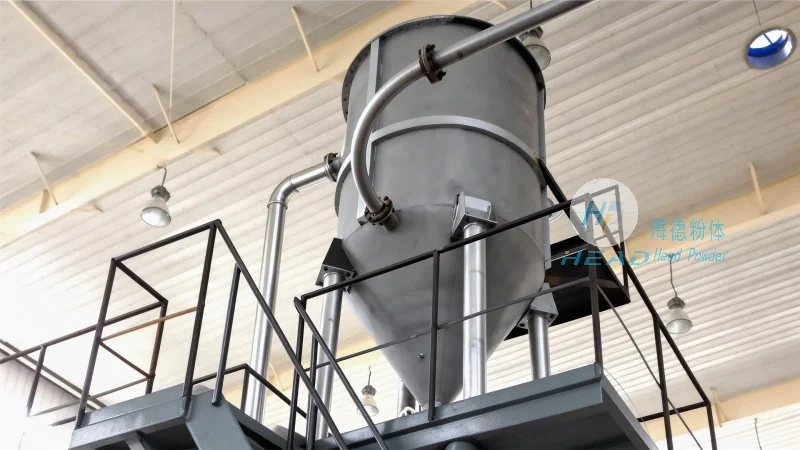
HeadPowder provides comprehensive support for the installation and commissioning of its long-distance pneumatic fertilizer transport systems. The process begins with a detailed site assessment to determine the optimal layout and system configuration. This includes evaluating the distance between the fertilizer source and application point, the type of fertilizer being transported, and any existing infrastructure that may need to be integrated. The company’s engineering team works closely with clients to develop a customized solution that meets all operational and safety requirements.
During installation, HeadPowder’s experienced technicians ensure that all components are properly assembled and aligned. The system is then tested under various conditions to verify its performance and identify any potential issues. This includes pressure testing, flow rate verification, and material handling trials. Once the system has been successfully commissioned, the company provides training to the client’s staff on operation and maintenance procedures. This ensures that the system is used effectively and maintained properly to maximize its lifespan and performance.
HeadPowder’s long-distance pneumatic fertilizer transport system represents a cutting-edge solution for the efficient and reliable handling of bulk fertilizers. By leveraging advanced pneumatic conveying technology and a commitment to quality, the system addresses the challenges of long-distance material transport in agricultural and industrial settings. With its robust design, flexible capacity, and comprehensive support, the system offers significant benefits to clients seeking to improve operational efficiency and reduce costs. As a trusted provider of engineering solutions, HeadPowder continues to innovate and deliver high-performance systems that meet the evolving needs of the fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top