Understanding the working principle and features of dust-free metering material conveying systems is crucial for industries that require precise and contamination-free material handling. This article provides an in-depth look at how these systems operate and the key characteristics that make them effective in various applications.
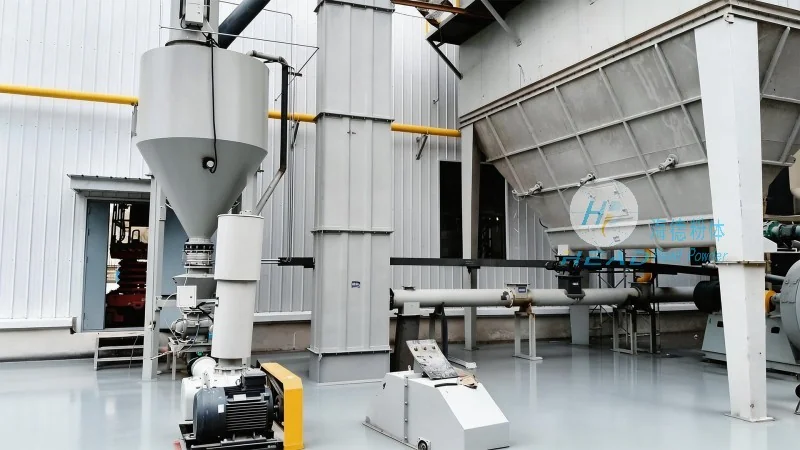
Dust-free metering material conveying systems are designed to transport powders, granules, and other bulk materials with minimal risk of contamination and loss. These systems are widely used in pharmaceutical, food, chemical, and other industries where product purity is paramount. The core of such systems lies in their ability to measure and control the flow of materials accurately while maintaining a clean environment.
The working principle of dust-free metering material conveying typically involves several key components working in tandem. The system starts with a hopper or storage container that holds the material. From there, the material is fed into a metering device, such as a rotary valve or a gravimetric feeder, which measures the exact amount of material to be conveyed. The metering device then controls the flow rate, ensuring consistent and precise delivery. The material is then transported through a sealed conveyor system, often using pneumatic or mechanical means, to the discharge point. The entire process is enclosed to prevent dust from escaping and to maintain a controlled environment.
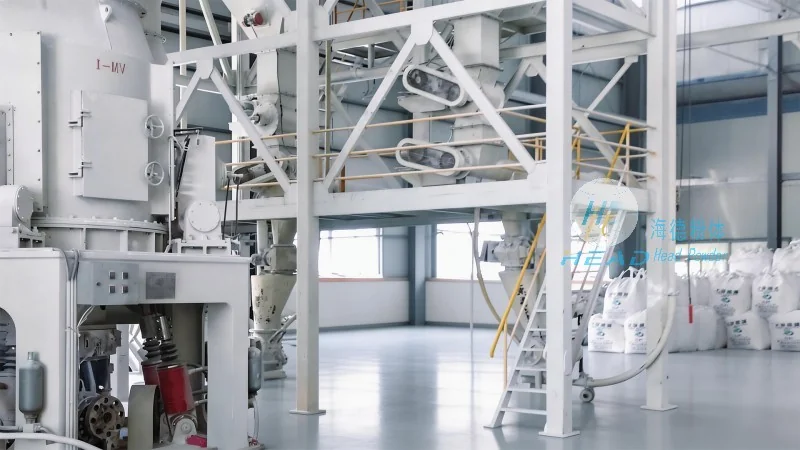
Several features distinguish effective dust-free metering material conveying systems. First, the system is fully enclosed, which prevents dust from contaminating the material or the surrounding environment. This is achieved through airtight seals and proper ventilation systems that maintain a controlled pressure within the system. Second, the metering mechanism is highly accurate, allowing for precise control over the material flow rate. This is critical for applications where exact dosing is required, such as in pharmaceutical manufacturing or food processing. Third, the system is designed for easy cleaning and maintenance, ensuring that it can be kept in optimal condition without disrupting production. Fourth, the materials used in the construction of the system are often corrosion-resistant and easy to clean, such as stainless steel, to withstand the demands of various industrial environments.
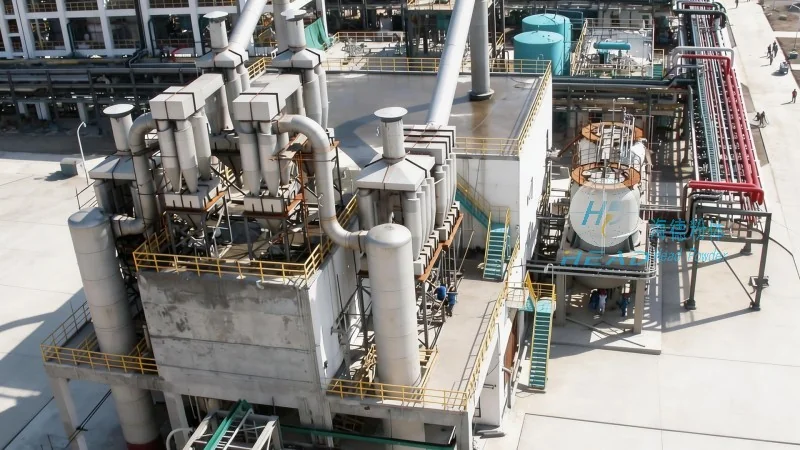
Dust-free metering material conveying systems are used in a wide range of applications across different industries. In the pharmaceutical industry, they are essential for handling active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the final product is free from contamination. In the food industry, they are used to convey ingredients like flour, sugar, and spices, maintaining the quality and safety of the end product. In the chemical industry, they are used to handle various powders and granules, preventing dust explosions and ensuring safe handling. The benefits of these systems include improved product quality, reduced waste, and increased efficiency in material handling processes.
In conclusion, dust-free metering material conveying systems are sophisticated and effective solutions for industries that require precise and contamination-free material handling. By understanding their working principles and key features, businesses can make informed decisions about implementing these systems to improve their operations. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., which specializes in such systems, industries can achieve higher levels of efficiency and product quality in their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top