Hematite, a common iron oxide with the chemical formula Fe₂O₃, is widely used in various industrial applications such as pigments, ceramics, and steel production. The efficient handling and transportation of hematite materials are critical for maintaining production efficiency and ensuring product quality. This article explores the working principles and key features of hematite material conveying systems, highlighting the technological advancements and operational advantages offered by modern solutions.
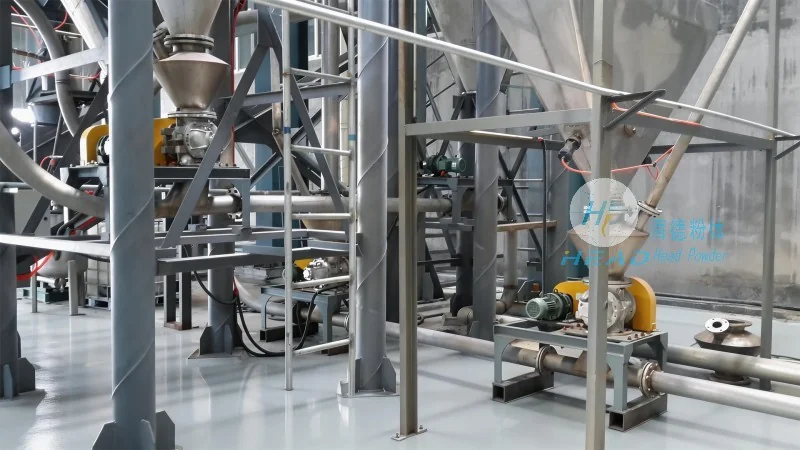
The core working principle of hematite material conveying involves the use of specialized equipment designed to transport bulk materials like hematite over long distances or within processing facilities. The process typically begins with material storage, where hematite is stored in bulk storage silos or hoppers. From there, the material is fed into the conveying system through feeders or chutes, which control the flow rate and ensure consistent material delivery.
Conveying systems for hematite often utilize mechanisms such as belt conveyors, screw conveyors, or pneumatic conveying systems. Belt conveyors are widely used due to their high load capacity and ability to handle abrasive materials like hematite without significant wear. Screw conveyors, on the other hand, are ideal for vertical or inclined transport, providing a compact solution for material elevation. Pneumatic conveying systems use air pressure to transport fine hematite powders, offering a dust-free and flexible conveying method.
Once the material is conveyed to the processing or storage location, it may undergo further handling steps such as screening, crushing, or blending. The conveying system must ensure that the material is transported without degradation, maintaining its physical properties and preventing contamination. This requires careful consideration of the material's characteristics, including its particle size, moisture content, and abrasiveness, to select the most appropriate conveying equipment and operational parameters.
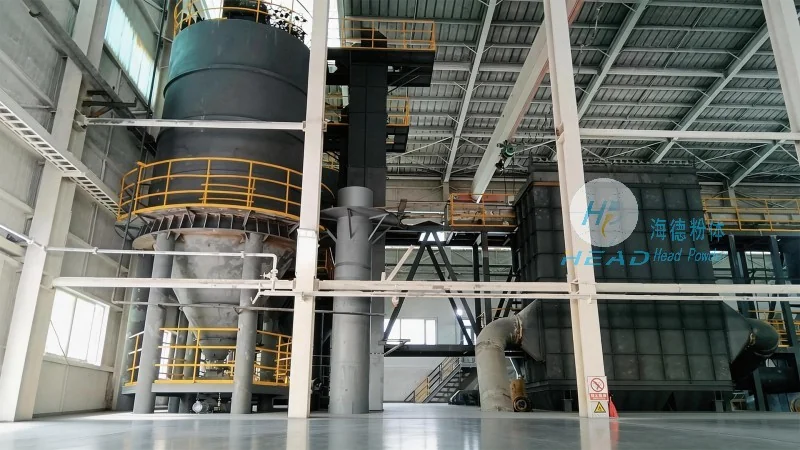
Modern hematite material conveying systems are characterized by several key features that enhance operational efficiency and product quality. One of the primary features is the ability to handle abrasive materials without excessive wear on the conveying components. This is achieved through the use of high-quality materials for conveyor belts, idlers, and other parts, ensuring long service life and reduced maintenance costs.
Another important feature is the integration of advanced control systems that allow for precise control of material flow rates, pressure, and temperature. These systems enable real-time monitoring and adjustment, ensuring consistent material delivery and preventing overloading or underloading of the conveying equipment. Additionally, many modern systems incorporate safety features such as emergency stop mechanisms, overload protection, and dust suppression systems to enhance workplace safety.
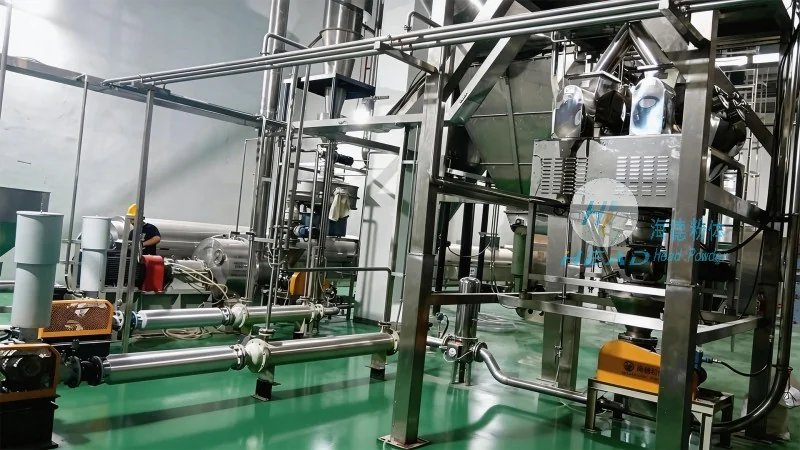
Efficiency and energy savings are also significant features of contemporary hematite conveying solutions. Advanced designs, such as variable speed drives and optimized conveyor geometry, reduce energy consumption while maintaining high throughput. This not only lowers operational costs but also aligns with sustainability goals by minimizing environmental impact. Furthermore, the use of automated feeding and conveying systems reduces the need for manual labor, improving operational safety and productivity.
Customization and adaptability are other notable features of hematite material conveying systems. Manufacturers like Shandong HeadPowder Engineering Co., Ltd. offer tailored solutions that can be adapted to specific production requirements, including different material types, processing capacities, and facility layouts. This flexibility allows industries to optimize their material handling processes and integrate conveying systems seamlessly into existing operations.
In summary, hematite material conveying systems play a vital role in the efficient and safe handling of iron oxide materials. The working principles, which involve specialized equipment and controlled material flow, combined with key features like durability, advanced control, and energy efficiency, make these systems essential for modern industrial applications. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can enhance their material handling capabilities, improve production efficiency, and ensure compliance with safety and environmental standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top