At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and implementation of efficient peanut powder conveying systems. Understanding the working principles and key features of these systems is crucial for optimizing material handling processes in various industrial applications. This article provides a detailed overview of how peanut powder conveying works and the distinctive characteristics that make such systems effective.
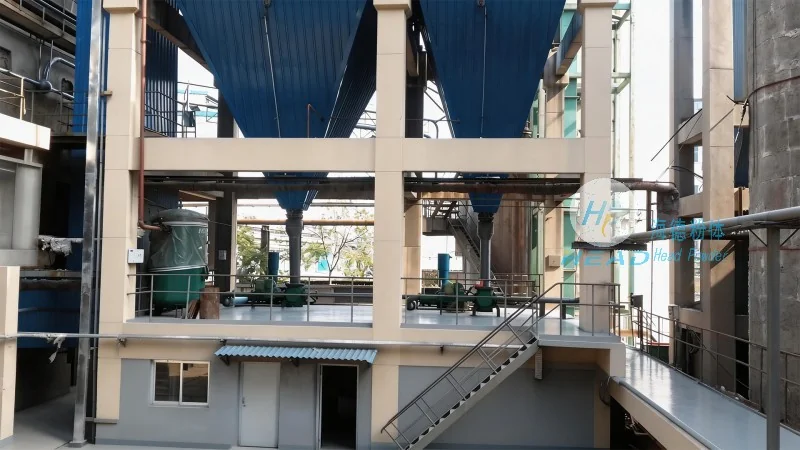
Peanut powder conveying systems operate on the principle of utilizing mechanical or pneumatic forces to transport granular or powdered materials, such as peanut flour or other similar products, from one location to another. The primary goal is to achieve a reliable, continuous, and efficient transfer of the material while minimizing product degradation, contamination, and energy consumption. The working principle typically involves a combination of components, including feeders, conveyors, and control mechanisms, all working in harmony to ensure smooth material flow.
One common method employed in peanut powder conveying is the use of screw conveyors or auger systems. These devices consist of a rotating helical screw that moves the powder along a tube or trough. As the screw rotates, it pushes the material forward, creating a positive displacement that ensures consistent flow. This mechanism is particularly effective for handling fine powders like peanut flour, as it prevents clogging and maintains a steady transfer rate. Additionally, pneumatic conveying systems may be used, where compressed air is employed to transport the powder through a pipeline. This approach is advantageous for longer distances or when dealing with more delicate powders, as it reduces the risk of mechanical stress on the material.
Modern peanut powder conveying systems from HeadPowder are characterized by several key features that enhance performance and reliability. These features are designed to address common challenges in material handling, such as dust control, product quality preservation, and operational efficiency. The first notable feature is the integration of advanced control systems. These systems allow for real-time monitoring of the conveying process, enabling operators to adjust parameters like speed, pressure, or feed rate as needed. This adaptability ensures that the system can handle varying production volumes and material characteristics without compromising performance.
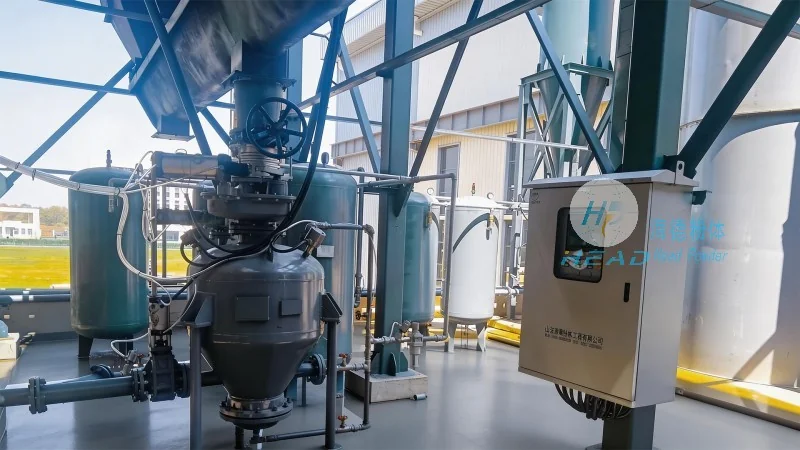
Another critical feature is the emphasis on dust suppression and containment. Peanut powders are often fine and can generate significant dust during handling, which poses health and safety risks as well as environmental concerns. Advanced conveying systems incorporate dust collection and filtration components, such as cyclones or bag filters, to capture and remove airborne particles. This not only protects the environment but also maintains a clean and safe working environment for personnel. Furthermore, the use of sealed and enclosed conveyor designs minimizes the exposure of the material to external contaminants, preserving the quality and purity of the peanut powder.
Efficiency and energy conservation are also prominent features of contemporary peanut powder conveying solutions. Many systems utilize energy-efficient motors and variable speed drives, which adjust the power consumption based on the actual conveying requirements. This reduces unnecessary energy waste and lowers operational costs over time. Additionally, the design of the conveyor components, such as smooth surfaces and minimal friction, contributes to lower energy usage while maintaining high transfer rates. By optimizing these aspects, the systems achieve a balance between performance and sustainability.
The adoption of peanut powder conveying systems offers numerous benefits for businesses involved in the processing and handling of peanut products. One of the most significant advantages is the improvement in operational efficiency. By automating the material transfer process, companies can reduce labor costs and minimize downtime associated with manual handling. The consistent and reliable flow of peanut powder ensures that production lines operate smoothly, leading to higher throughput and increased productivity. This efficiency is particularly valuable in high-volume processing facilities where continuous operation is essential.
Another key benefit is the preservation of product quality. Peanut powders are sensitive to moisture, temperature, and physical stress, which can affect their flavor, texture, and shelf life. Advanced conveying systems are designed to minimize these factors, ensuring that the powder remains in optimal condition throughout the transfer process. The use of gentle handling mechanisms, such as pneumatic conveying or low-speed screw conveyors, reduces the risk of particle breakage or agglomeration, maintaining the integrity of the product. This is crucial for maintaining customer satisfaction and meeting quality standards in the food industry.
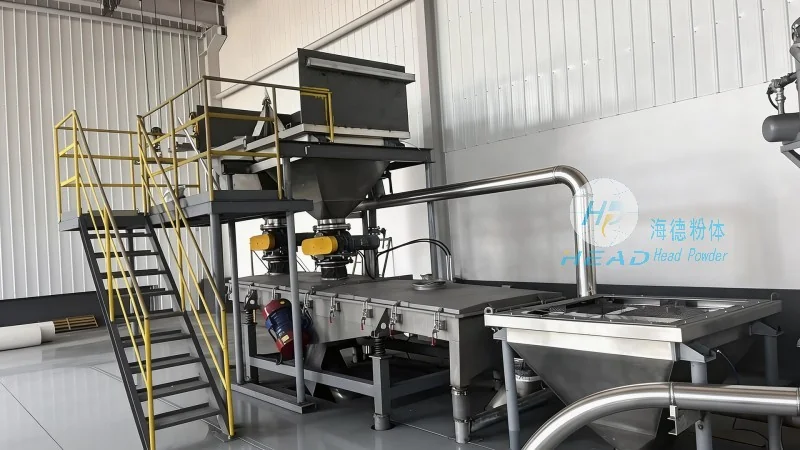
Cost-effectiveness is also a major advantage of implementing these systems. While the initial investment may be significant, the long-term savings in labor, energy, and material waste often outweigh the costs. The reduction in product loss due to spillage or contamination, combined with lower maintenance requirements for efficient systems, contributes to overall cost savings. Additionally, the ability to scale the system according to production needs allows businesses to adapt to changing market demands without incurring excessive expenses.
In conclusion, peanut powder conveying systems are essential for optimizing the handling of peanut-based products in industrial settings. The working principles, which may involve mechanical or pneumatic methods, are tailored to the specific characteristics of the material, ensuring efficient and reliable transfer. The key features of modern systems, including advanced controls, dust suppression, and energy efficiency, address common challenges and enhance overall performance. The benefits, such as improved efficiency, product quality preservation, and cost-effectiveness, make these systems a valuable investment for businesses in the food processing industry.
Shandong HeadPowder Engineering Co., Ltd. specializes in providing tailored conveying solutions that meet the unique needs of our clients. With our expertise in designing and manufacturing high-quality peanut powder conveying systems, we help businesses streamline their operations and achieve their production goals. Our commitment to innovation and quality ensures that our systems are reliable, efficient, and sustainable, supporting the success of our clients in the competitive market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top