HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of efficient systems for transporting dust collector ash. This article explores the fundamental working principles and key characteristics of such systems, offering insights into their operational efficiency and practical applications.
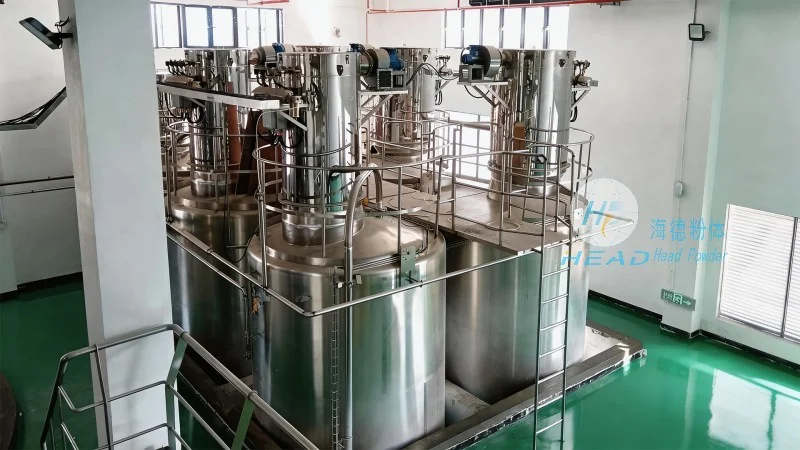
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With a focus on delivering reliable and innovative solutions for material handling, the company has established itself as a trusted partner in the industrial sector. Their expertise lies in developing systems that ensure safe, efficient, and cost-effective transportation of bulk materials, including dust collector ash, which is a critical byproduct in many industrial processes.
The process of transporting dust collector ash typically involves several key components and steps. At the core of the system is the dust collector, which captures fine particles from industrial processes such as combustion, manufacturing, or chemical reactions. Once collected, the ash is transferred to a storage or processing unit, where it is then conveyed to its final destination—often a disposal site or a recycling facility.
The conveying mechanism can vary depending on the specific application and material properties. Common methods include pneumatic conveying, where air pressure is used to move the ash through pipes; mechanical conveying, such as screw conveyors or belt conveyors, which rely on mechanical components to transport the material; and hydraulic systems, which use fluid pressure to move the ash. Each method has its advantages and is selected based on factors like material size, moisture content, and the distance to be covered.
In pneumatic conveying, for example, the ash is introduced into a pipeline and carried by a stream of air. This method is particularly effective for fine, dry materials and can handle long distances with minimal maintenance. Mechanical conveyors, on the other hand, are often preferred for bulkier or wetter ash, as they can handle higher volumes and are more resistant to clogging. The choice of conveying method directly impacts the system's efficiency, energy consumption, and overall operational costs.
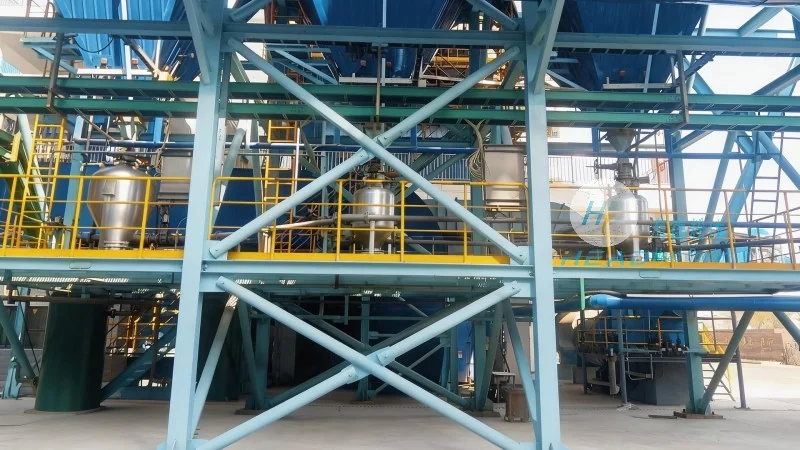
Efficient dust collector ash material conveying systems exhibit several distinct characteristics that contribute to their effectiveness. One of the primary characteristics is their ability to handle a wide range of material types and sizes. Dust collector ash can vary significantly in terms of particle size, moisture content, and bulk density, and a good conveying system must be adaptable to these variations to ensure consistent performance.
Another important characteristic is the system's reliability and durability. Industrial environments are often harsh, with high temperatures, corrosive substances, and abrasive materials. The conveying equipment must be constructed from materials that can withstand these conditions without degradation. For instance, stainless steel or specialized alloys may be used for components that come into direct contact with the ash, ensuring longevity and preventing contamination.
Energy efficiency is also a critical characteristic. Modern conveying systems are designed to minimize energy consumption while maintaining high throughput. This is achieved through optimized airflow in pneumatic systems, efficient drive mechanisms in mechanical conveyors, and smart control systems that adjust operation based on real-time conditions. By reducing energy use, these systems not only lower operational costs but also contribute to environmental sustainability.
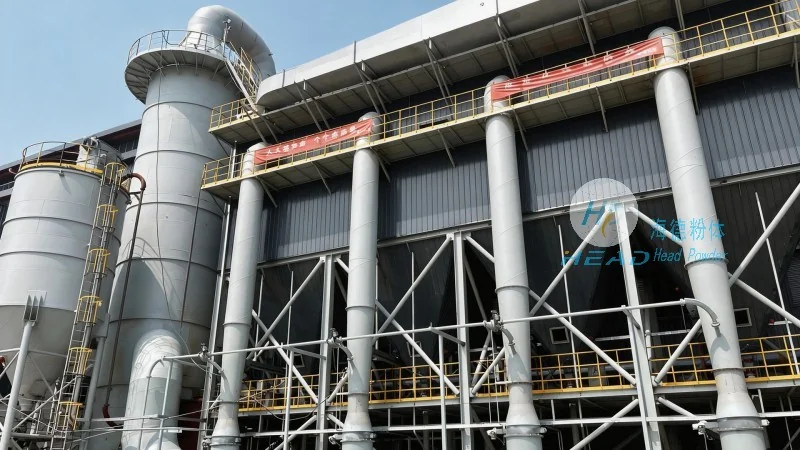
Furthermore, the systems must ensure safety and compliance with regulatory standards. Dust collector ash often contains hazardous components, and the conveying process must prevent dust emissions, leaks, or other safety hazards. Advanced sealing technologies and enclosed systems are employed to maintain a safe working environment. Additionally, compliance with local and international regulations regarding waste management and emissions is essential, making the system's design and operation a critical consideration.
The effective transportation of dust collector ash offers numerous operational benefits for industrial facilities. By streamlining the process of ash removal and disposal, companies can improve overall plant efficiency and reduce downtime associated with manual handling. Automated conveying systems also enhance safety by minimizing the need for workers to handle heavy or potentially hazardous materials.
These systems are widely used in various industries, including power generation, cement production, and chemical manufacturing. In power plants, for example, the ash generated from coal combustion is a significant byproduct, and efficient conveying systems are essential for managing this waste and ensuring compliance with environmental regulations. Similarly, in cement plants, the ash from the kiln process is often used as a raw material in the production of cement, and reliable conveying systems facilitate its transport to the mixing and processing areas.
Moreover, the use of advanced conveying technologies allows for better integration with other industrial processes. For instance, the ash can be directly fed into a recycling system or a waste-to-energy plant, reducing the overall environmental impact of the industrial operation. This integration not only improves efficiency but also aligns with the growing trend of sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top