Stone powder conveying systems play a pivotal role in the industrial processing of fine stone powders, which are widely used in construction, manufacturing, and chemical industries. These systems are engineered to efficiently transport stone powders from storage silos or processing units to downstream equipment such as mixers, reactors, or packaging machines. The primary goal of these systems is to maintain the quality and integrity of the stone powder, which can be sensitive to moisture, agglomeration, and contamination during transportation. To achieve this, the equipment must be designed to handle the unique physical properties of stone powders, including their fine particle size, high density, and potential for dust generation.
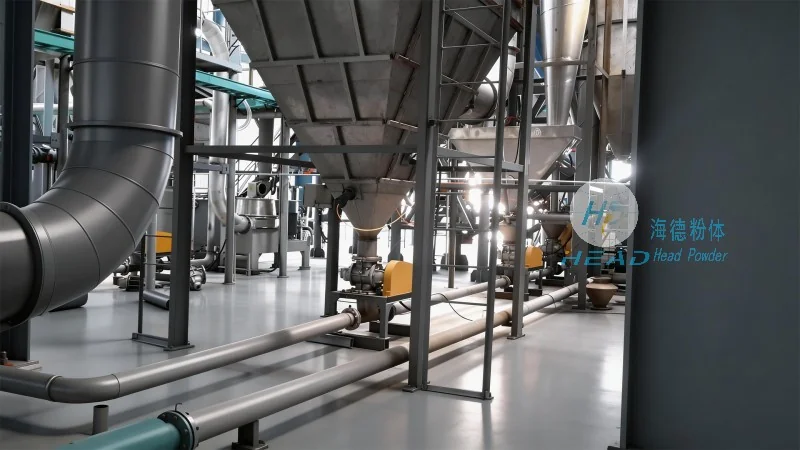
The fundamental working principle of stone powder conveying systems revolves around the movement of material through a sealed pipeline. There are two main categories of conveying mechanisms: positive displacement and pneumatic. Positive displacement conveyors, such as rotary lobe blowers or rotary airlocks, operate by creating a continuous flow of material through a rotating mechanism. This method is particularly effective for handling high-density and abrasive stone powders, as it provides consistent and reliable delivery rates. The rotary lobe blower, for example, uses two lobed rotors to push material forward, while maintaining a sealed environment that prevents dust leakage. Pneumatic conveyors, on the other hand, utilize compressed air to either push or pull the material through the pipeline. This approach is ideal for materials that are more delicate or require a dust-free environment, as the air flow can be controlled to minimize particle breakage. The selection of a specific conveying method depends on factors like the material's characteristics, the distance to be conveyed, and the required system capacity.
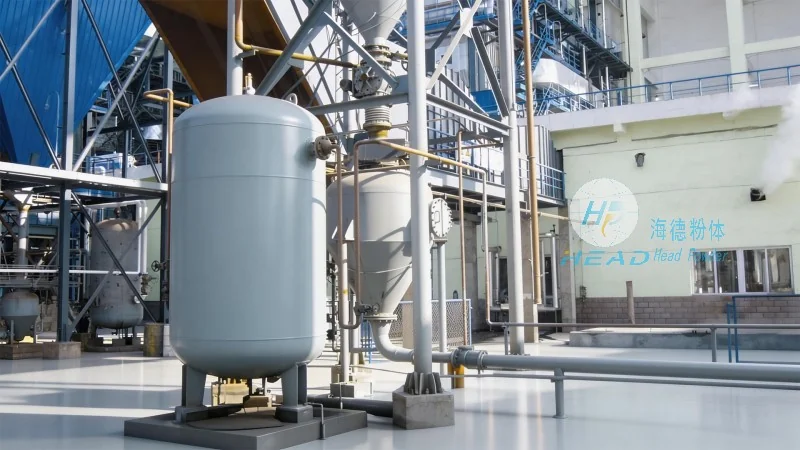
Modern stone powder conveying systems are equipped with several advanced features that enhance their performance, safety, and efficiency. One critical feature is the integration of dust control and filtration systems. These systems are essential for maintaining a safe working environment and complying with environmental regulations. The equipment typically includes cyclones or bag filters that capture and recycle fine particles, reducing airborne dust and preventing contamination of the surrounding area. Another important feature is the ability to adjust conveying rates dynamically. This allows operators to match the system's output to the production schedule, optimizing energy usage and preventing material buildup in the pipeline. Additionally, many systems incorporate monitoring and control systems that provide real-time data on flow rates, pressure, and temperature. This data helps in troubleshooting and maintaining the equipment in optimal condition, thereby reducing downtime and increasing overall productivity.
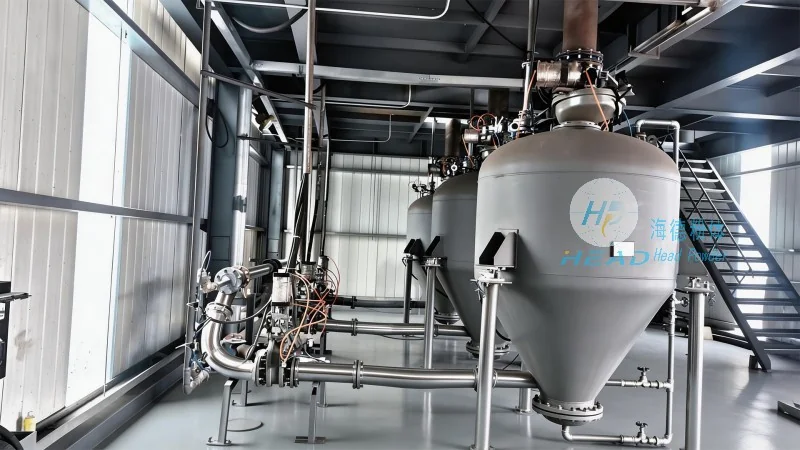
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a prominent manufacturer specializing in the design and production of stone powder conveying systems. The company is headquartered in Shandong, China, and has established itself as a leading provider of industrial conveying solutions. With a strong commitment to innovation and quality, headpowder has developed a comprehensive range of equipment tailored to the diverse needs of the stone processing industry. The company's products are designed to handle various types of stone powders, including limestone, granite, and quartz, and are suitable for applications in construction, mining, and chemical processing. By leveraging advanced engineering and manufacturing techniques, headpowder ensures that its conveying systems are efficient, durable, and cost-effective for its clients. The company also emphasizes customer support, providing technical assistance and maintenance services to ensure the long-term performance of its equipment.
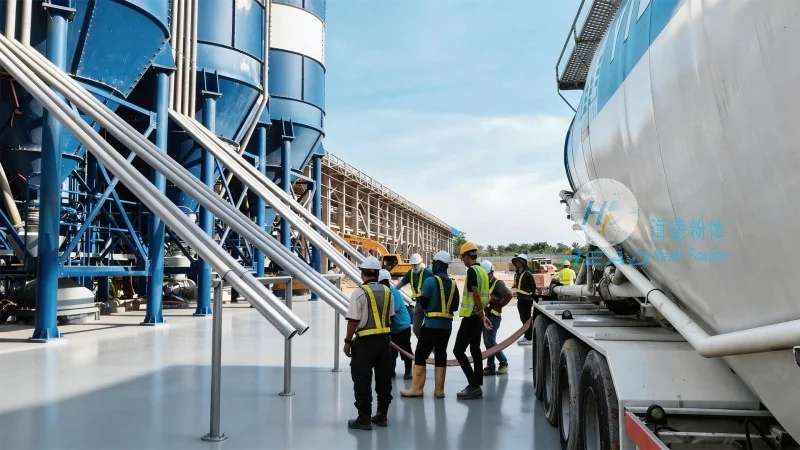
The conveying equipment from headpowder is distinguished by several technical advantages that enhance its performance and reliability. One key advantage is the use of high-quality, corrosion-resistant materials in construction. The components are made from stainless steel and special alloys, which are essential for handling abrasive and high-density stone powders. This not only extends the equipment's service life but also reduces maintenance costs over time. Another advantage is the advanced control systems integrated into the equipment. These systems allow for precise control over conveying parameters, ensuring consistent material flow and minimizing the risk of system failures. Furthermore, headpowder's systems are designed with energy efficiency in mind. By optimizing the air flow and pressure, the equipment operates at lower energy consumption levels, contributing to significant cost savings for the end-user. The company also prioritizes user-friendly operation, with intuitive controls and clear indicators that make it easy for operators to monitor and manage the system. Additionally, headpowder's equipment is designed for easy maintenance, with accessible components and modular designs that simplify repairs and replacements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top