Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, specializes in the development and supply of advanced river sand powder conveying system equipment. This article delves into the operational principles and distinctive features of such systems, illustrating how they effectively manage the transport of river sand in industrial settings.
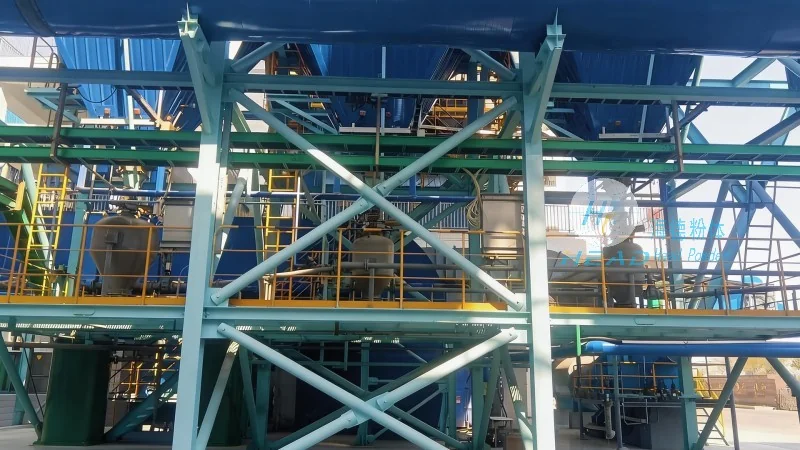
River sand, a critical raw material in construction, mining, and manufacturing, presents unique handling challenges due to its granular structure and variable moisture content. The river sand powder conveying system is engineered to address these challenges by providing a reliable, efficient method for transporting sand from storage facilities to processing units or end-use applications. The system typically comprises several key components, including feeders, conveyors, control panels, and dust management units, all integrated to ensure seamless operation and minimal material loss.
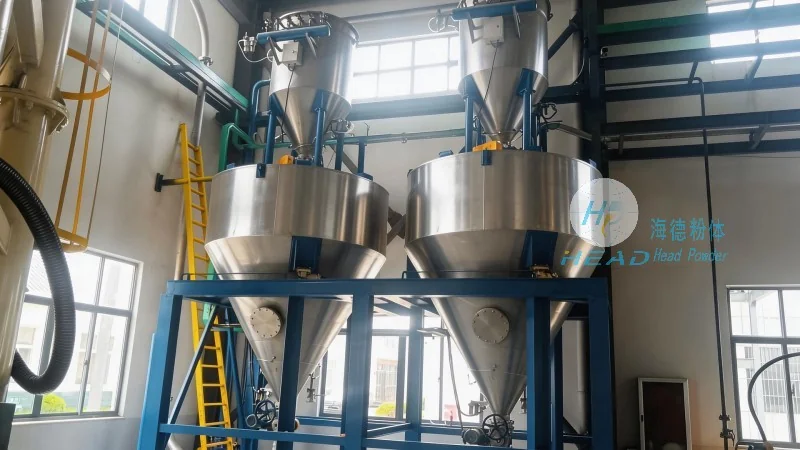
The fundamental working principle of the river sand powder conveying system centers on the method of material movement. Most systems employ a hybrid approach combining mechanical and pneumatic technologies to optimize performance. For example, a common configuration starts with a screw or belt conveyor for initial transport, followed by a pneumatic conveying section for longer distances or complex routing. The process initiates with sand being fed into the system via a hopper or feeder, which regulates flow to maintain consistent pressure and prevent blockages. The material then travels through a network of pipes or ducts, either carried by air (in pneumatic systems) or moved by rotating blades (in mechanical systems). Integrated control valves and pressure sensors monitor and adjust the flow, ensuring the system operates within optimal parameters. The final stage involves discharging the sand into the target container or processing equipment, with dust collection systems in place to manage airborne particles and maintain environmental compliance.
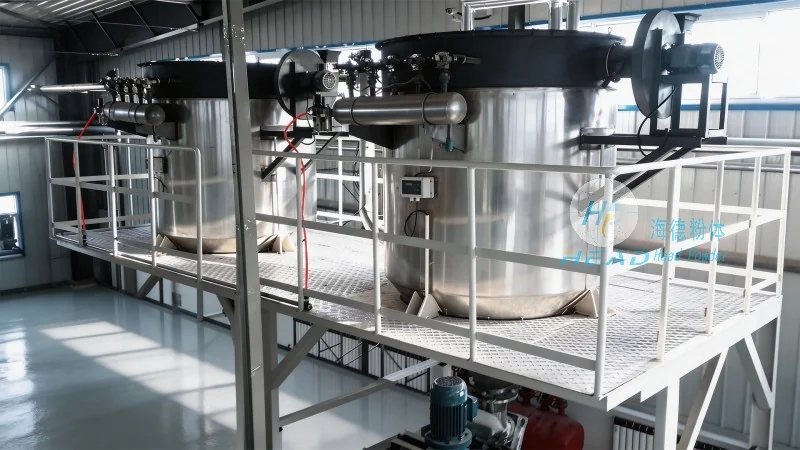
The river sand powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is distinguished by several key features that enhance its performance and usability. Firstly, the system is designed for high efficiency, capable of handling large volumes of river sand with minimal energy consumption. Advanced control systems enable precise regulation of flow rates and pressure, reducing operational costs and improving productivity. Secondly, the equipment is built for durability and reliability, utilizing corrosion-resistant materials to withstand the abrasive nature of river sand and potential moisture exposure. This robust construction ensures long-term operation with low maintenance requirements. Thirdly, the system offers flexibility in layout and integration, accommodating various site configurations and existing infrastructure. It can be customized to meet specific operational needs, including different conveying distances, material types, and environmental standards. Additionally, the system incorporates safety features such as overload protection and emergency stop mechanisms, ensuring safe operation in industrial environments. The dust collection and filtration systems not only improve air quality but also help maintain the quality of the conveyed sand by preventing contamination from external particles. Overall, these features make the system an ideal solution for industries requiring efficient, reliable, and environmentally friendly handling of river sand.
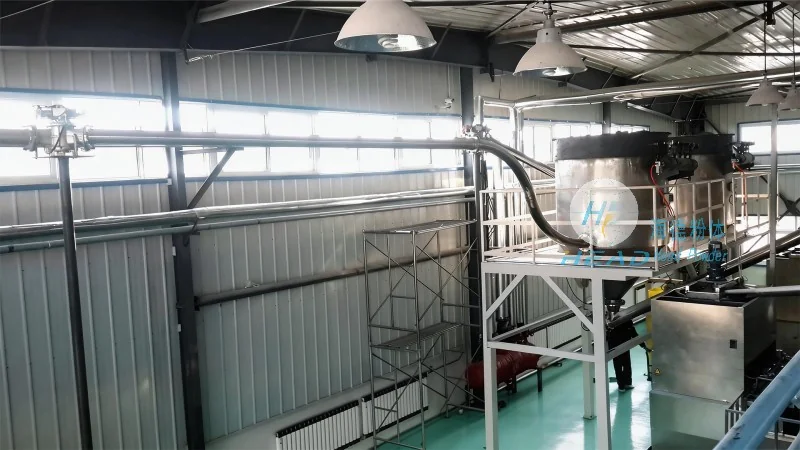
The river sand powder conveying system is widely applicable across multiple industrial sectors, including construction, mining, and manufacturing. In construction, it is used to transport sand from stockpiles to concrete mixing plants or brick-making facilities, ensuring a steady supply of raw material for production. In mining operations, the system aids in the transport of sand from extraction sites to processing units, facilitating the separation and purification of valuable minerals. The benefits of using this system extend beyond material transport; it also enhances workplace safety by reducing manual handling of heavy or dusty materials. Automated control systems minimize human intervention, lowering accident risks and improving operational consistency. Furthermore, the system's ability to handle varying moisture levels in river sand makes it suitable for regions with fluctuating climatic conditions, ensuring consistent performance regardless of environmental factors. The integrated dust collection systems also contribute to environmental sustainability by minimizing air pollution and complying with regulatory standards. In summary, the river sand powder conveying system from Shandong HeadPowder Engineering Co., Ltd. provides a comprehensive solution for efficient and reliable sand handling, supporting industrial operations with high performance and durability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top