HeadPowder, a leading provider of industrial conveying solutions, specializes in the efficient handling of inorganic salts through pneumatic conveying systems. This article explores the fundamental working principles, various classifications, and practical applications of inorganic salt pneumatic conveying, offering insights into how these systems enhance material transport in industrial settings.
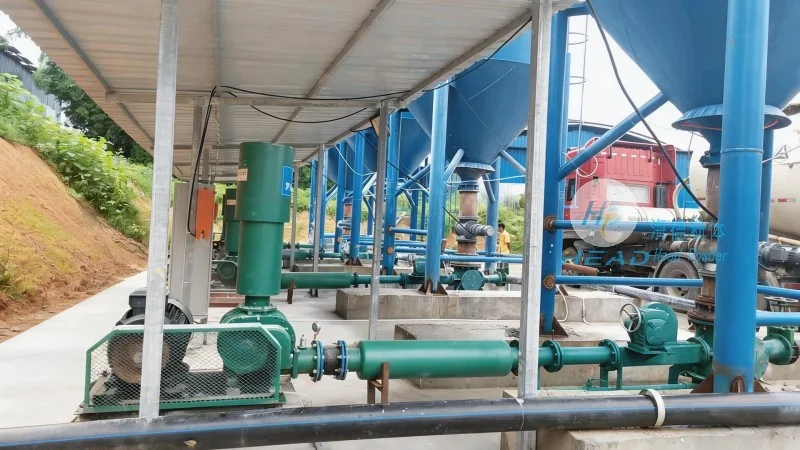
Pneumatic conveying is a method of transporting bulk materials, such as inorganic salts, using a stream of pressurized air or gas. The process involves creating a flow of air that carries the solid particles through a pipeline. This technique is widely adopted in industries dealing with dry, free-flowing materials like salts due to its ability to handle delicate or abrasive substances without causing damage. The core principle revolves around the interaction between the air and the solid particles, where the air's kinetic energy propels the material forward. Key factors influencing the efficiency of this system include air velocity, particle size, and the design of the conveying line.
The operation of an inorganic salt pneumatic conveying system typically follows a sequence of steps. First, the inorganic salt is introduced into a hopper or feeder, where it is fed into the conveying line. Simultaneously, a fan or blower generates the necessary air pressure to create the conveying stream. The air and salt particles mix in the pipeline, forming a dense or dilute phase depending on the system design. As the mixture travels through the line, it may encounter bends, filters, or cyclones to separate the air from the material. The final stage involves depositing the inorganic salt into a receiving container or storage silo. This continuous process ensures a reliable and controlled transport of the material from the source to the destination.
Pneumatic conveying systems for inorganic salts are categorized based on the pressure of the air used and the direction of material flow. The primary classifications include:
Suction systems operate under negative pressure, drawing the inorganic salt from a source using a vacuum pump. This method is ideal for applications where the material needs to be collected from a distance or from a low-level source. The system typically consists of a vacuum source, a conveying line, and a collection hopper. The air flow is directed towards the material, creating a suction effect that pulls the particles into the line. Suction systems are particularly useful for handling fine powders or when the material is located in an area that is difficult to access with positive pressure systems.
Positive pressure systems use a blower or compressor to generate high-pressure air that pushes the inorganic salt through the conveying line. This approach is suitable for applications requiring high transport rates or when the material needs to be delivered to a higher elevation. The system includes a pressure source, a conveying line, and a discharge point. The air is forced into the line, carrying the salt particles forward. Positive pressure systems are often preferred for abrasive or corrosive materials as they can handle higher particle loads without causing wear on the equipment.
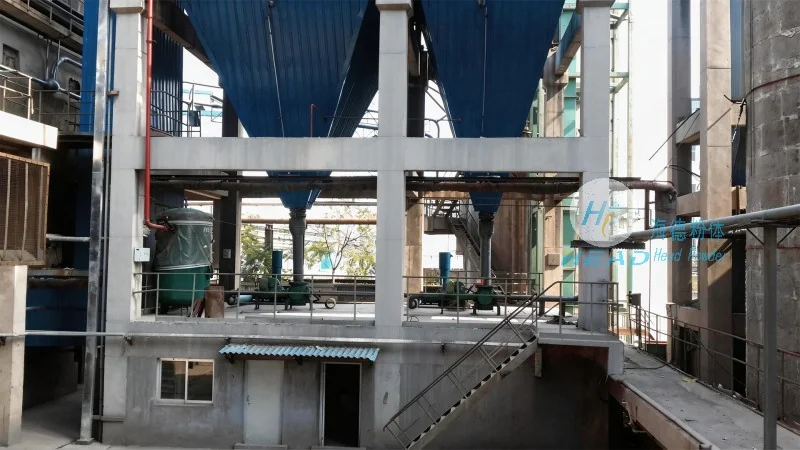
Mixed-pressure systems combine elements of both suction and positive pressure systems. They utilize a combination of vacuum and pressure to transport the inorganic salt over longer distances or through complex layouts. This hybrid approach allows for flexibility in system design, accommodating both collection and delivery requirements. Mixed-pressure systems are commonly used in large-scale industrial operations where the material needs to be transported from multiple sources to a central processing facility.
Inorganic salt pneumatic conveying is widely applied across various industries due to its versatility and efficiency. Some of the key applications include:
In the chemical and fertilizer industry, inorganic salts such as sodium chloride, potassium chloride, and calcium carbonate are commonly transported using pneumatic systems. These materials are often used as raw ingredients in the production of various chemicals and fertilizers. The conveying systems help in moving these materials from storage silos to processing units, ensuring a continuous supply of raw materials. The ability to handle large volumes and maintain material integrity makes pneumatic conveying an ideal choice for these applications.
The food and pharmaceutical sectors require strict handling of inorganic salts, such as table salt or calcium supplements. Pneumatic conveying systems are used to transport these materials without contamination or degradation. The systems are designed to maintain hygiene standards, with features like stainless steel construction and air filtration. This ensures that the inorganic salts remain pure and suitable for use in food products or pharmaceutical formulations. The gentle handling of the material also prevents caking or agglomeration, which is crucial for maintaining product quality.
In the mining industry, inorganic salts are often extracted from ores and need to be transported to processing plants. Pneumatic conveying systems are employed to move these materials over long distances, often in harsh environments. The systems are built to withstand the abrasive nature of the materials and the challenging conditions of mining sites. The ability to handle high volumes and maintain a consistent flow rate is essential for efficient mineral processing. Additionally, the systems can be integrated with other processing equipment, such as crushers and grinders, to form a complete material handling solution.
Many industrial plants, including power plants and manufacturing facilities, use inorganic salts for various processes. Pneumatic conveying systems help in transporting these materials from storage areas to the points of use, such as boilers or reactors. The systems are designed to handle different types of inorganic salts, including those with varying particle sizes and moisture content. The flexibility of pneumatic conveying allows for the adaptation of the system to meet the specific requirements of each industrial application. This ensures that the material is delivered efficiently and without interruption, contributing to the overall productivity of the plant.
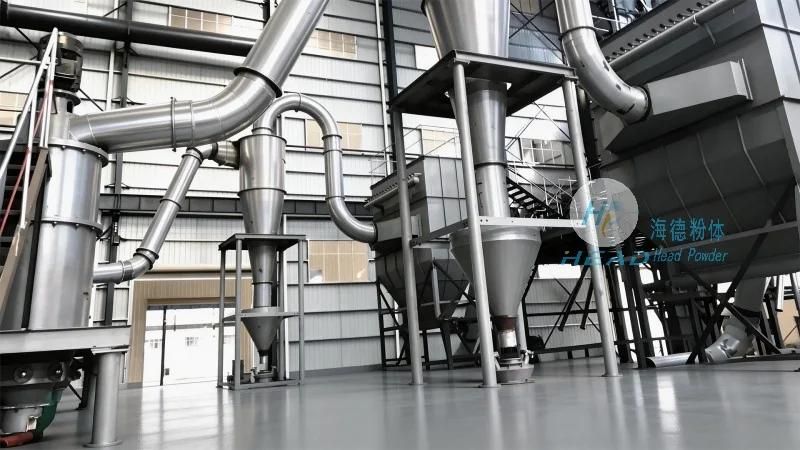
Implementing pneumatic conveying systems for inorganic salts offers several advantages over traditional methods like belt conveyors or bucket elevators. These benefits include:
Pneumatic conveying systems can be fully automated, reducing the need for manual labor in material handling. The systems can be integrated with sensors and control systems to monitor the flow rate, pressure, and material level. This automation not only reduces labor costs but also improves the safety and reliability of the operation. Workers are no longer exposed to the risks associated with handling bulk materials manually, such as dust exposure or physical strain.
The ability to transport inorganic salts over long distances and through complex layouts makes pneumatic conveying more efficient than other methods. The systems can handle high volumes of material with minimal downtime, ensuring a continuous supply of raw materials. The gentle handling of the material also reduces the risk of damage or degradation, which is crucial for maintaining product quality. This efficiency translates into higher productivity and lower operational costs for industrial facilities.
Pneumatic conveying systems are designed to minimize dust emissions and prevent material contamination. The enclosed pipeline system reduces the exposure of workers to dust and other airborne particles, improving workplace safety. Additionally, the systems can be equipped with air filtration and dust collection devices to further reduce environmental impact. This makes pneumatic conveying a more environmentally friendly option compared to open-air handling methods.
The modular design of pneumatic conveying systems allows for easy expansion or modification to accommodate changing production needs. The systems can be adapted to handle different types of inorganic salts, including those with varying particle sizes and properties. This flexibility makes pneumatic conveying a versatile solution for a wide range of industrial applications. Companies can invest in a basic system and expand it as their operations grow, without the need for significant capital investment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top