Industrial alkali gas-pneumatic conveying is a critical technology in the chemical processing industry, particularly for handling caustic materials like sodium hydroxide, calcium hydroxide, and other alkaline compounds. This method involves transporting bulk materials through a pipeline system using compressed air or other gases, offering a safe and efficient alternative to traditional mechanical conveying systems. The process is widely adopted in manufacturing facilities due to its ability to minimize material contamination, reduce labor costs, and enhance operational safety.
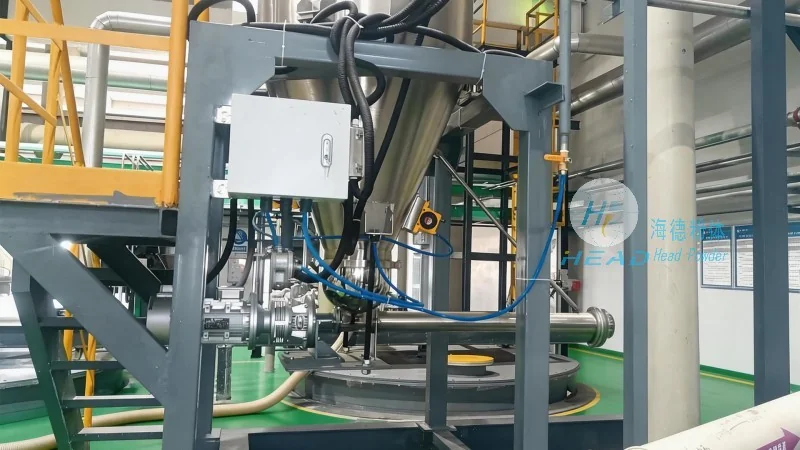
The core mechanism of gas-pneumatic conveying for industrial alkalis relies on the interaction between the material being conveyed and the air stream. In a typical system, the alkaline powder or granules are introduced into a hopper or feeder, where they are then drawn into a pipeline by the pressure differential created by the compressed air. The air acts as a carrier, suspending the particles and transporting them to the destination point, such as a storage silo, processing unit, or packaging area. The velocity of the air and the size of the particles determine the conveying capacity and efficiency of the system. Proper design of the air flow rate and pipeline dimensions is essential to ensure smooth and consistent material transport without causing excessive wear or degradation of the alkaline product.
A standard industrial alkali gas-pneumatic conveying system comprises several key components, each playing a vital role in the overall operation. The primary components include a hopper or feeder for material storage and feeding, a compressor or blower to generate the necessary air pressure, a pipeline network for material transport, and a receiver or silo for material discharge. Additionally, the system may incorporate accessories such as cyclones for separation, filters to remove air contaminants, and control valves to regulate air flow and pressure. The design of the system must consider factors like material properties (e.g., particle size, density, moisture content), conveying distance, and required throughput to ensure optimal performance. For example, in applications involving highly reactive or corrosive alkalis, the materials of construction for the hopper, feeder, and pipeline must be selected carefully to prevent chemical reactions or degradation.
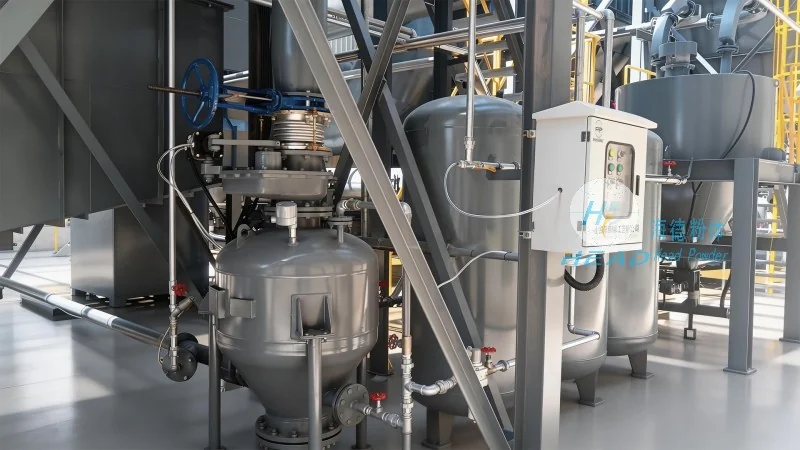
Industrial alkali gas-pneumatic conveying systems can be classified based on the mode of air flow and the method of material transport. The two main categories are pressure and vacuum systems. Pressure systems utilize compressed air to push the material through the pipeline, while vacuum systems use a vacuum to draw the material into the pipeline. Within these categories, further classifications exist based on the specific conveying method, such as dilute phase and dense phase systems. Dilute phase systems operate at higher air velocities, typically transporting particles in a suspended state, making them suitable for short to medium distances and low to medium material loads. Dense phase systems, on the other hand, operate at lower air velocities, where the material is conveyed in a slurry-like state, allowing for longer distances and higher material loads. The choice between pressure and vacuum, as well as dilute and dense phase, depends on the specific application requirements, including material characteristics, conveying distance, and system constraints.
The versatility of industrial alkali gas-pneumatic conveying makes it applicable across various industrial sectors. In the chemical industry, it is commonly used for transporting caustic soda (sodium hydroxide) and other alkaline reagents to reactors, storage tanks, or packaging lines. The food and beverage industry may employ this technology for handling alkaline ingredients like sodium bicarbonate or calcium carbonate in food processing facilities. Additionally, in the pharmaceutical sector, gas-pneumatic conveying can be utilized for transporting alkaline excipients or active pharmaceutical ingredients (APIs) with strict purity requirements. The system's ability to maintain product integrity, prevent cross-contamination, and ensure consistent material flow makes it a preferred choice in these industries. For instance, in a chemical plant producing sodium hydroxide, the gas-pneumatic conveying system efficiently transports the caustic material from the production unit to the storage silo, ensuring a continuous supply for downstream processes.
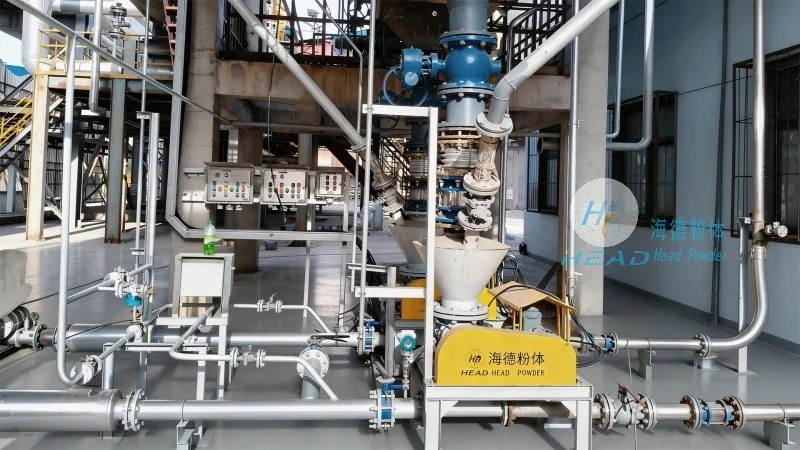
Implementing industrial alkali gas-pneumatic conveying offers several advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in material contamination, as the system is enclosed and does not involve direct contact with external elements. This is particularly important for handling caustic materials, which can be hazardous if contaminated or exposed to moisture. Additionally, the system minimizes labor costs by automating the material transport process, reducing the need for manual handling and associated risks. The enclosed nature of the system also enhances operational safety by preventing dust emissions and minimizing the risk of chemical exposure to personnel. However, there are considerations to keep in mind when designing and operating such systems. For example, the selection of appropriate air flow rates and pipeline dimensions is crucial to avoid excessive energy consumption or material degradation. Furthermore, regular maintenance of the compressor, filters, and pipeline components is necessary to ensure long-term system reliability and prevent downtime. The cost of initial system installation and maintenance should also be factored into the overall operational budget.
Industrial alkali gas-pneumatic conveying is a robust and efficient technology that plays a vital role in the handling and transport of caustic materials in various industrial applications. By understanding the working principles, system components, and classification of these systems, manufacturers can optimize their material transport processes, improve operational efficiency, and enhance safety standards. As the demand for caustic materials continues to grow in industries such as chemicals, food, and pharmaceuticals, the adoption of advanced gas-pneumatic conveying systems will remain essential for maintaining productivity and product quality. The expertise and solutions provided by companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) are instrumental in helping industrial facilities implement and maintain effective alkali conveying systems, ensuring reliable and safe material transport in line with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top