Denitrification urea transport systems play a crucial role in modern industrial processes, particularly in power plants and other facilities that employ selective catalytic reduction (SCR) technology to reduce nitrogen oxide emissions. The efficient and reliable transport of urea, a key reagent in SCR systems, is essential for maintaining optimal performance and environmental compliance. This article provides an overview of denitrification urea transport systems, focusing on the advantages and features of pneumatic conveying technology for urea delivery.
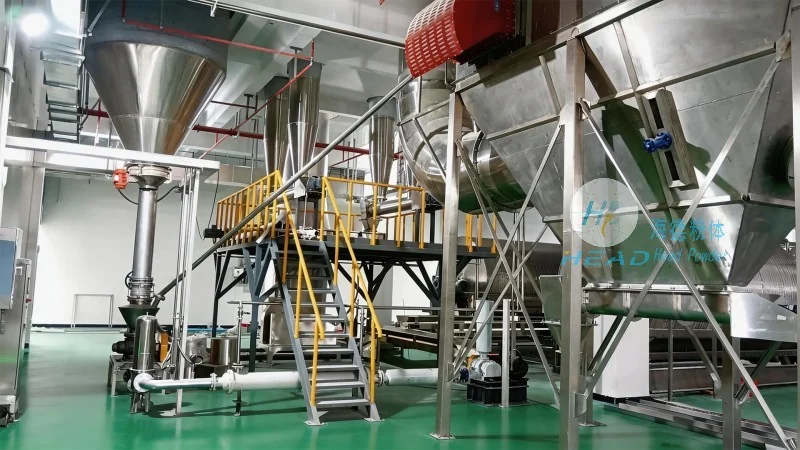
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced material handling equipment, specializing in the design, development, and installation of urea transport systems for denitrification applications. With years of experience in the industry, HeadPowder has established itself as a reliable partner for clients seeking efficient and cost-effective solutions for urea handling and delivery. The company's headquarters is located in Shandong, China, where it leverages its expertise and state-of-the-art facilities to deliver high-quality products and services.
Denitrification urea transport systems are designed to transport urea from storage silos or bulk containers to the injection points in SCR reactors. These systems typically consist of several key components, including a urea storage tank, a pump or feeder system, a pneumatic conveying line, and a control system. The primary function of these systems is to ensure a consistent and controlled supply of urea to the SCR system, which is critical for maintaining the proper ratio of urea to nitrogen oxides and achieving the desired reduction in NOx emissions.
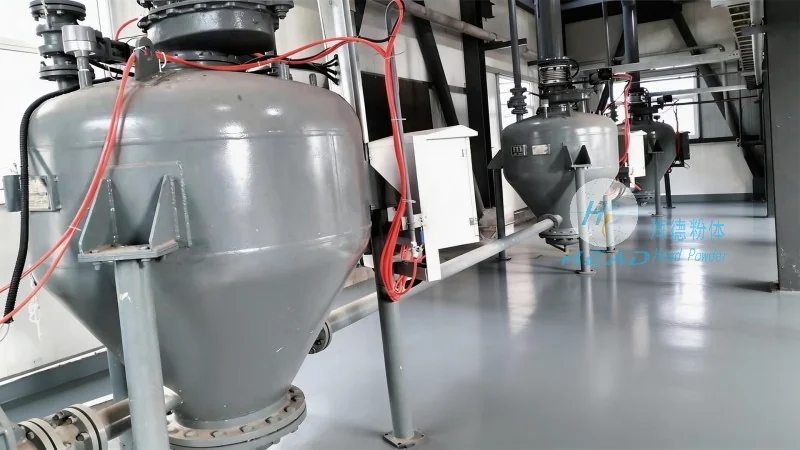
Pneumatic conveying is a widely adopted method for transporting urea in denitrification systems due to its numerous advantages over traditional methods such as screw conveyors or belt conveyors. One of the key benefits is the ability to handle urea in a dust-free environment, which reduces the risk of contamination and improves the overall safety of the process. Additionally, pneumatic conveying systems can transport urea over long distances with minimal pressure drop, making them suitable for large-scale industrial applications. The technology also allows for precise control of the urea flow rate, ensuring that the SCR system receives the exact amount of reagent needed for optimal performance.
HeadPowder's denitrification urea transport systems are engineered with several advanced features that enhance their performance and reliability. These systems are equipped with high-quality urea storage tanks that are designed to prevent moisture and contamination, ensuring the purity of the urea reagent. The pump or feeder system is equipped with advanced control technology that allows for precise regulation of the urea flow rate, which is critical for maintaining the proper NOx reduction efficiency. The pneumatic conveying line is constructed from corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of urea and ensure long-term durability. Furthermore, the control system is integrated with sensors and monitoring devices that provide real-time data on the system's performance, enabling operators to detect and address any issues promptly.
The efficiency of a denitrification system is directly linked to the reliability of its urea transport system. Any disruptions or inefficiencies in the urea delivery process can lead to reduced NOx reduction rates and increased emissions. HeadPowder's pneumatic conveying systems are designed to minimize downtime and ensure consistent performance, thereby maximizing the effectiveness of the SCR process. By delivering a steady and controlled supply of urea to the injection points, these systems help maintain the optimal operating conditions for the SCR catalyst, resulting in higher NOx reduction efficiency and lower operating costs.
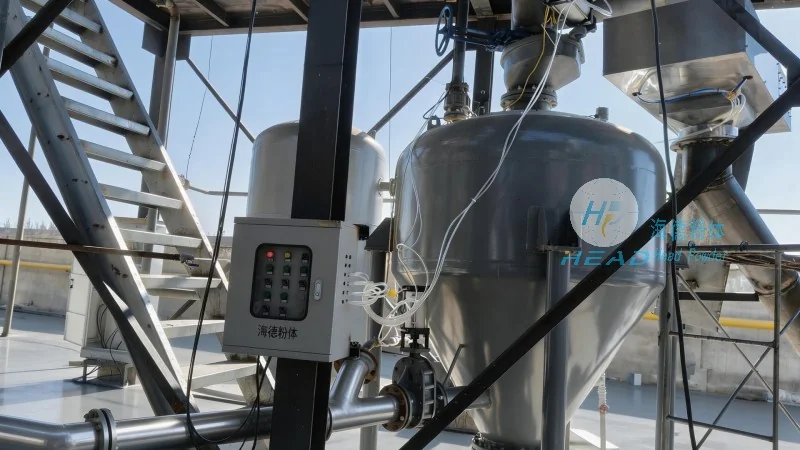
HeadPowder understands that each industrial facility has unique requirements for urea transport. Therefore, the company offers customized solutions tailored to the specific needs of its clients. Whether the application involves a small-scale power plant or a large industrial facility, HeadPowder can design and implement a urea transport system that meets the client's specifications. The company's engineering team works closely with clients to assess their requirements, provide technical recommendations, and develop a comprehensive solution that addresses all aspects of the urea handling process. This customized approach ensures that the final system is not only efficient and reliable but also cost-effective and easy to maintain.
Urea transport systems must adhere to strict safety and environmental regulations to ensure the well-being of workers and the protection of the environment. HeadPowder's denitrification urea transport systems are designed with safety as a top priority. The systems are equipped with safety features such as pressure relief valves, emergency shut-off valves, and leak detection systems to prevent accidents and minimize the risk of environmental contamination. Additionally, the company complies with all relevant industry standards and regulations, ensuring that its products meet the highest safety and quality requirements. By choosing HeadPowder's urea transport systems, clients can be confident that their operations are in compliance with all applicable regulations and that the safety of their personnel and the environment is protected.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top