HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced fly ash particle conveying systems. With a focus on efficiency and reliability, our systems are engineered to meet the demanding requirements of industrial applications, particularly in the power generation sector where fly ash management is critical. Based in Shandong, China, our company has established itself as a trusted partner for clients seeking innovative and effective solutions for transporting fly ash particles.
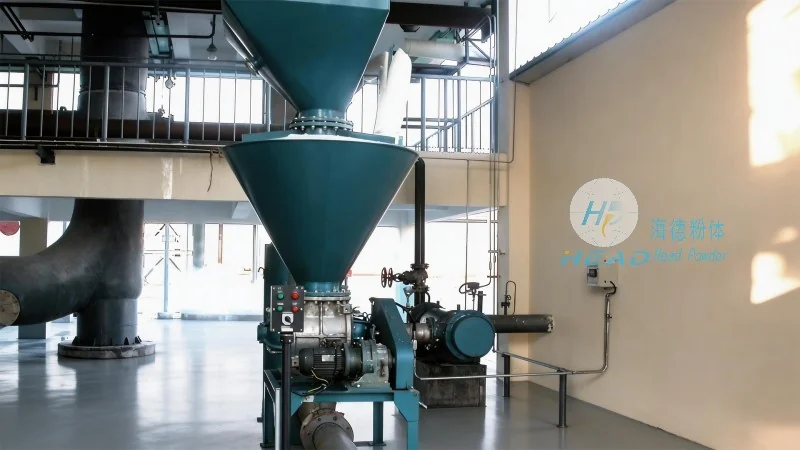
The fly ash particle conveying system developed by HeadPowder typically consists of several key components that work in tandem to ensure seamless and efficient material transport. These components include a material feeder, a conveying pipeline, a control system, and a dust collection unit. The material feeder is responsible for accurately measuring and feeding the fly ash particles into the system, while the conveying pipeline, often made of high-quality materials such as stainless steel or special plastic, transports the particles from the source to the destination. The control system monitors and regulates the entire process, ensuring optimal performance and preventing operational issues. Additionally, the dust collection unit is integrated to capture and filter any airborne particles, maintaining a clean and safe working environment.
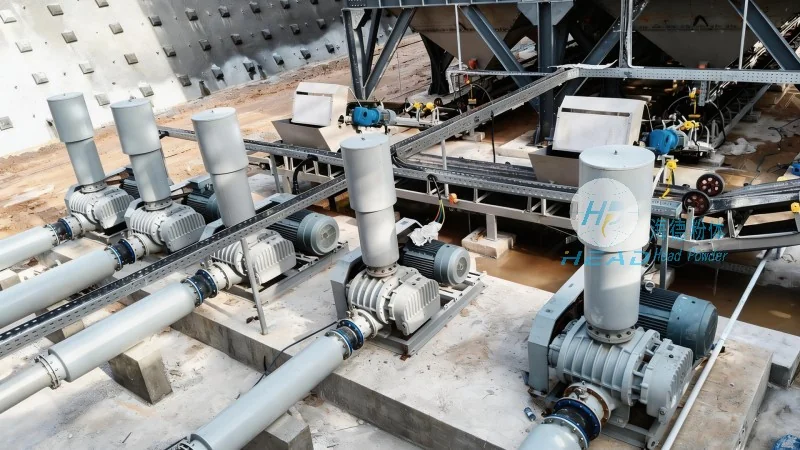
Pneumatic conveying offers several distinct advantages over traditional methods like belt conveyors or screw conveyors when it comes to transporting fly ash particles. One of the primary benefits is the ability to handle abrasive and fine materials without causing excessive wear and tear on equipment. Fly ash is known for its high abrasiveness, and conventional conveyors may experience rapid degradation over time. In contrast, pneumatic systems use air pressure to move particles, reducing mechanical stress on components and extending the lifespan of the equipment. Another significant advantage is the flexibility in system design. Pneumatic conveying systems can be easily adapted to various layouts and configurations, allowing for complex routing and integration with existing infrastructure. This flexibility is particularly valuable in industrial settings where space constraints or changing operational needs may require adjustments to the material flow path. Furthermore, pneumatic systems provide a more hygienic and controlled environment for handling fly ash. Unlike open conveyors that may expose workers to dust and particulate matter, pneumatic systems enclose the material transport process, minimizing the risk of contamination and improving overall safety. The enclosed design also helps in maintaining the quality of the fly ash, as it is less likely to be exposed to external elements or contaminants during transport. Additionally, pneumatic conveying systems can achieve higher transport speeds and capacities compared to traditional methods, enabling faster material movement and increased productivity in industrial operations. This efficiency is crucial for power plants and other facilities that require large volumes of fly ash to be transported quickly and reliably. The ability to handle both dry and wet fly ash, depending on the system configuration, adds another layer of versatility. Some systems are designed to handle wet or slurry-like fly ash, which is common in certain processing stages, while others are optimized for dry material transport. This adaptability ensures that the system can be tailored to the specific needs of the application, whether it involves transporting freshly produced fly ash or processed ash from storage facilities. The energy efficiency of pneumatic conveying is also a notable advantage. By using compressed air as the primary driving force, the systems can operate with lower energy consumption compared to electrically powered conveyors, especially when considering the overall operational costs over time. This makes pneumatic systems a cost-effective solution for long-term material handling needs. Finally, the reduced maintenance requirements of pneumatic conveying systems contribute to lower operational costs and increased uptime. With fewer moving parts and less mechanical friction, these systems experience lower wear and tear, resulting in fewer breakdowns and less downtime for maintenance. This reliability is essential for continuous industrial operations where any interruption in material transport can lead to significant production delays or operational inefficiencies.
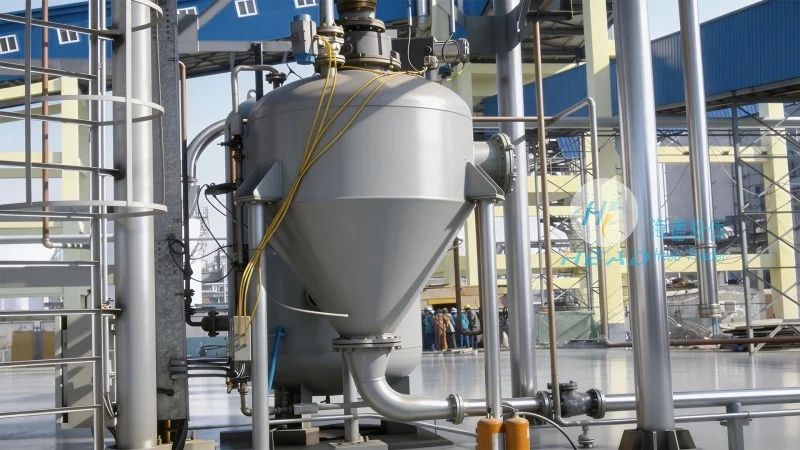
HeadPowder's fly ash particle conveying systems are widely used across various industries, with a particular focus on the power generation sector. Power plants, both thermal and biomass, rely on these systems to transport fly ash from the boiler to storage facilities or for further processing. The systems are also utilized in cement production, where fly ash is often used as a supplementary cementitious material, requiring efficient transport from storage to the production line. Additionally, in the construction and recycling industries, fly ash is used as a raw material for concrete and other building materials, making the conveying system essential for integrating this material into production processes. The versatility of the system allows it to be adapted to different scales of operation, from small-scale industrial applications to large-scale power plant installations. This adaptability ensures that clients can find a solution that meets their specific needs, whether they are handling small volumes of fly ash or large quantities in continuous production environments.
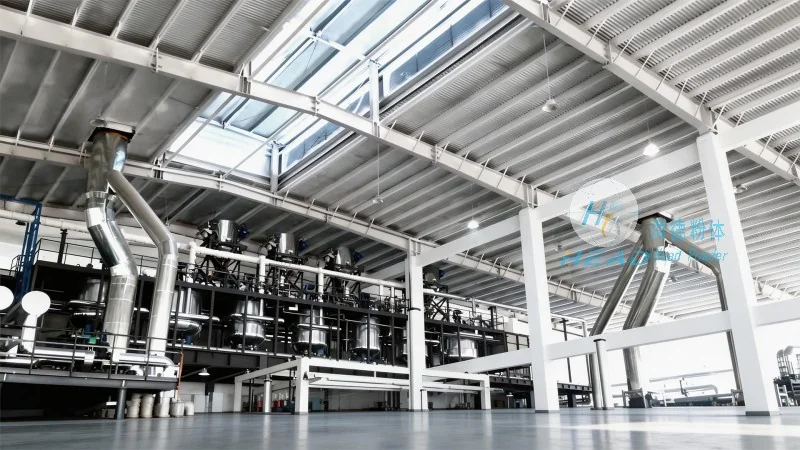
HeadPowder remains committed to providing high-quality, reliable, and efficient fly ash particle conveying systems. Our expertise in material handling technology, combined with a focus on customer needs and operational excellence, ensures that our systems deliver superior performance and long-term value. By leveraging advanced engineering and manufacturing capabilities, we continue to innovate and improve our solutions to meet the evolving demands of the industry. With our headquarters in Shandong, China, we are well-positioned to serve clients globally, offering tailored solutions that enhance operational efficiency and sustainability in fly ash management. The advantages of pneumatic conveying, as demonstrated by our systems, make them an ideal choice for industries seeking to optimize their material transport processes while maintaining safety and environmental standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top