Food processing facilities rely on efficient and reliable material handling systems to ensure smooth operations and maintain product quality. Among the various technologies available, pneumatic conveying stands out as a critical solution for transporting food products with precision and care. This overview explores the role of food handling systems, with a focus on the advantages of pneumatic conveying, as offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the industry.
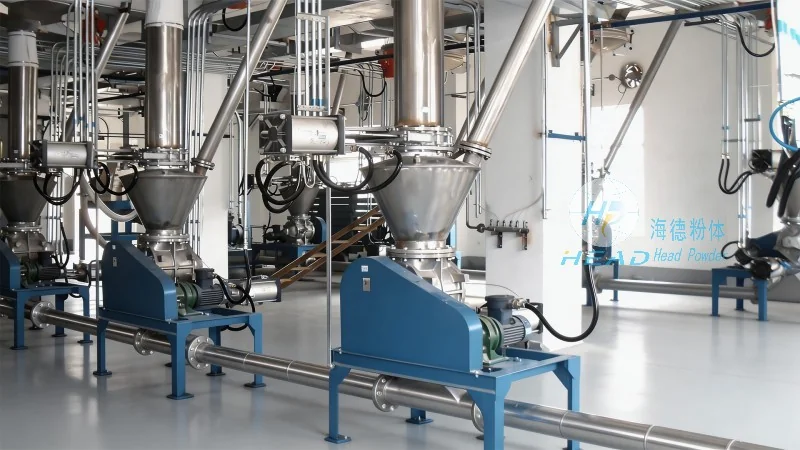
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable enterprise based in Shandong, China. Specializing in engineering solutions for the food processing sector, HeadPowder has established itself as a trusted partner for businesses seeking advanced material handling systems. The company's commitment to quality and innovation has positioned it as a key player in providing tailored solutions that meet the stringent requirements of the food industry.
In the food processing industry, the selection of appropriate handling systems is paramount to ensuring product integrity, safety, and operational efficiency. Traditional methods like belt conveyors or manual handling may pose challenges such as contamination risks, labor-intensive processes, and limited flexibility. Modern food handling systems, particularly those incorporating pneumatic conveying technologies, address these challenges by offering a hygienic, contactless, and scalable approach to material transport. These systems are designed to maintain the quality of sensitive food products while optimizing workflow and reducing downtime.
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using compressed air. In the context of food processing, this technology is widely adopted due to its ability to handle a diverse range of food products, from powders and granules to liquids and semi-solids. The process involves the use of air to move materials from a source to a destination, often with minimal human intervention. This approach eliminates the need for direct contact between the product and machinery, reducing the risk of cross-contamination and ensuring compliance with food safety regulations.
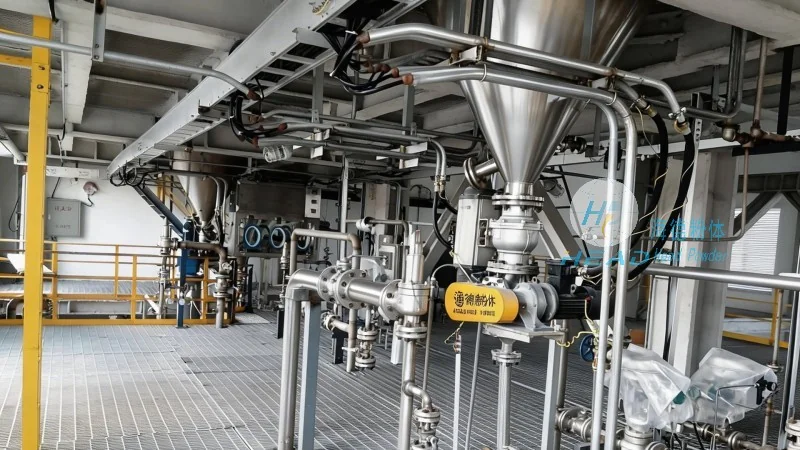
One of the primary advantages of pneumatic conveying is its superior hygiene. The enclosed system prevents dust, particles, and contaminants from entering the product stream, which is crucial for maintaining the safety and quality of food products. Additionally, the technology allows for precise control over material flow, enabling manufacturers to adjust the speed and direction of transport as needed. This flexibility is particularly beneficial in dynamic production environments where product types or quantities may vary.
Efficiency is another significant benefit of pneumatic conveying. By automating the material handling process, companies can reduce labor costs and minimize the time required for product transfer. The system’s ability to handle materials over long distances without the need for multiple transfer points or manual handling reduces operational complexity and enhances overall productivity. Furthermore, the compact design of pneumatic conveying systems saves valuable floor space in processing facilities, making them ideal for both new and existing installations.
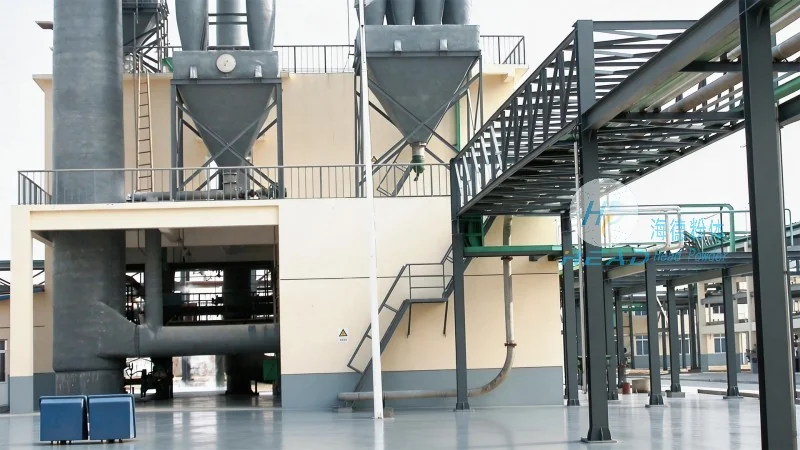
Food processing facilities must adhere to strict regulatory standards to ensure consumer safety. Pneumatic conveying systems are engineered with hygienic design principles in mind, featuring smooth surfaces, easy-to-clean components, and minimal dead zones where contaminants can accumulate. These features are essential for maintaining compliance with food safety guidelines such as those outlined by the FDA and other international regulatory bodies. HeadPowder’s expertise in designing and manufacturing pneumatic conveying systems ensures that their solutions meet these stringent requirements, providing peace of mind to food manufacturers.
Every food processing operation has unique requirements, and pneumatic conveying systems can be customized to suit specific needs. HeadPowder offers tailored solutions that can be scaled to accommodate varying production volumes and product types. Whether a facility is processing small batches of specialty foods or large-scale commodity products, the company’s engineers can design a system that optimizes performance and cost-effectiveness. This adaptability ensures that businesses can grow and expand their operations without the need for significant system overhauls.
Food handling systems, particularly those utilizing pneumatic conveying technology, play a vital role in modern food processing. The advantages of this approach, including enhanced hygiene, operational efficiency, and compliance with industry standards, make it an attractive choice for food manufacturers. Shandong HeadPowder Engineering Co., Ltd. continues to lead the way in providing innovative and reliable pneumatic conveying solutions, helping businesses in the food industry achieve their operational goals while maintaining the highest standards of product quality and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top