Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and implementation of advanced material handling solutions. With a focus on efficiency and reliability, the company has established itself as a trusted partner in the food processing industry, particularly in the cocoa sector. This article provides an overview of cocoa conveying systems, highlighting the key benefits and features of pneumatic conveying technology for cocoa transportation.
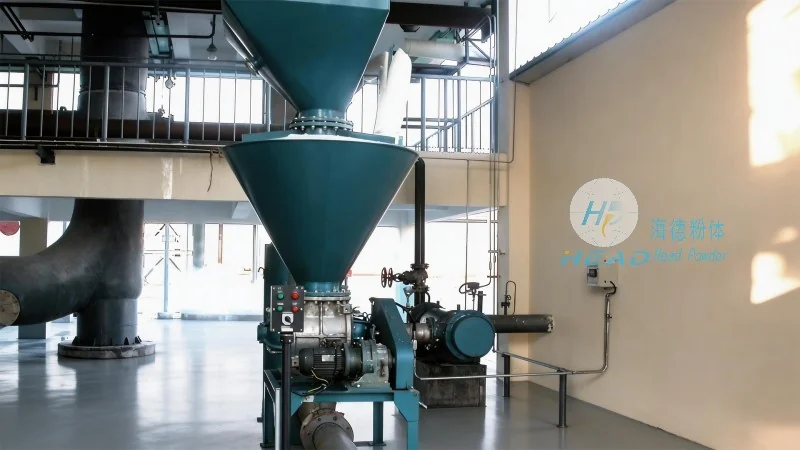
Cocoa conveying systems are essential for the efficient movement of cocoa beans, nibs, and other cocoa products within processing facilities. These systems are designed to handle the unique characteristics of cocoa, such as its moisture content, density, and susceptibility to breakage during transport. Traditional methods like belt conveyors or bucket elevators may struggle with the delicate nature of cocoa, leading to product damage or inefficiencies. In contrast, modern pneumatic conveying systems offer a more gentle and effective solution for cocoa handling.
Pneumatic conveying, also known as air conveying, is a method that uses air pressure or vacuum to transport bulk materials like cocoa through a pipeline system. This technology offers several advantages over traditional mechanical conveyors, making it an ideal choice for cocoa processing. First, it provides a hygienic and enclosed environment, which is crucial for maintaining the quality and safety of cocoa products. The enclosed system prevents contamination from external sources and ensures compliance with food safety regulations. Second, pneumatic conveying is highly flexible, allowing for the integration of multiple processing stages without the need for complex reconfigurations. This flexibility enables manufacturers to adapt to changing production demands and streamline their operations.
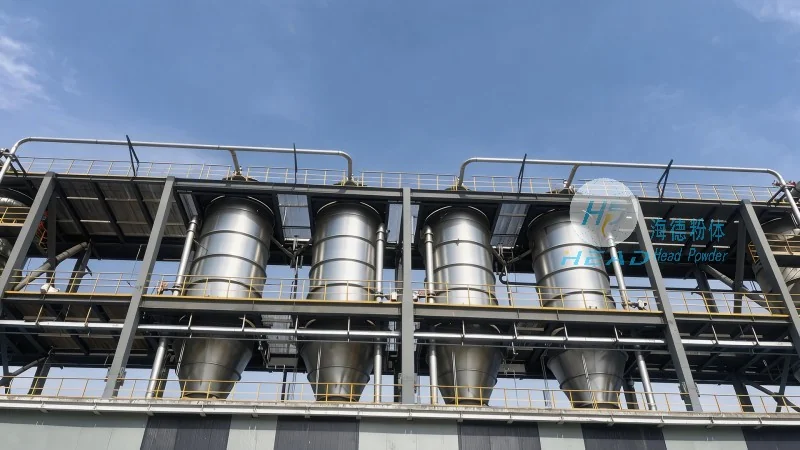
Modern cocoa pneumatic conveying systems incorporate advanced features that enhance performance and reliability. These systems typically include components such as airlocks, cyclones, and rotary valves, which work together to ensure smooth and continuous material flow. The use of high-quality materials, such as stainless steel, ensures durability and resistance to corrosion, which is essential for handling cocoa and other food products. Additionally, advanced control systems allow for precise regulation of air pressure and flow rates, optimizing energy consumption and reducing operational costs. The gentle handling of cocoa particles minimizes breakage and maintains the product's quality, which is critical for downstream processing steps like roasting and grinding.
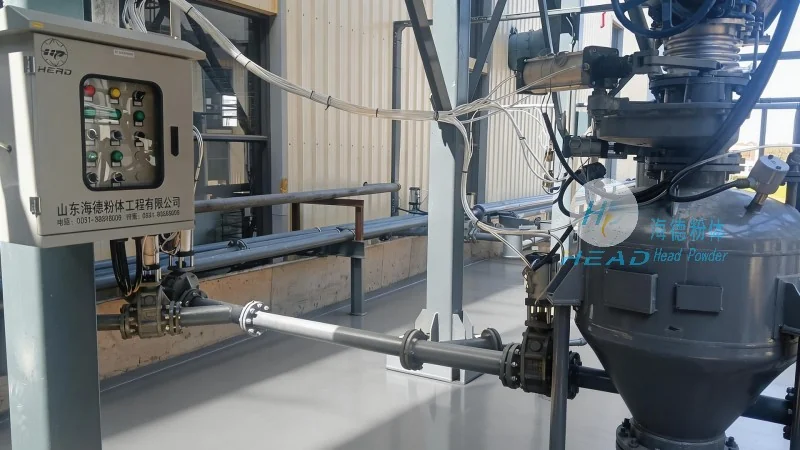
Cocoa pneumatic conveying systems are widely used in various stages of cocoa processing. From the initial reception and storage of cocoa beans to the final packaging of cocoa powder or cocoa butter, these systems play a vital role in ensuring efficient material handling. In the reception stage, pneumatic conveyors can transport cocoa beans from trucks or storage silos into processing facilities, reducing manual labor and exposure to dust. During the roasting process, the system can transfer roasted beans to grinding equipment, ensuring a consistent and uniform flow. In the final stages, pneumatic conveying is used to move cocoa powder or cocoa butter from grinding and refining equipment to packaging lines, maintaining product integrity throughout the process.
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive solutions for cocoa conveying systems, leveraging the advantages of pneumatic conveying technology to meet the demands of modern cocoa processing. By providing efficient, hygienic, and flexible material handling solutions, the company helps cocoa manufacturers improve productivity, reduce costs, and maintain product quality. With a commitment to innovation and customer satisfaction, HeadPowder continues to be a leader in the development of advanced material handling systems for the food industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top